Featured Raw Materials for Food Grade Wrapping
Precision-manufactured base substrates engineered for high barrier performance, food hygiene compliance, and seamless cup formation.
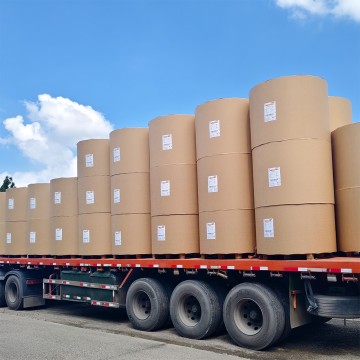
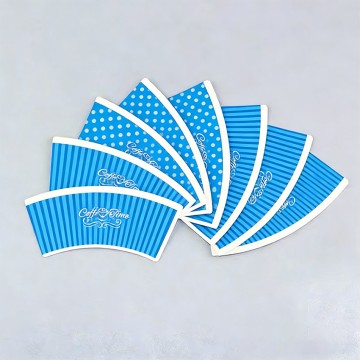
Commercial Landscape & Industrial Evolution of Paper Cup Raw Materials for Food Grade Wrapping
In modern industrial packaging and quick-service restaurant (QSR) logistics, paper cup raw materials have transitioned from conventional single-use drink vessels into sophisticated substrates suited for comprehensive food-grade wrapping, takeaway bowls, dual-chamber lunch boxes, and moisture-controlled barrier envelopes. Driven by global plastic restrictions such as the EU Single-Use Plastics Directive (SUPD) and surging demand across North America and the Asia-Pacific region, the industry is witnessing an unprecedented technological overhaul toward sustainable barrier chemistry and high-tensile baseboards.
Our raw board matrices are formulated with pure long-fiber and short-fiber balances, ensuring high internal bond strength and optimal bending stiffness (MD/CD stiffness ratio), indispensable for cup formers exceeding 250 cups/min.
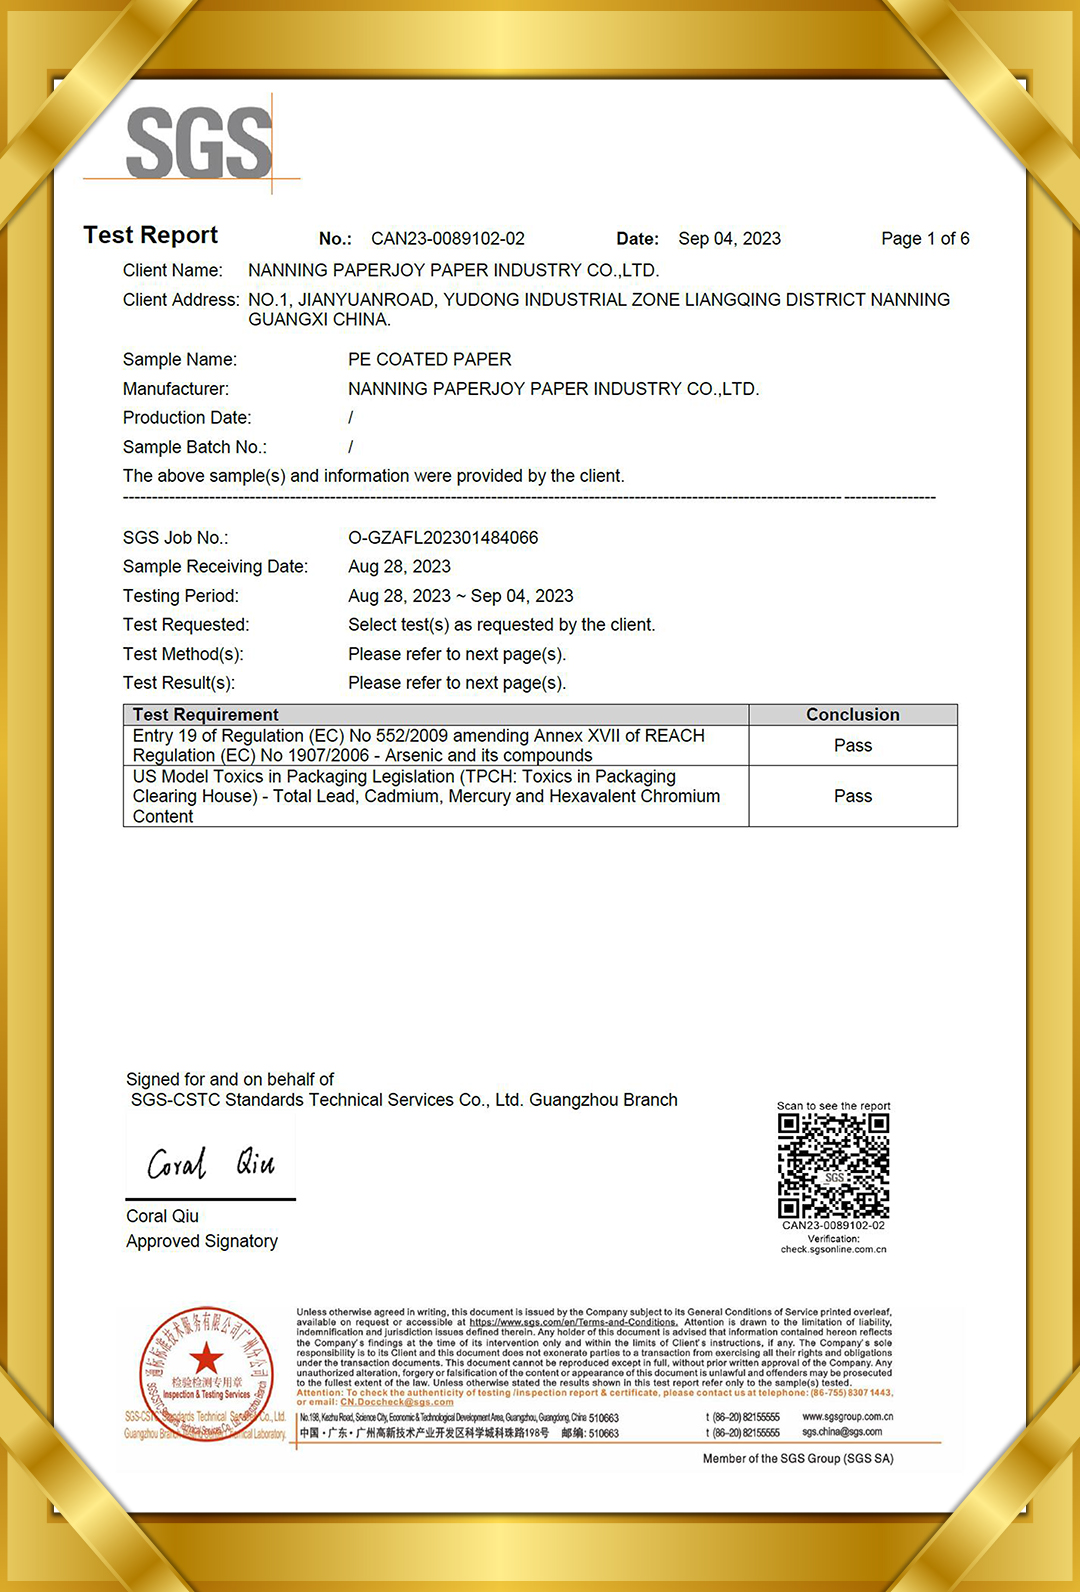
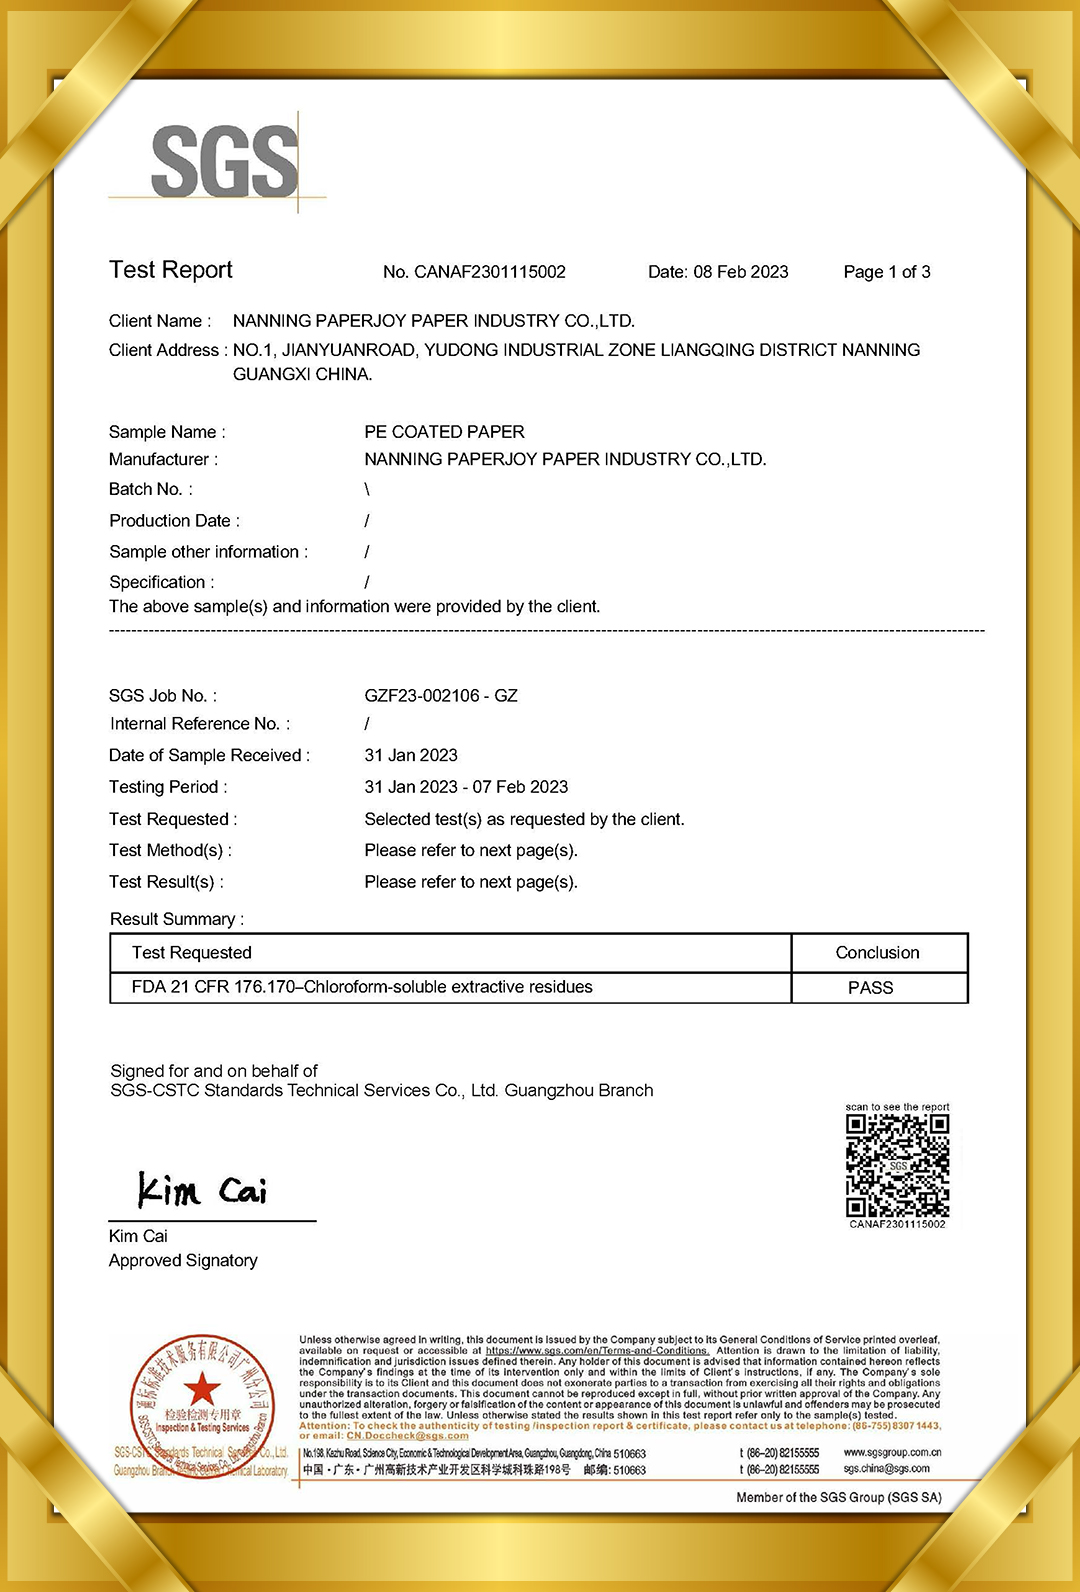
Certified food-contact surfaces undergo multi-layer polymer extrusion. This blocks grease, hot oil, organic acids, and aqueous vapors without chemical migration into contents, fulfilling FDA 21 CFR 176.170 specifications.
Innovations in easily repulpable waterborne coatings and ultra-thin high-density PE formulations allow converting waste and post-consumer containers to re-enter conventional pulp reclaiming channels with minimum yield loss.
In-Depth Analysis: Multi-Scenario Food Grade Wrapping Applications
While historically isolated to cold beverage cups and hot coffee mugs, paper cup raw materials—such as virgin pulp C1S ivory board, folding box board (FBB), and specialized extrusion kraft paper—have penetrated advanced wrapping sectors:
- Direct-Contact Hot Food Containers: Single-wall and double-wall PE coated sheets prevent thermal softening and grease permeation when holding fried meats, greasy pastries, and piping-hot broths up to 100°C.
- Cold Chain & Frozen Dessert Wrapping: Double-sided PE laminated board prevents condensation-induced delamination in ice cream tubs, gelato containers, and flash-frozen meat wrapping.
- Modular Takeaway Boxes & Compartment Bowls: The rigid structure of GC1 and GC2 folding box boards enables interlocking lid seals and leak-free structural scoring, ensuring food integrity across multi-stage gig-economy food delivery.
Future Market Trajectory & Technical Challenges
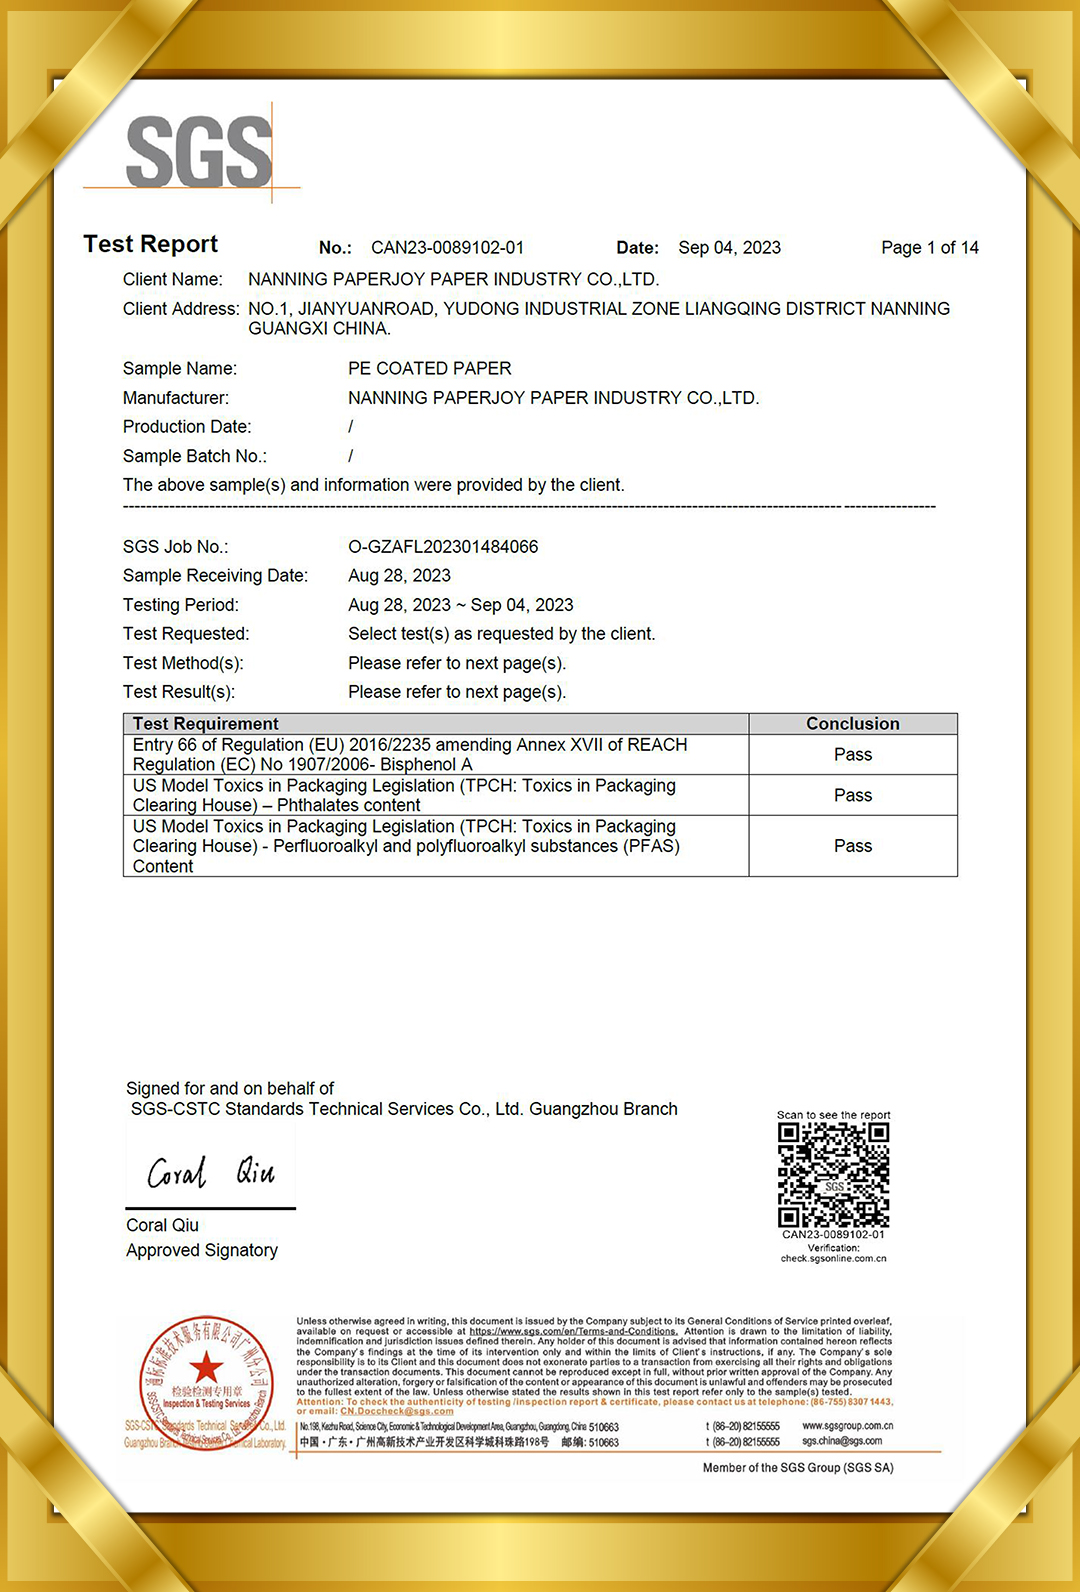
The intersection of artificial intelligence in factory line defect detection, ultrasonic seam welding, and microscopic barrier thickness consistency defines current paperboard production. As global brands eliminate polyfluoroalkyl substances (PFAS) and bisphenol contaminants, Paperjoy delivers 100% certified virgin fiber grades ensuring non-toxic migration, reliable heat sealing, and uncompromised surface printability via non-toxic water-based flexo inks.
Company Profile
Nanning Paperjoy Paper Industry Co., Ltd. – Leading the Global Standard in Food Grade Paper Converting
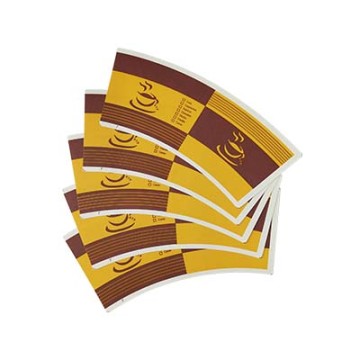
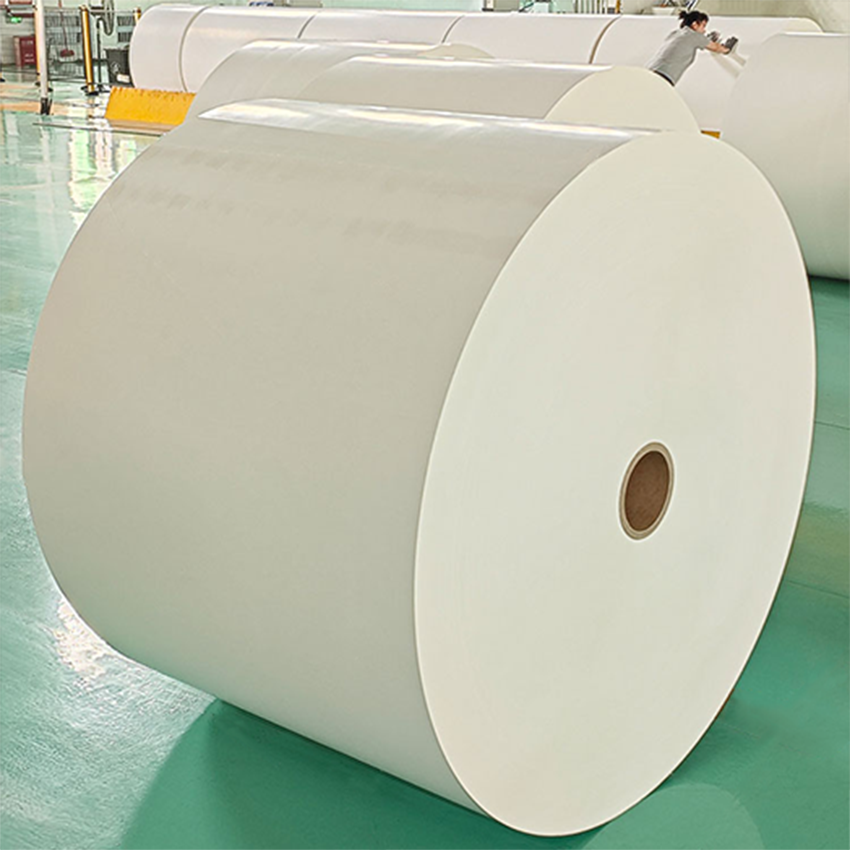
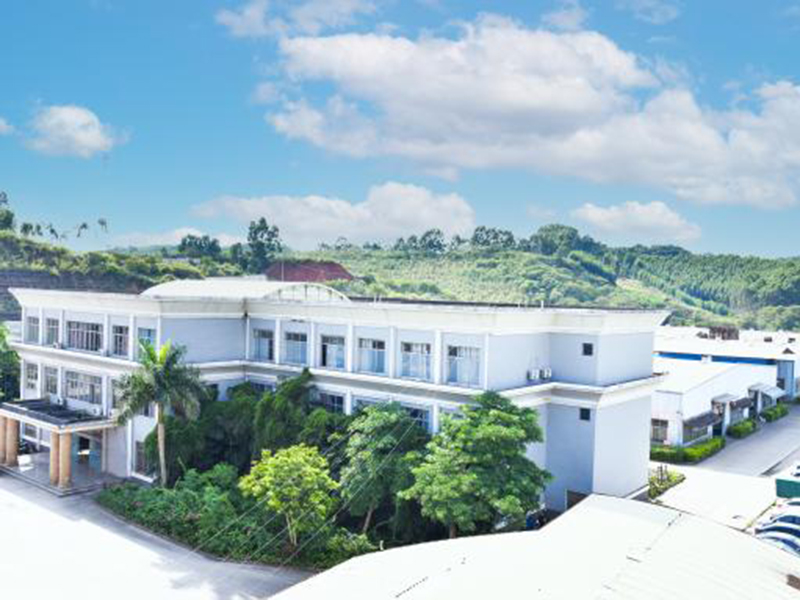
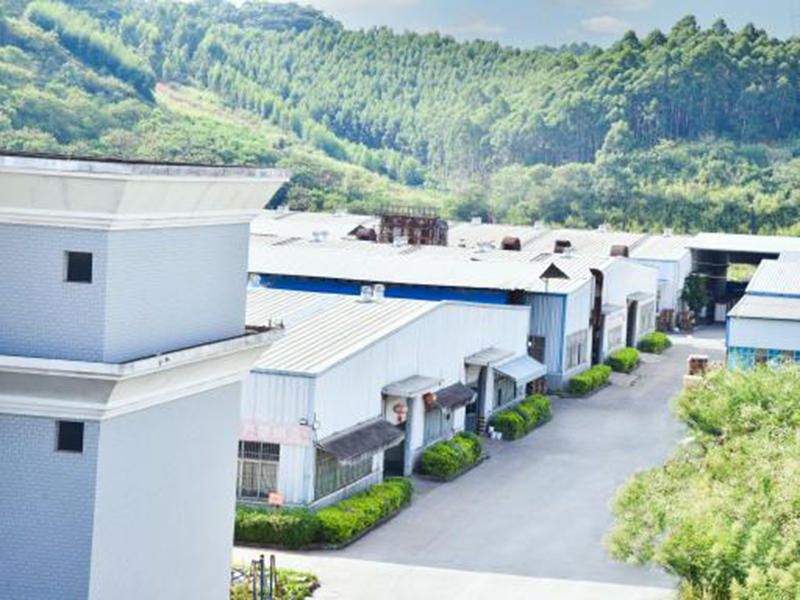
Nanning Paperjoy Paper Industry Co., Ltd. (“Paperjoy”) was established in 2006, with 200 employees and covers over 15000㎡. Paperjoy is a professional manufacturer of raw materials for paper cup and packaging box, especially the PE coated paper roll, paper cup fan, cup bottom reel and C1S ivory board. We are specializing in producing different kinds of PE coated paper raw materials. The annual production capacity is 60,000 tons.
Our factory ideally located at the heart of Nanning city economic zone, which is very near to Qinzhou port, Beibu Gulf at the South of China. Our 200 well-trained and technically sound staff are motivated towards accomplish a common goal of customer satisfaction and devoted to achieve “Honesty, Mutual benefit, Win-Win cooperation” business philosophy.
Our Development Journey
Factory Overview & Key Metrics
Unmatched industrial scale backing your food wrapping raw material procurement.
Located near top tier paper mill conglomerates: Stora Enso, Sunpaper, APP, Yibin paper, and FiveStar paper. We guarantee non-stop raw roll allocation, reliable fiber quality, and stable lead times.
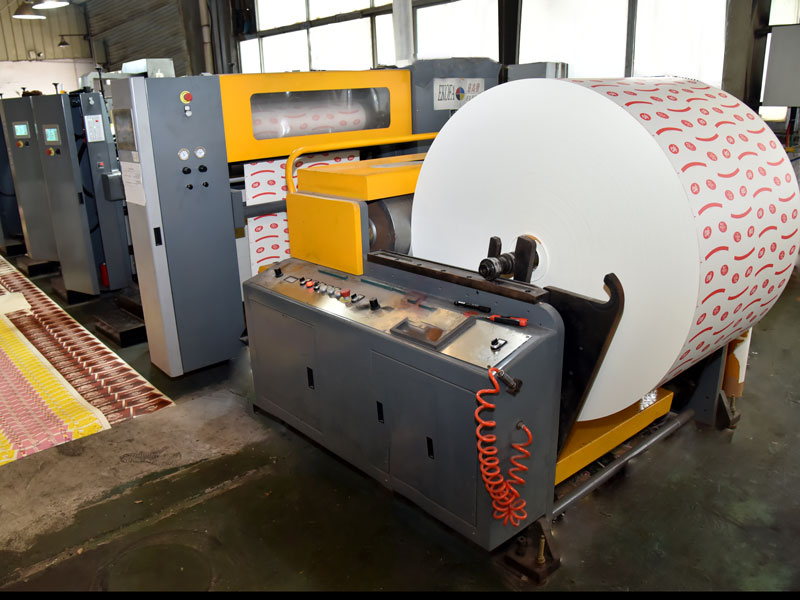
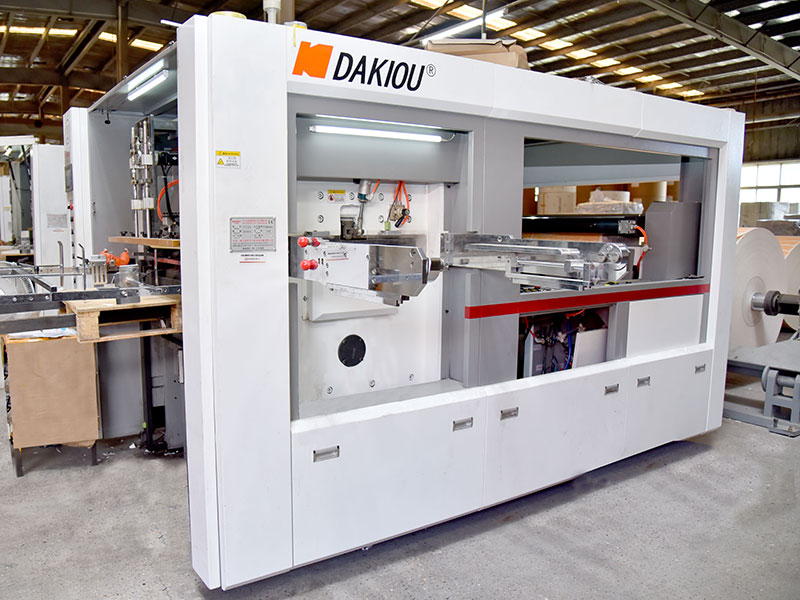
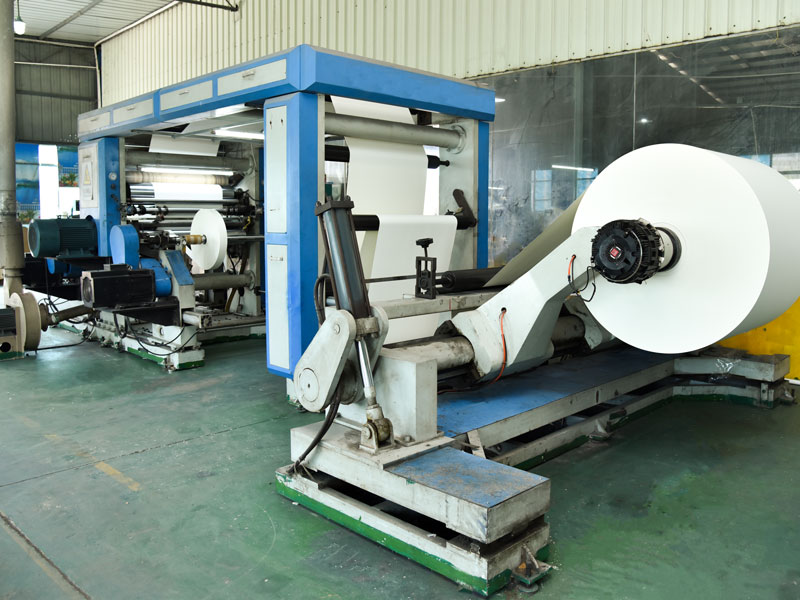
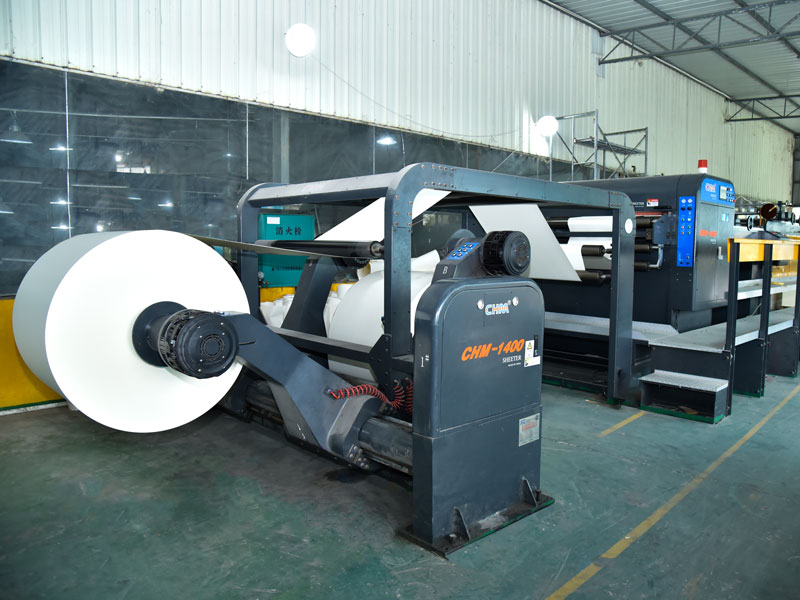
With complete automated systems, Paperjoy provides complete one-stop processing from high-grade PE extrusion coating, 6-color flexographic printing, die-cutting, to precise slitting.
Equipped with intelligent supply chain mechanisms, standard high-demand specifications are dispatched seamlessly, with large batch volume orders fulfilled within 7-15 business days.
PaperJoy Global Service & Value Proposition
Why Choose Paperjoy Paper? Your Reliable Global Partner for High-Quality Professional Paper Cup Raw Materials Supplier and Manufacturer & Professional Solutions.
We provide tailored paperboard raw material solutions according to target specifications, cup volumes, barrier thicknesses, and sealing equipment parameters.
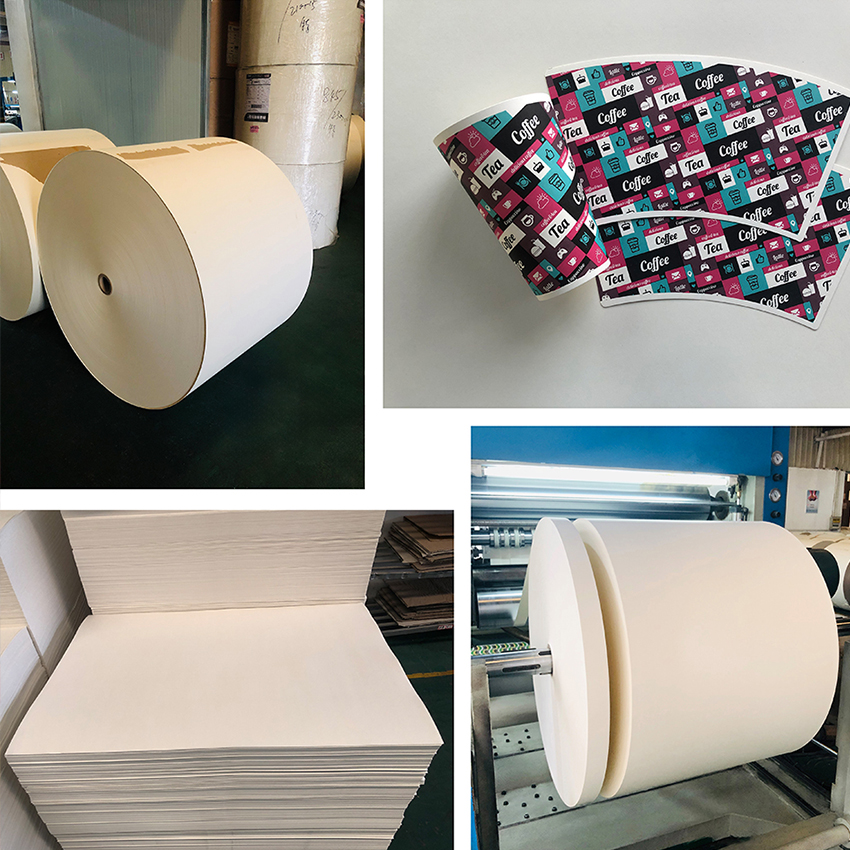
Complete product range including PE Coated Paper Rolls, PE Coated Paper Sheet, Paper Cup Fans, C1S Ivory Board, and Kraft Paper Roll to satisfy any food wrapping requirement.
We provide free testing samples and detailed technical quotations so partners can test heat-sealability, rigidity, and food barrier efficiency on their own production machinery.
Source inspection of 100% pure pulp, real-time in-line thickness sensors, continuous burst & Cobb moisture barrier verification, and full batch traceability.
Direct factory manufacturing without intermediary markup guarantees maximum price competitiveness for industrial converters and distributors globally.
Our packaging engineering and customer care team delivers round-the-clock guidance covering machine adjustment, tension profiles, and eco-compliance certifications.
Vision & Mission
Dedicated to environmental stewardship, social responsibility, and worldwide product excellence.
Our Vision
Bring health & environmental protection to all over the world through pure, biodegradable, and sustainable food packaging materials.
Mission: Global Leadership
To be the best global supplier of paper cup raw materials, driving technical innovation, reliable performance, and eco-friendly packaging shifts.
Mission: Empowering People
To be the happy home for our staff, fostering safety, career growth, mutual respect, and shared win-win prosperity across the enterprise.
Factory Tour & Advanced Production Infrastructure
Explore our smart manufacturing facilities, cleanroom conversion lines, and strict multi-checkpoint testing laboratories.
Office & Administrative Environment
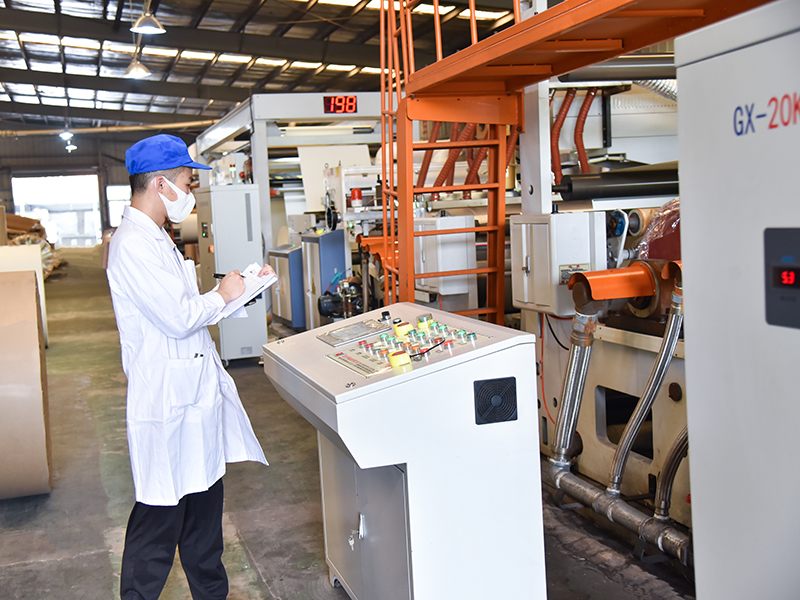
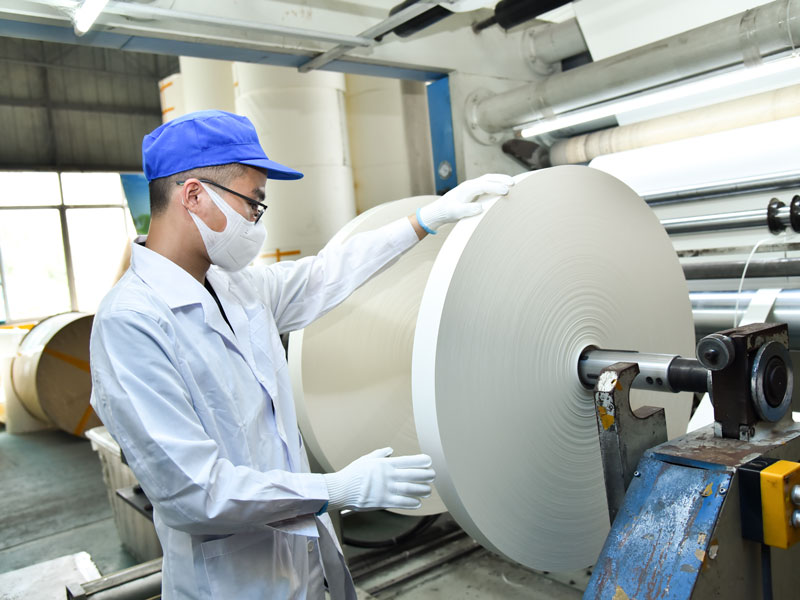
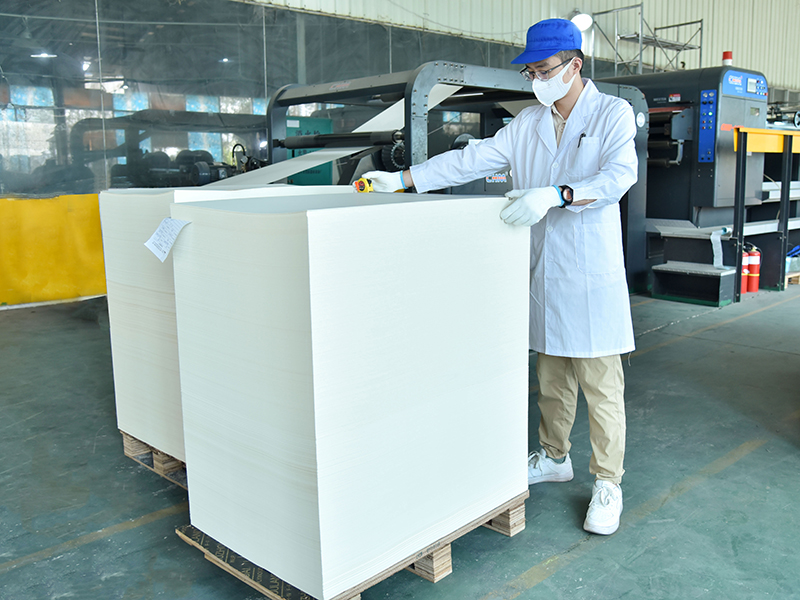
Personnel Operation & Quality-Controlled Workflows
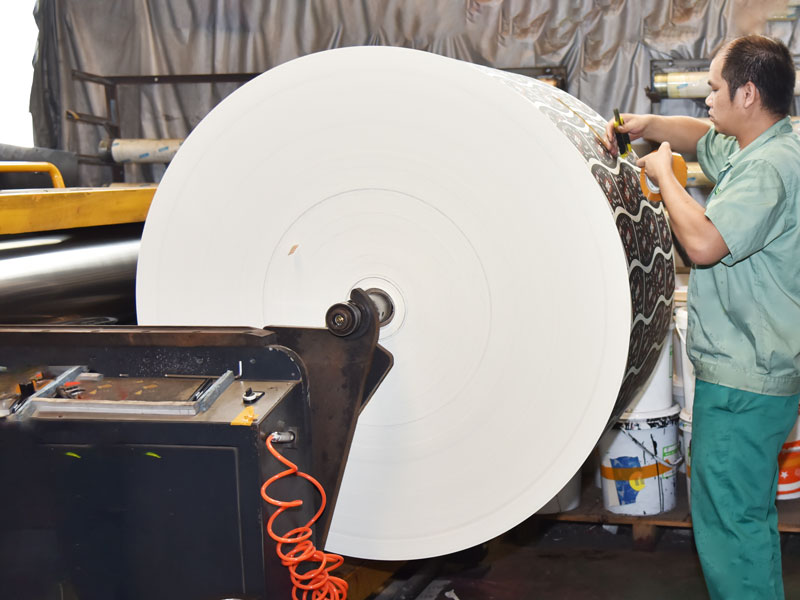
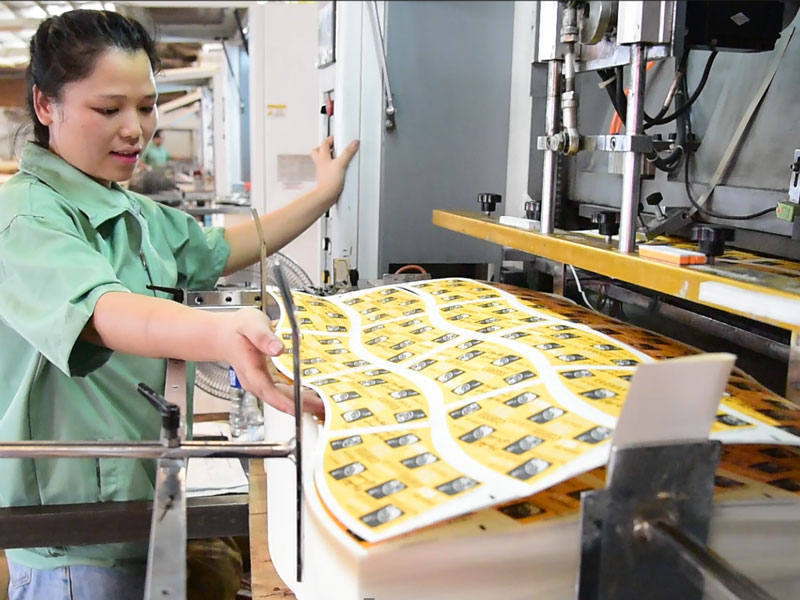
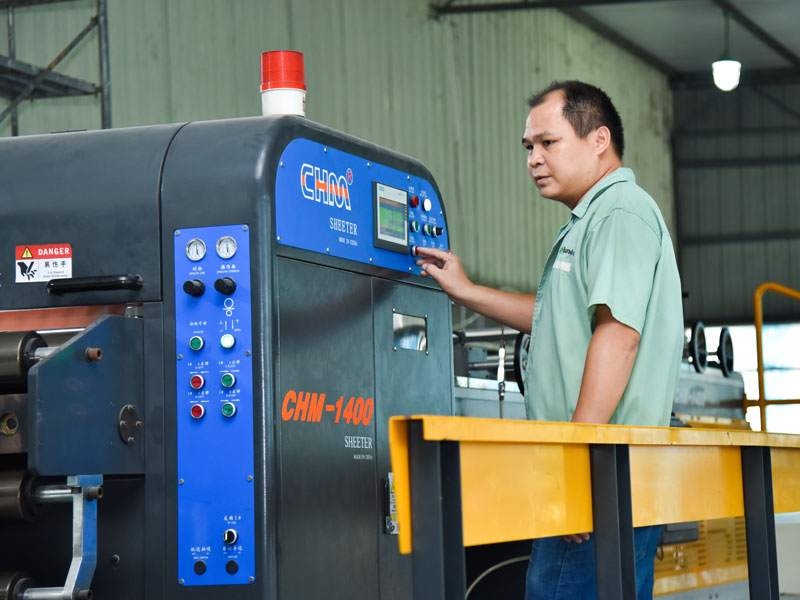
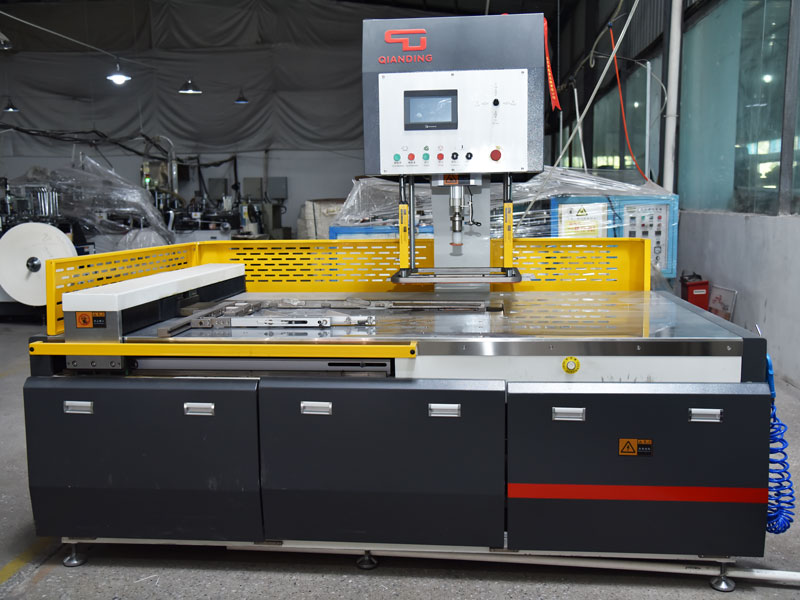
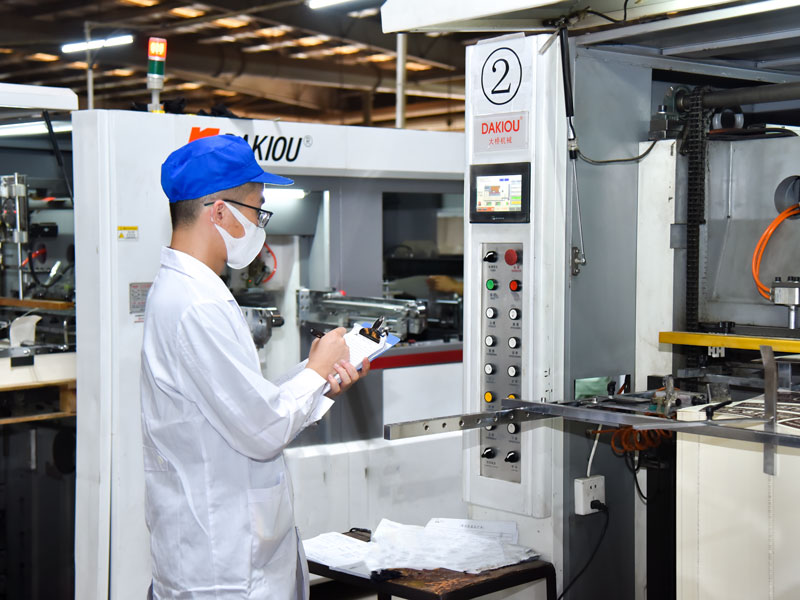
Industrial Converting Machinery Fleet
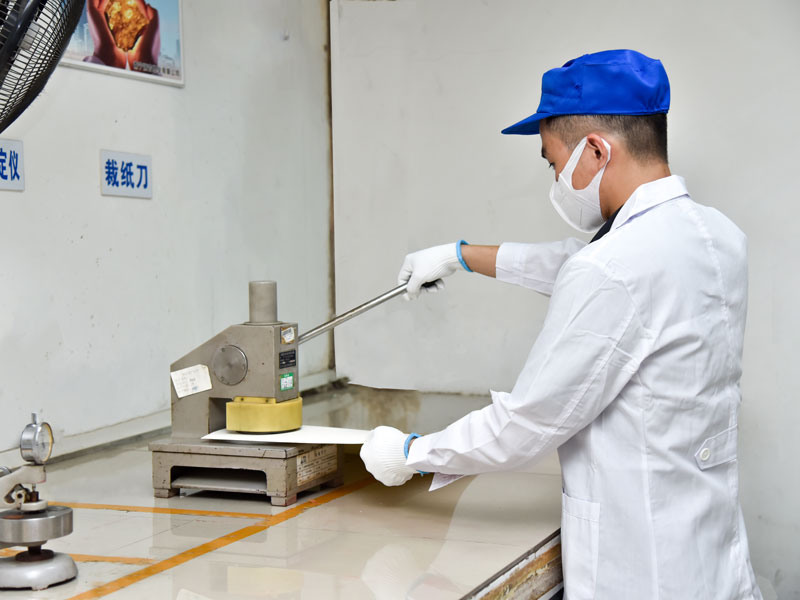
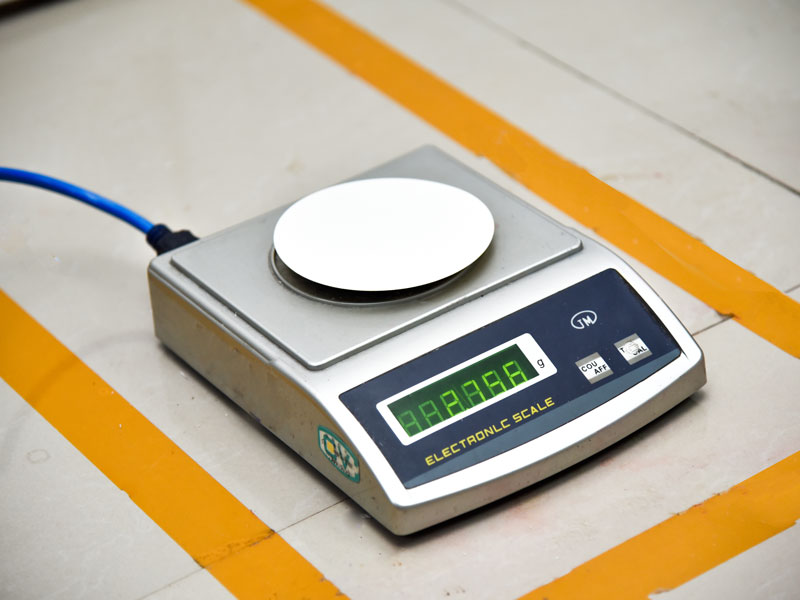
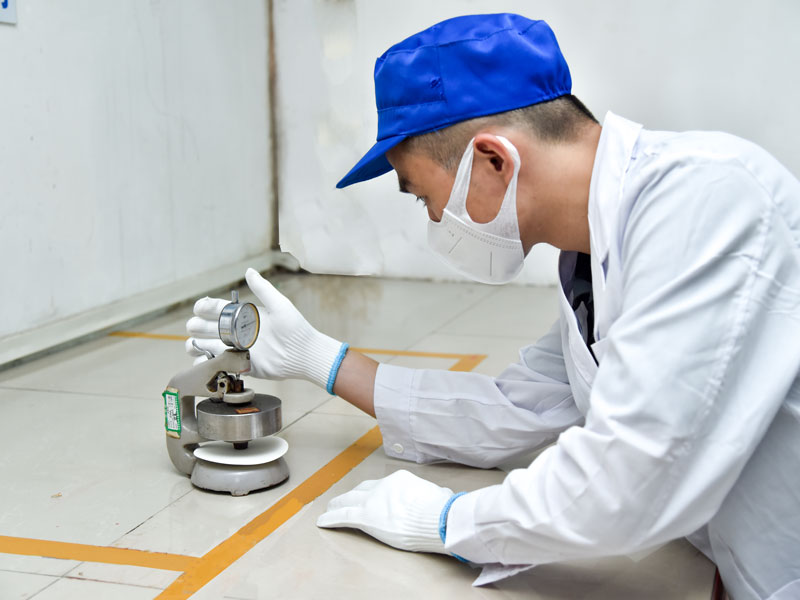
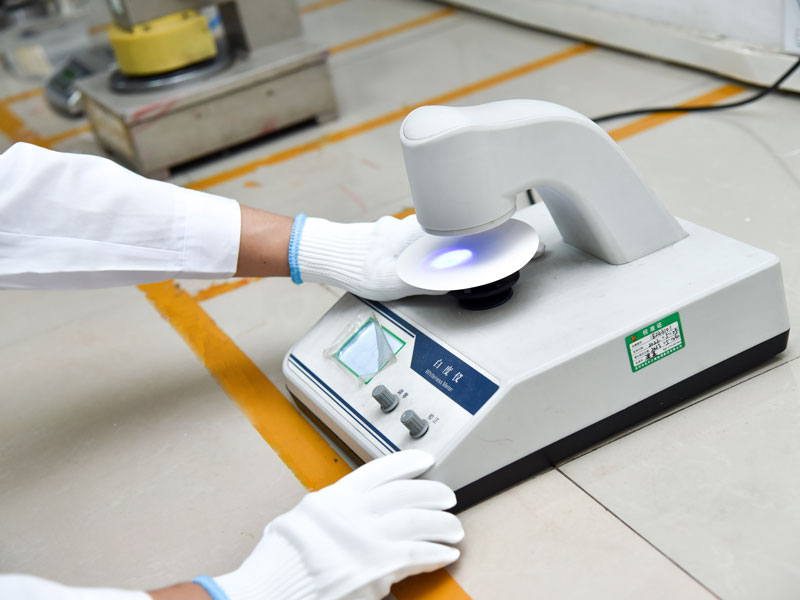
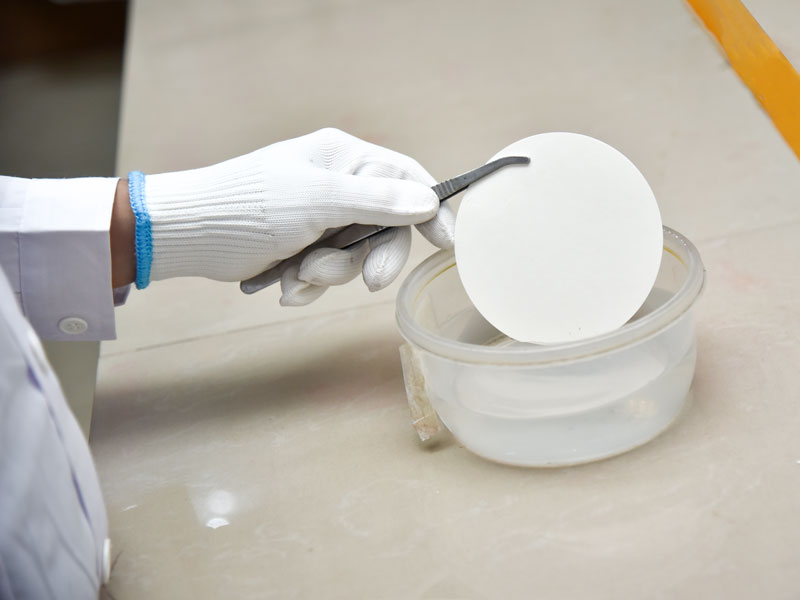
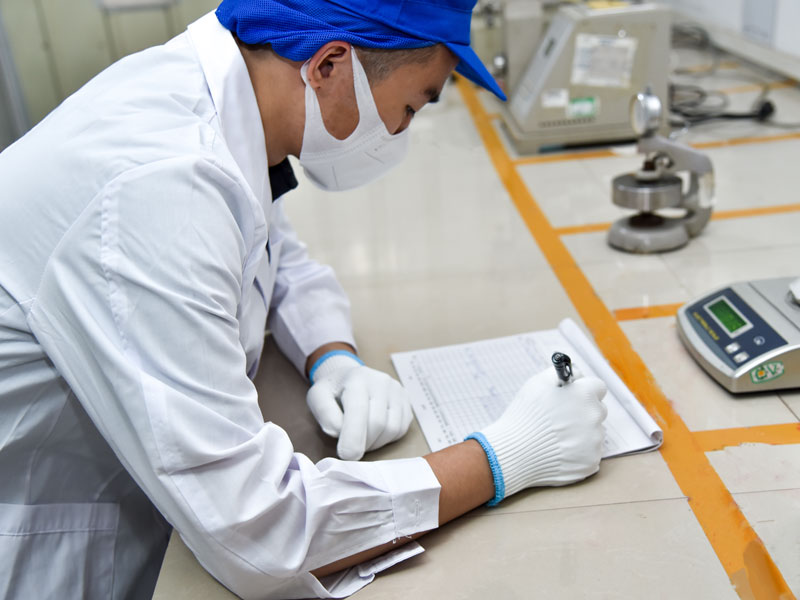
Quality Inspection & Laboratory Standards
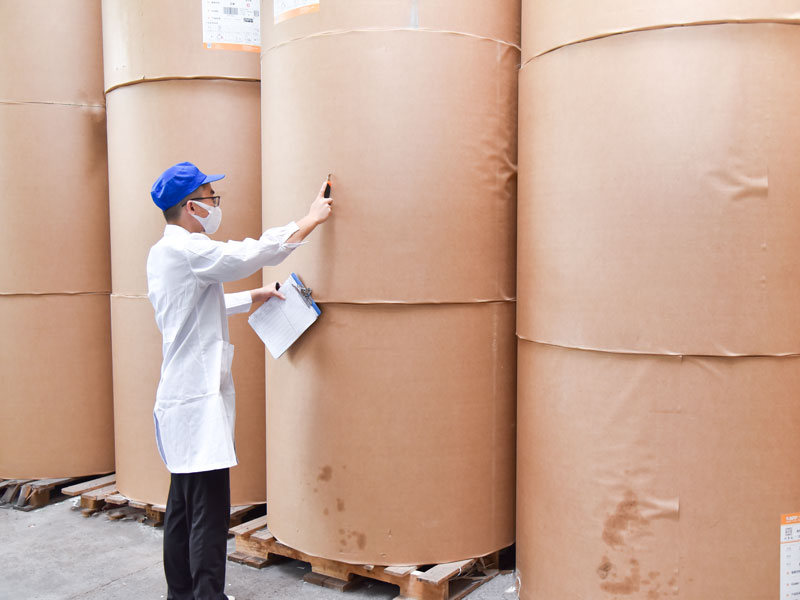
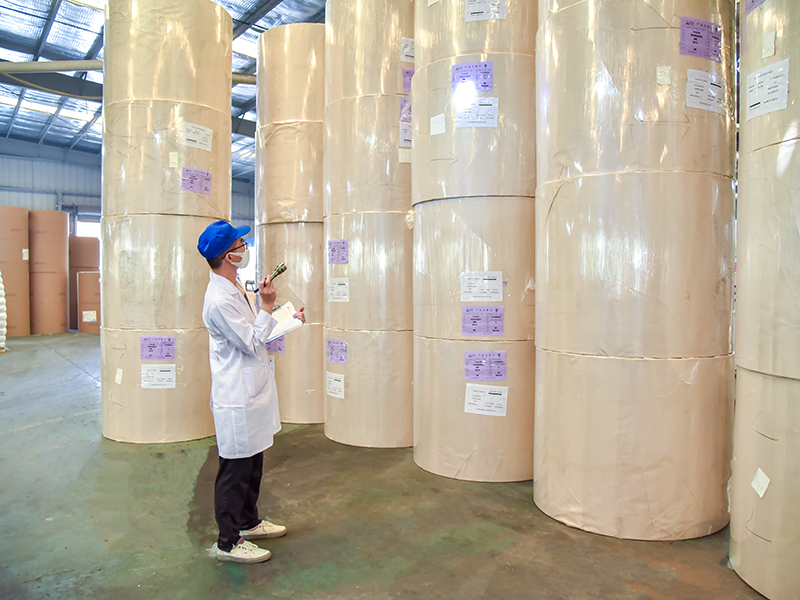
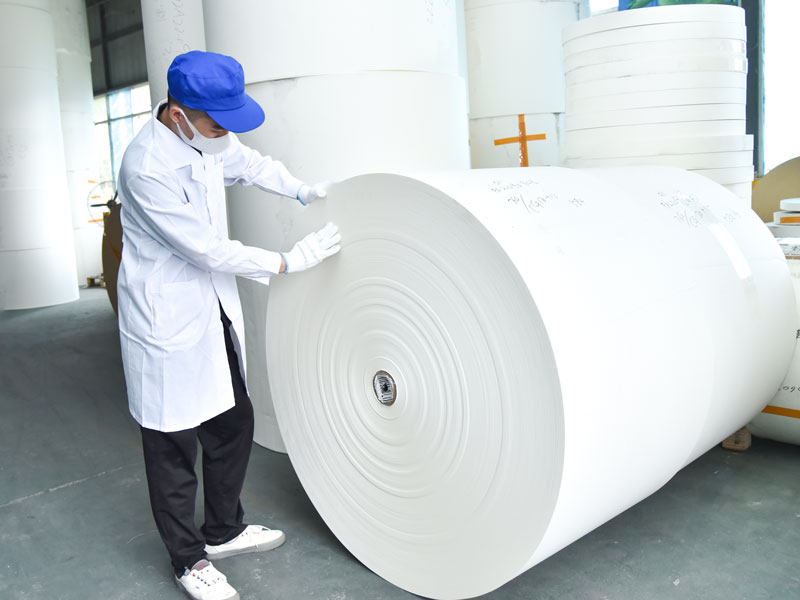
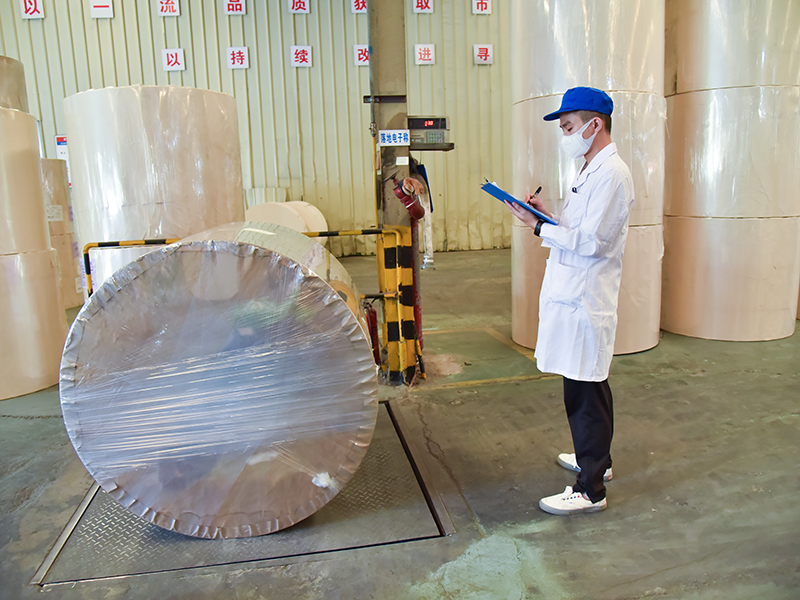
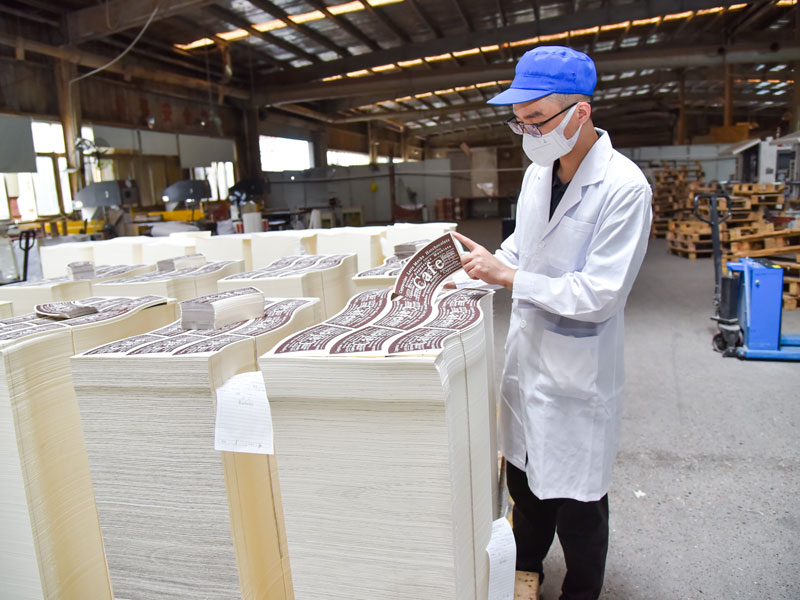
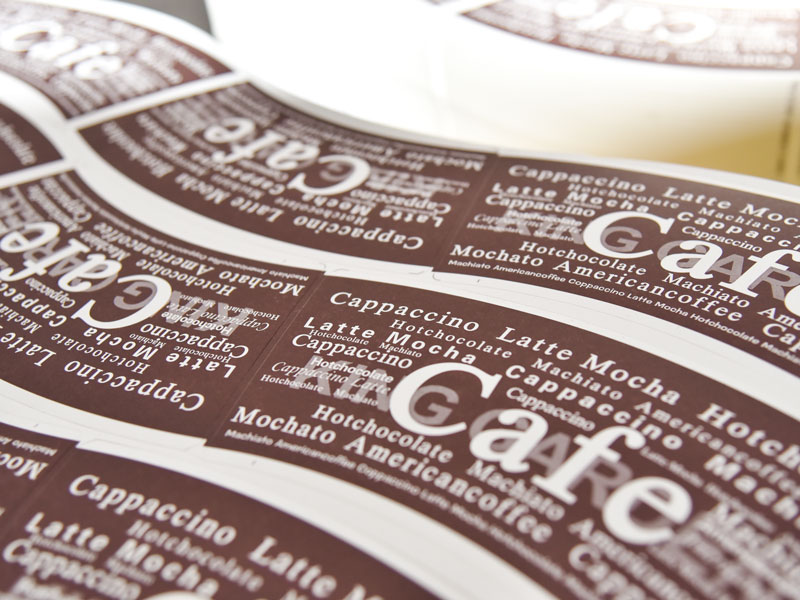
PaperJoy’s quality assurance system applies across 100% of material processes, verifying barrier integrity, cup stiffness, pinhole resistance, and migration safety.
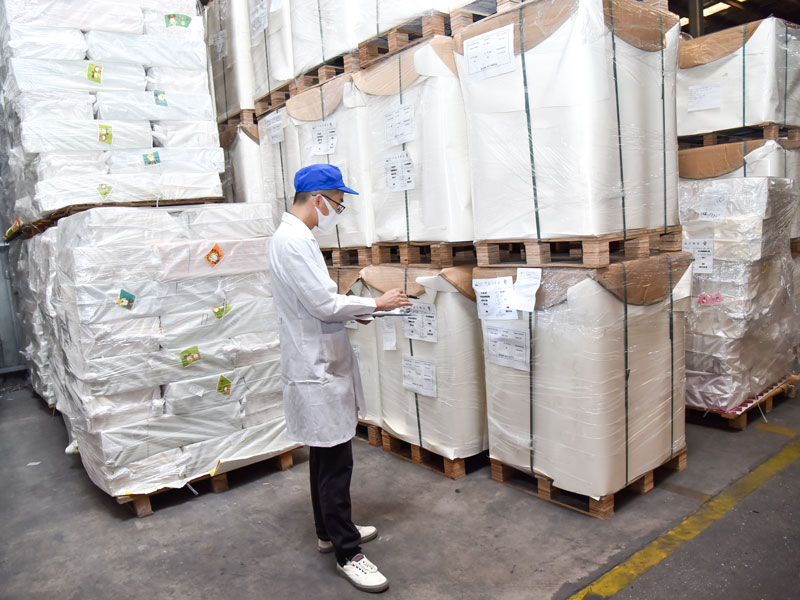
Packaging, Warehousing & Export Delivery
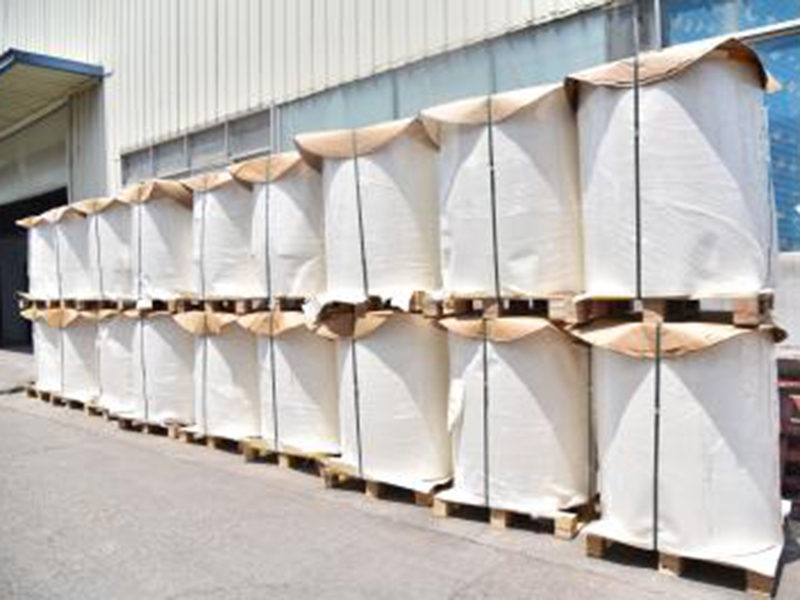
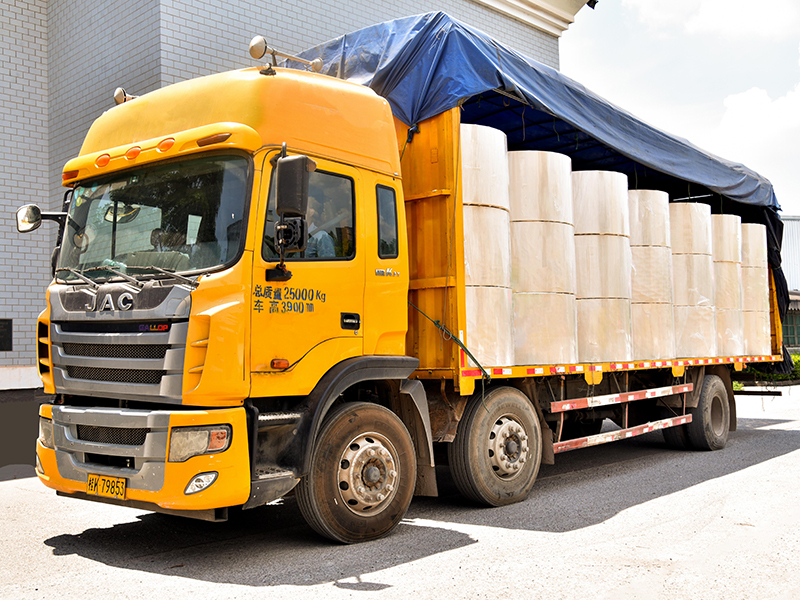
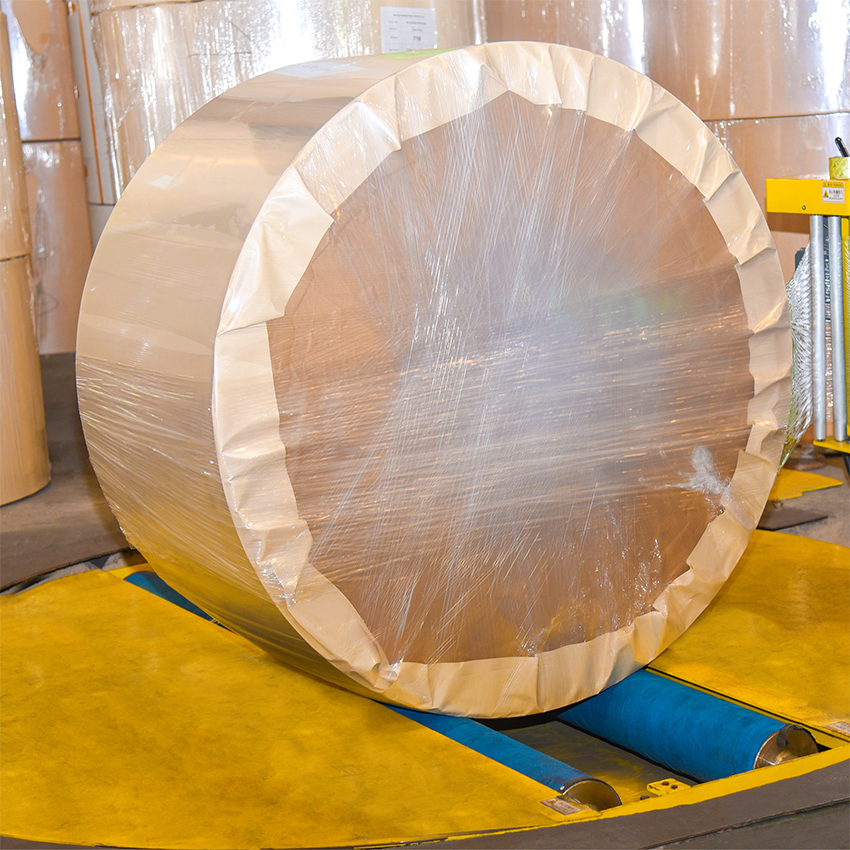
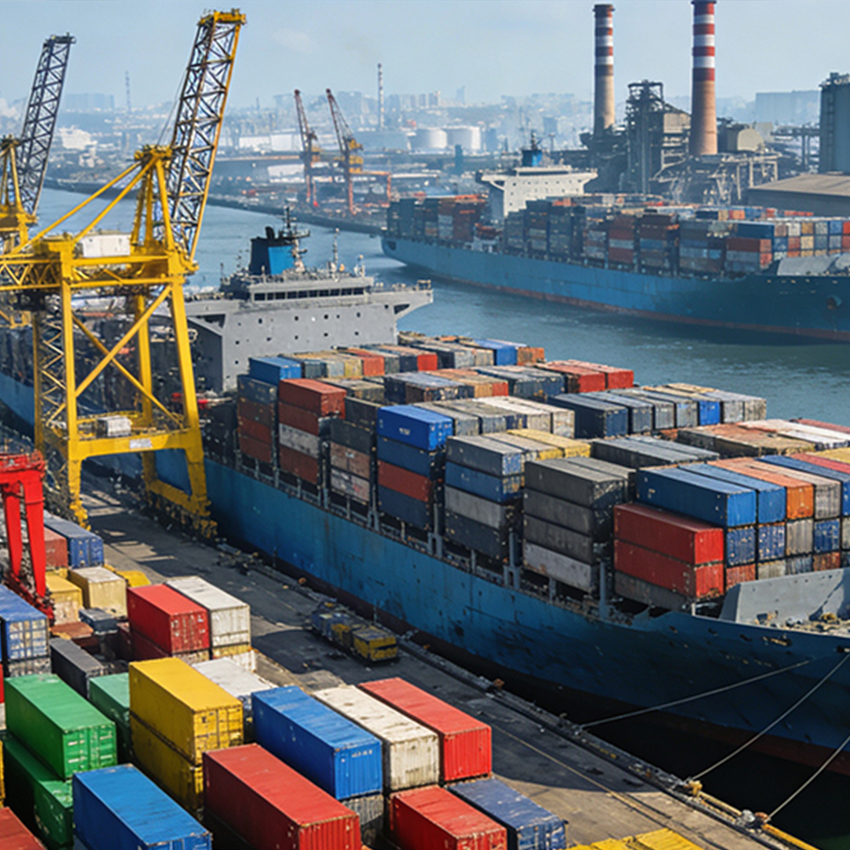
Seaworthy multi-layer export moisture packaging protects virgin wood pulp substrates during transoceanic shipping.
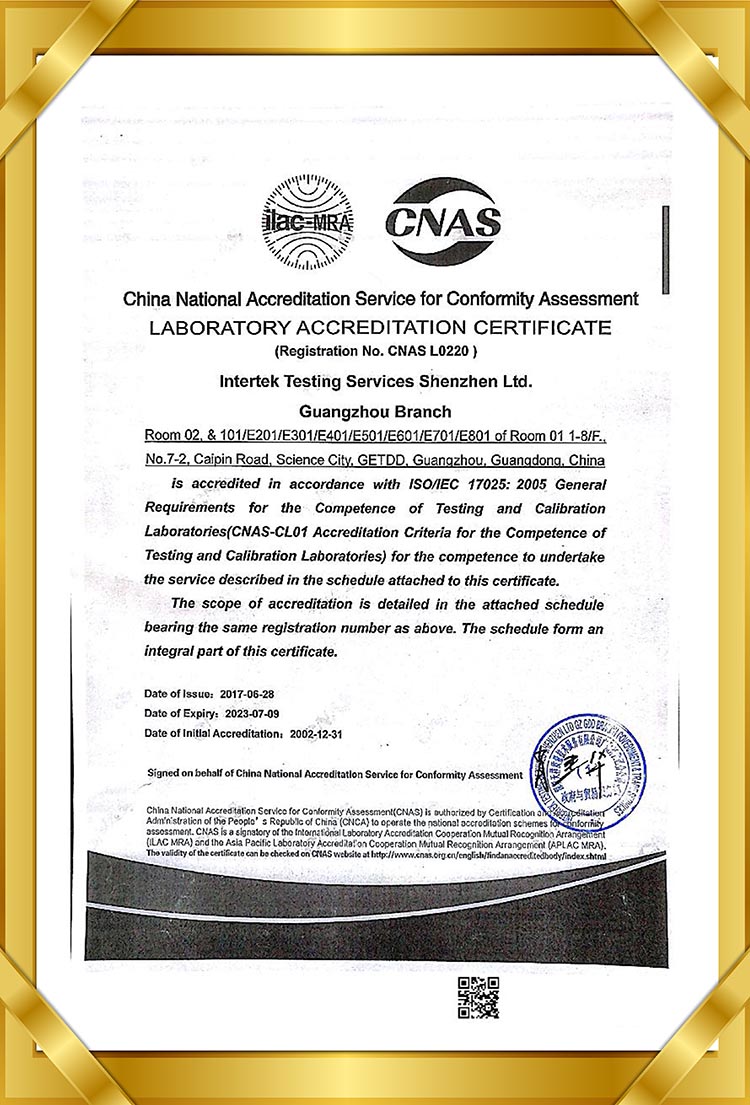
International Certifications & Industry Honors
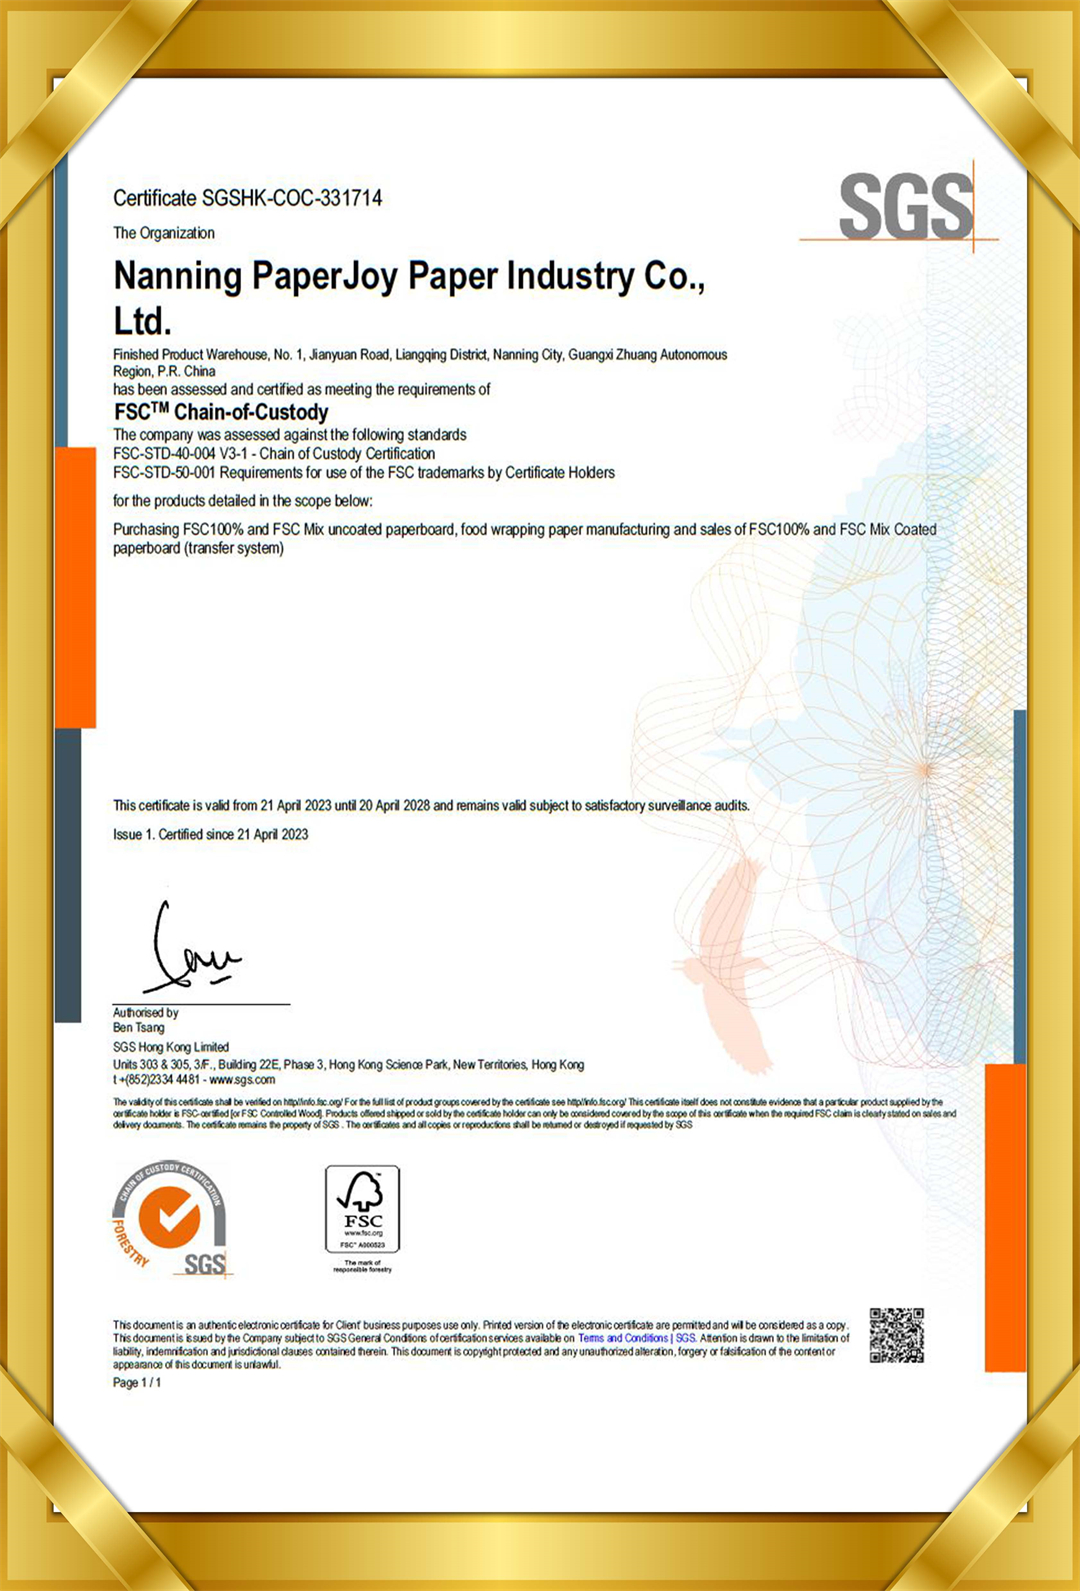
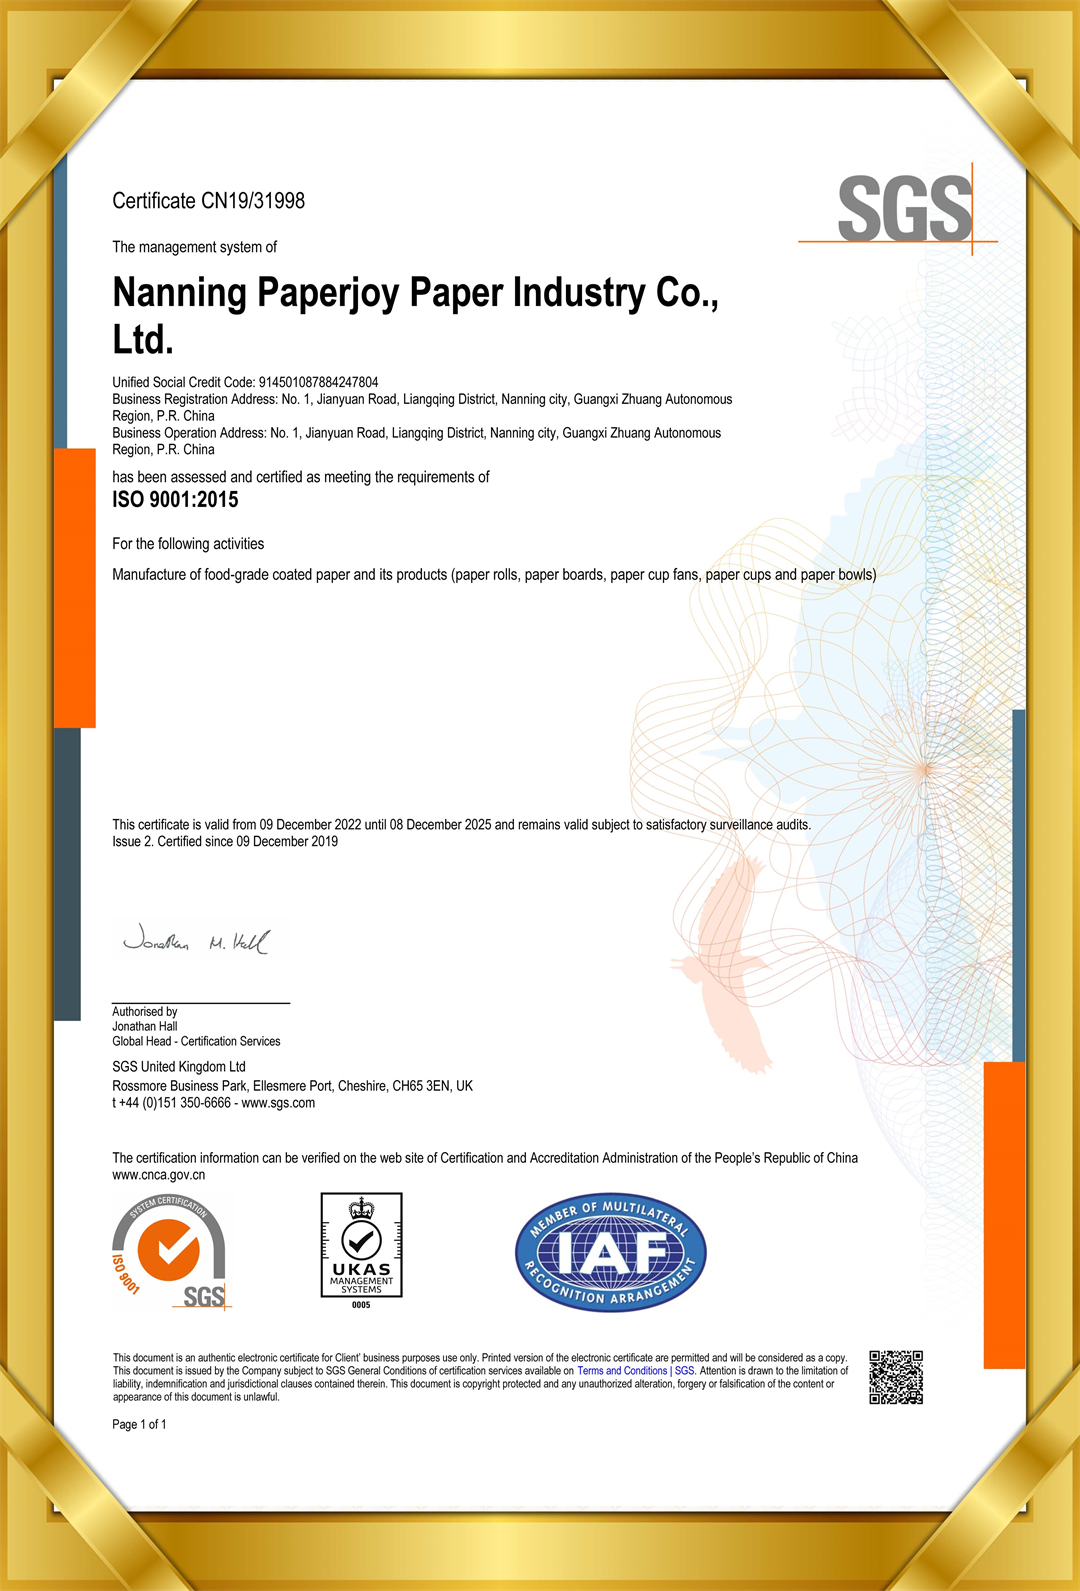
Fully verified against stringent global food safety, environmental forestry, and chemical compliance frameworks.
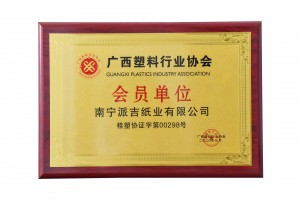
Corporate Recognition & Social Responsibility
Complete Food Grade Paper Cup & Wrapping Product Catalog
Browse our complete inventory of rolls, sheets, fans, and boards engineered for high-performance packaging and food-wrapping integrity.