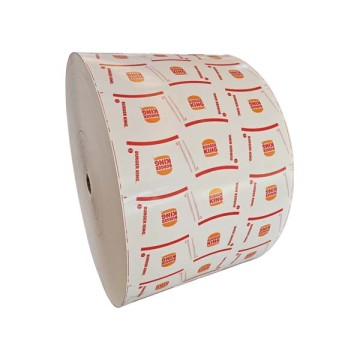
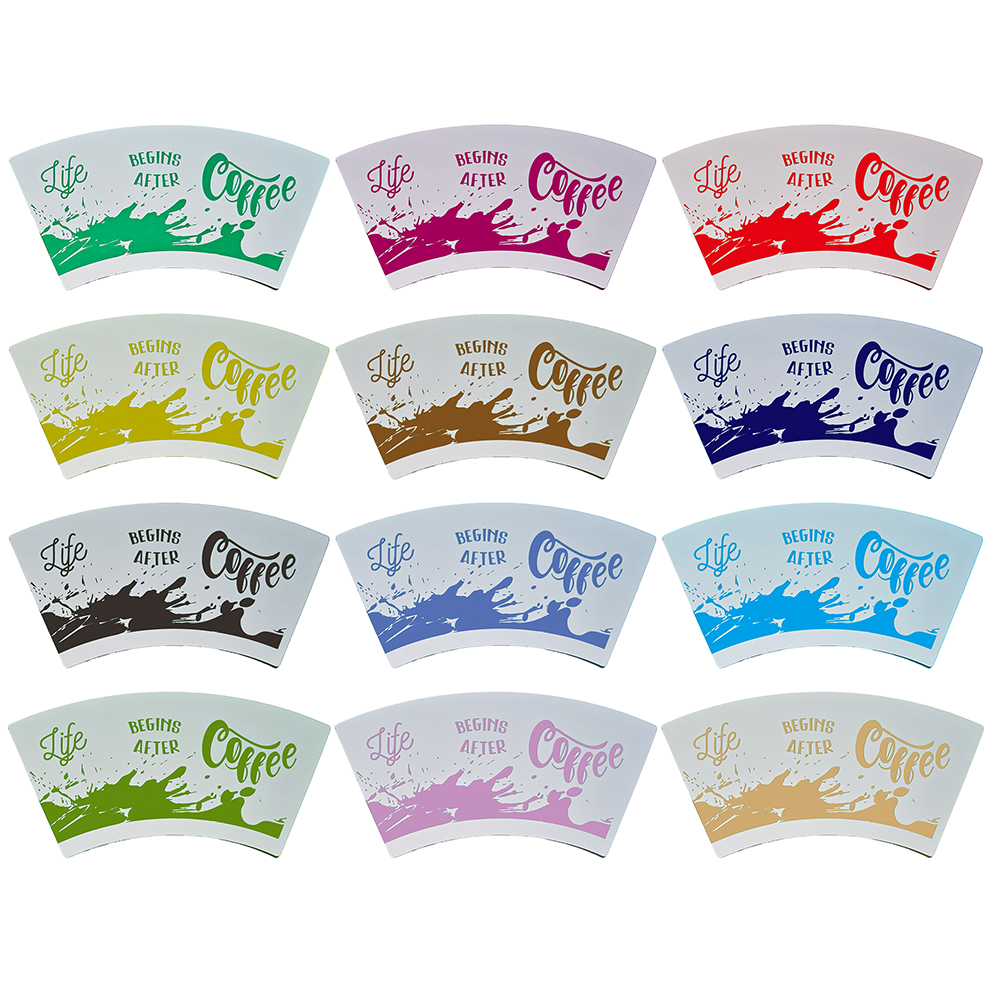
Featured Food Grade Wrapping Substrates
High-performance single and double-coated paperboard engineered for heavy-duty food wrapping, quick-service restaurant containers, and hot/cold beverage conversions.
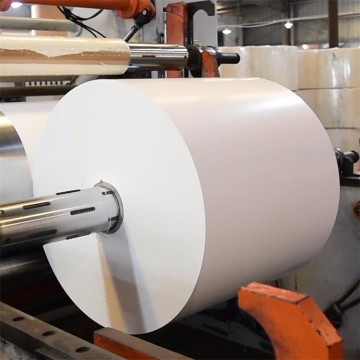
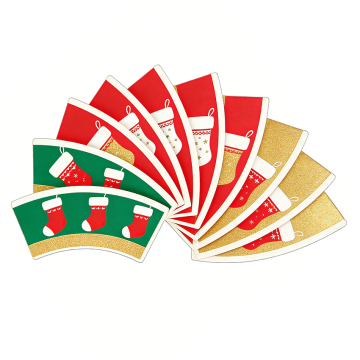
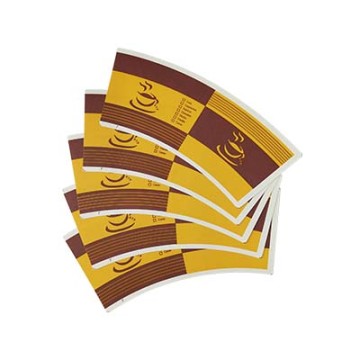
Industrial Landscape & Global Market Evolution
Examining the structural shift toward barrier-coated virgin pulp substrates in commercial foodservice, food retail, and FMCG packaging.
Superior Barrier Dynamics
Polyethylene (PE) coating delivers an impenetrable barrier against water vapor, animal fats, plant oils, and organic acids. Extrusion lamination forms a micro-smooth, pinhole-free film over high-bulk virgin fiberboard, preventing oil leakage and moisture absorption during long holding times.
PFAS-Free Regulatory Compliance
With global bans on per- and polyfluoroalkyl substances (PFAS) intensifying across North America and the European Union, clean mechanical PE lamination has emerged as the certified food contact benchmark, ensuring zero migration of toxic fluorine compounds into fatty or hot foods.
High-Speed Thermo-Sealing
Modern automated converting lines require optimal heat-seal responsiveness. Food grade PE coated paper offers consistent melting points and high hot-tack strength, enabling continuous leakproof ultrasonic or heat sealing on rapid packaging lines reaching up to 300 units per minute.
Commercial Industry Outlook: The Surge in Sustainable Food-Grade Barriers
The global market for food contact barrier paper is expanding rapidly, driven by strict single-use plastic restrictions and surging demand from multinational QSR (Quick Service Restaurant) chains, industrial bakeries, and chilled meat processors. Food-grade PE coated paperboard solves the critical dilemma of paper packaging: maintaining natural fiber stiffness while completely blocking liquid penetration. As consumers and enterprise buyers demand non-toxic, odorless, and certified hygienic food contact surfaces, premium virgin wood pulp combined with food-grade LDPE/HDPE extrusion has become the gold standard across over 100 regional markets worldwide.
Comprehensive Food Grade Wrapping Application Scenarios
From deep-freeze storage to searing fast-food applications, discover how customized PE coated substrates maintain structural and chemical integrity.
Quick-Service Fast Food Wrapping
Ideal for direct wrapping of hot burgers, crispy fried chicken, burritos, and tacos. The single-side or double-side PE barrier blocks scorching oil and grease seepage, keeping the exterior dry and crisp while retaining food warmth and steam freshness without sogginess.
Butcher, Fresh Meat & Seafood Wrap
Engineered with high tensile wet strength and heavy-duty poly lamination. Prevents blood, moisture, and liquid purge penetration during cold-chain transport, ensuring meat retains natural juices without adhering to or dissolving the underlying wrapping paper.
Artisan Bakery & Confectionery Liners
Designed for pastries, butter croissants, cream cakes, and artisan donuts. The non-stick, release-ready poly coating prevents butter saturation through the container, offering a pristine aesthetic display that preserves delicate pastry aromas and visual presentation.
Frozen Food & Ice Cream Packaging
Double-sided PE coating prevents deep condensation damage and structural fiber collapse in sub-zero freezers. Effectively blocks ambient freezer odor absorption while ensuring cups, tubs, and folding boxes preserve rigidity upon room-temperature thawing.
Takeaway Noodle & Soup Pail Conversion
Provides rigid, leak-proof bottom sealing for round paper bowls and folding food cartons holding boiling broths, gravies, and spicy sauces. Certified safe up to 100°C without hazardous chemical extraction or odor emissions.
Dry Grocery & Powder Sachet Sachets
Barrier against ambient humidity and air penetration for instant seasonings, sugar, milk powder, and dehydrated goods. Guarantees long shelf life and prevents clumping without requiring expensive multi-layer metalized foil laminates.
Company Profile & Manufacturing Excellence
Nanning Paperjoy Paper Industry Co., Ltd. — Pioneering Food Grade Paperboard Solutions Since 2006.
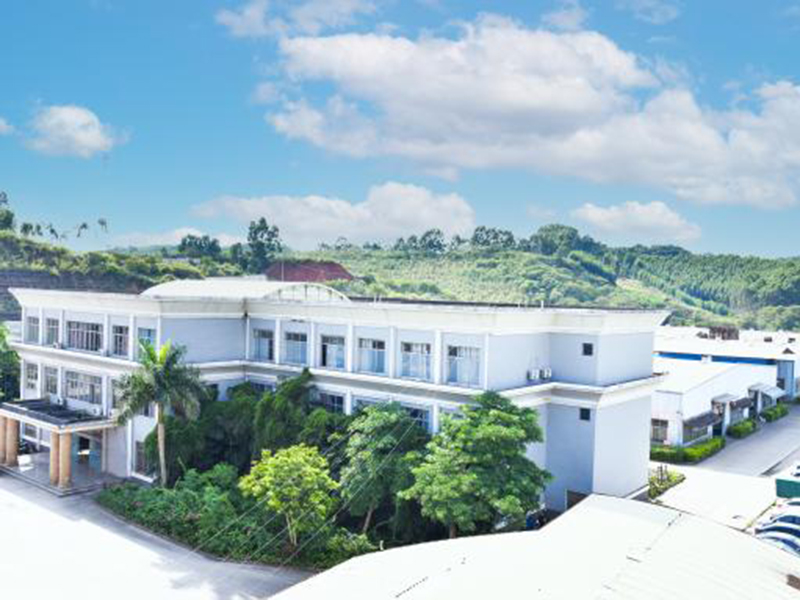
Nanning Paperjoy Paper Industry Co., Ltd. (“Paperjoy”) was established in 2006, with 200 employees and covers over 15,000㎡. Paperjoy is a professional manufacturer of raw materials for paper cup and packaging box, especially the PE coated paper roll, paper cup fan, cup bottom reel and C1S ivory board. We specialize in producing different kinds of PE coated paper raw materials. The annual production capacity is 60,000 tons.
Our factory is ideally located at the heart of Nanning city economic zone, which is very near to Qinzhou port, Beibu Gulf at the South of China. Our 200 well-trained and technically sound staff are motivated towards accomplishing a common goal of customer satisfaction and devoted to achieving the “Honesty, Mutual benefit, Win-Win cooperation” business philosophy.
Milestones & Continuous Development
Set up in 2006, engaged in paper cup paper PE coating industry. Paperjoy means good luck and happiness.
Developing B2B overseas market. Expanded the international market, targeting Asia, Africa, Europe, North America, etc.
Brand-new automatic production line launched; total annual capacity doubled to 60,000 tons/year.
Our products have been utilized in more than 2,000 factories and exported to over 60 countries across the globe.
Strategic Raw Material Supply & Integrated Advantages
Direct partnership with tier-1 forestry and paper pulp giants guarantees uninterrupted production and unmatched cost efficiency.
Our Corporate Vision
Bring health, safety, and eco-friendly packaging protection to every corner of the world through innovative sustainable paper technology.
Our Dual Mission
Mission 1: To be the world’s most trusted global supplier of food-grade paperboard and paper cup raw materials.
Mission 2: To create a prosperous, fulfilling, and joyful workplace for our entire dedicated team.
Certified International Quality & Food Safety Standards
PaperJoy’s quality assurance system governs every production stage, ensuring all food contact papers meet or exceed FDA, EU, and ISO safety standards.
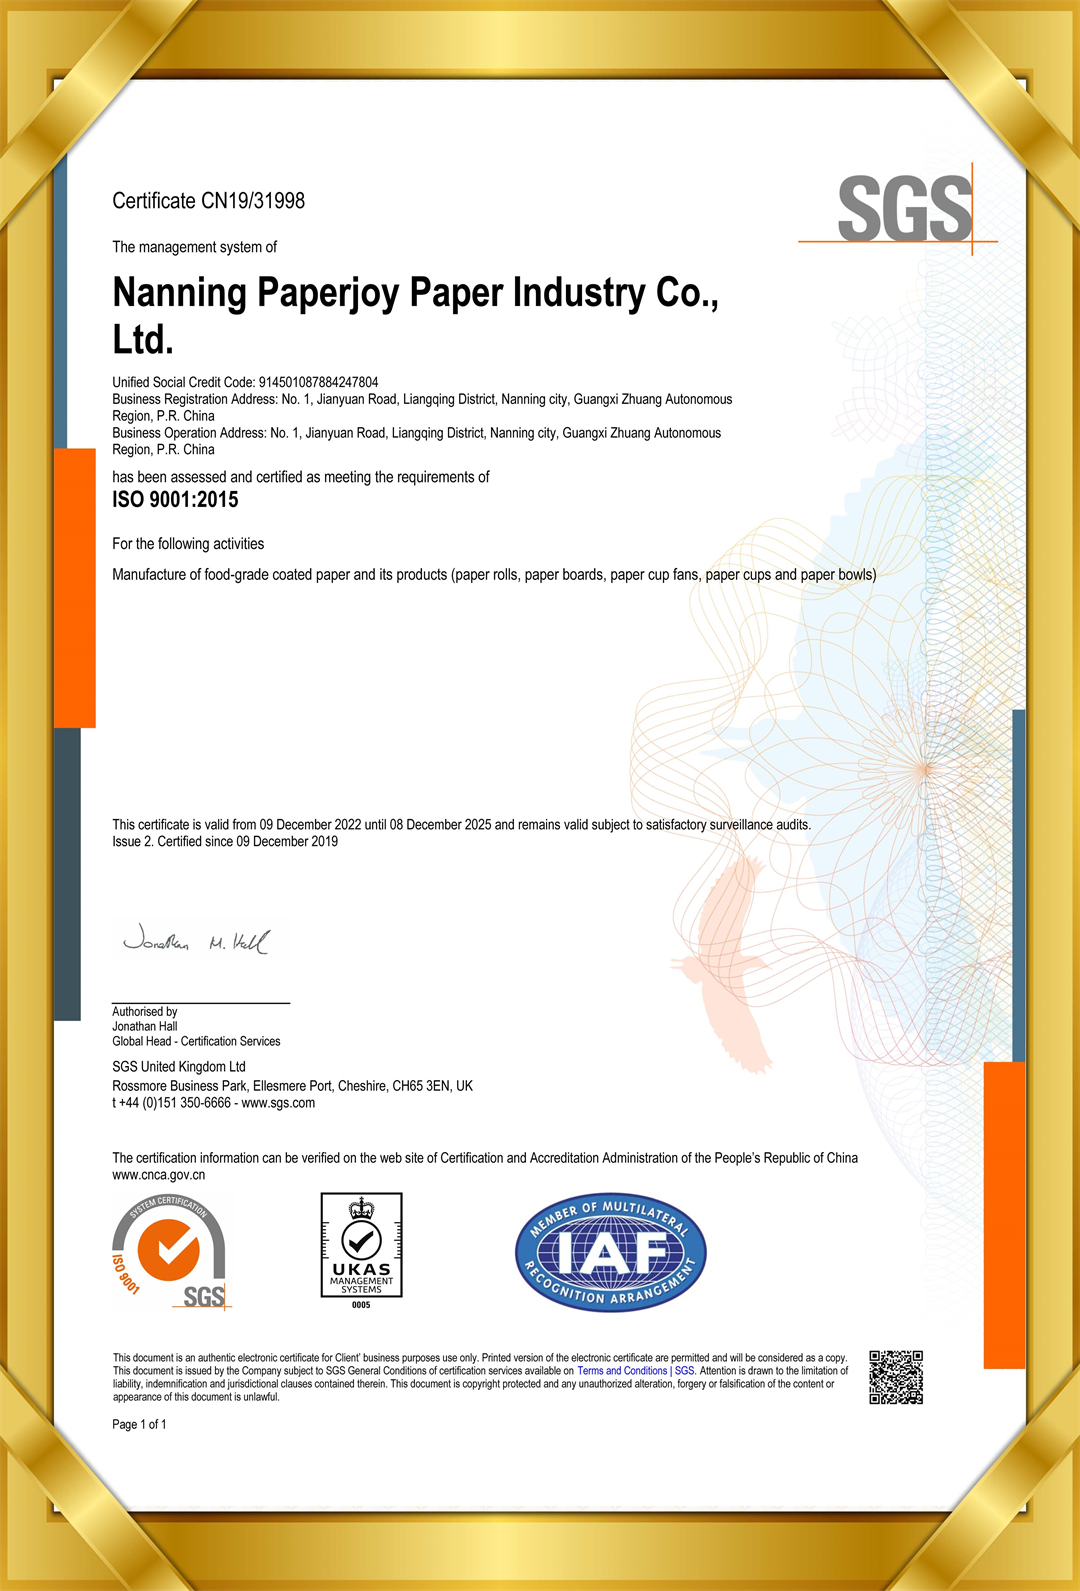
ISO 9001:2015
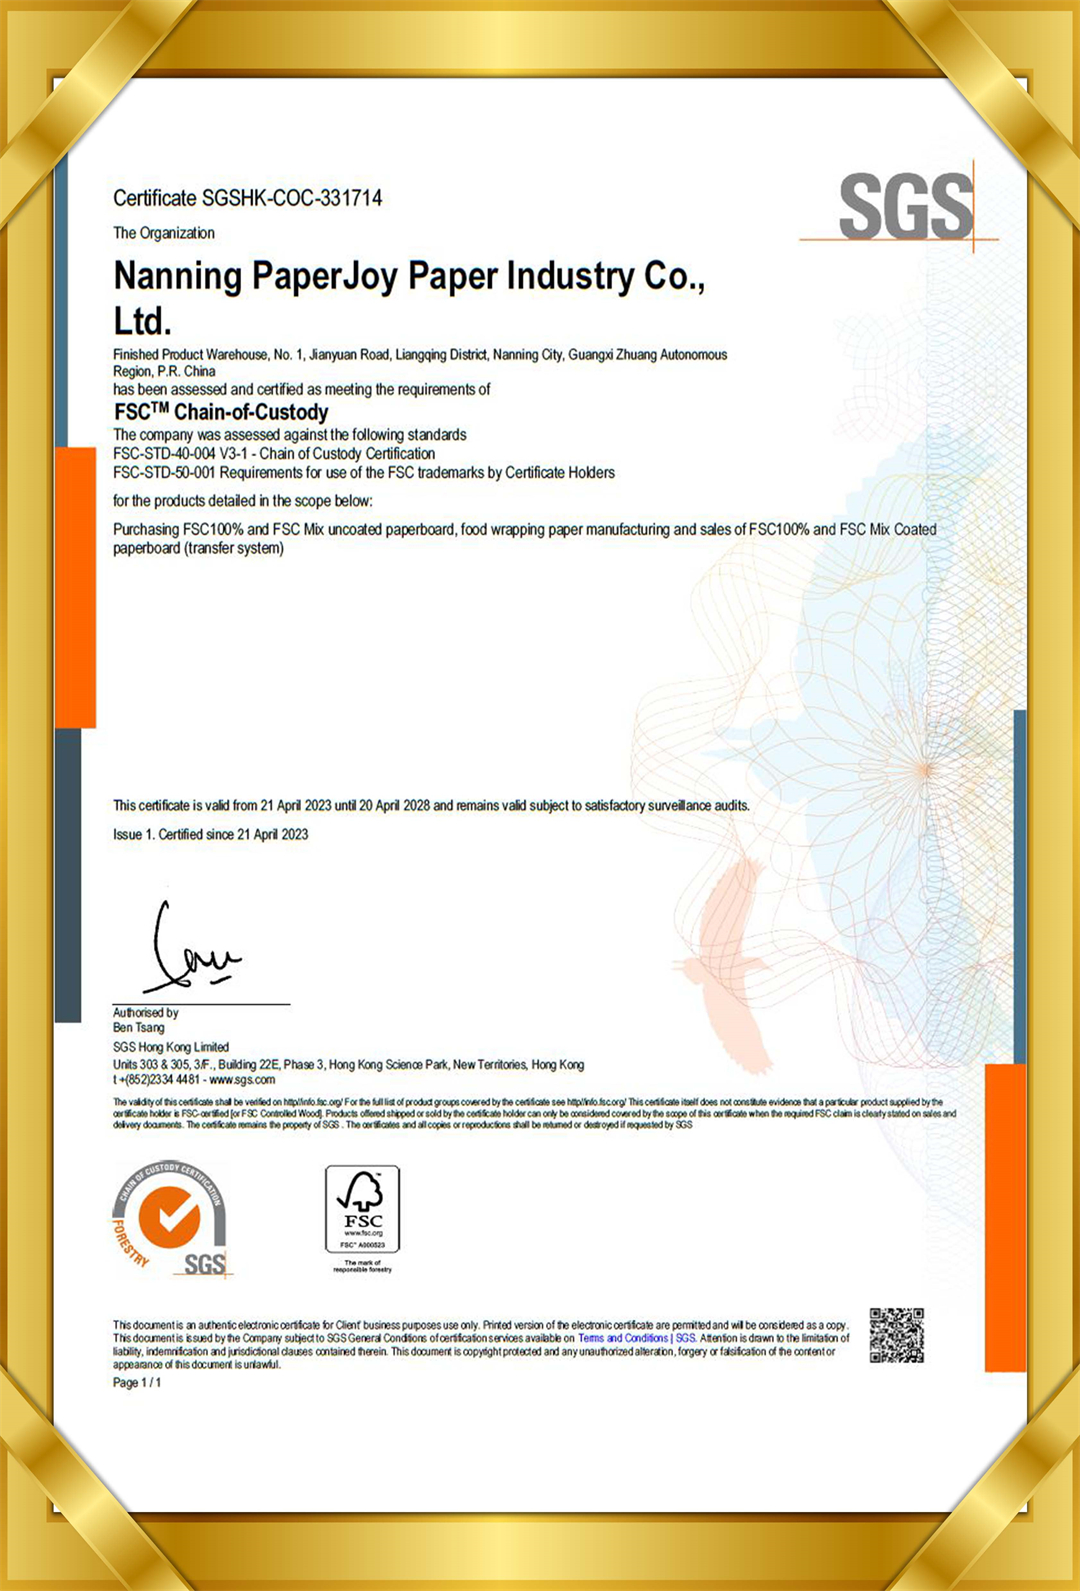
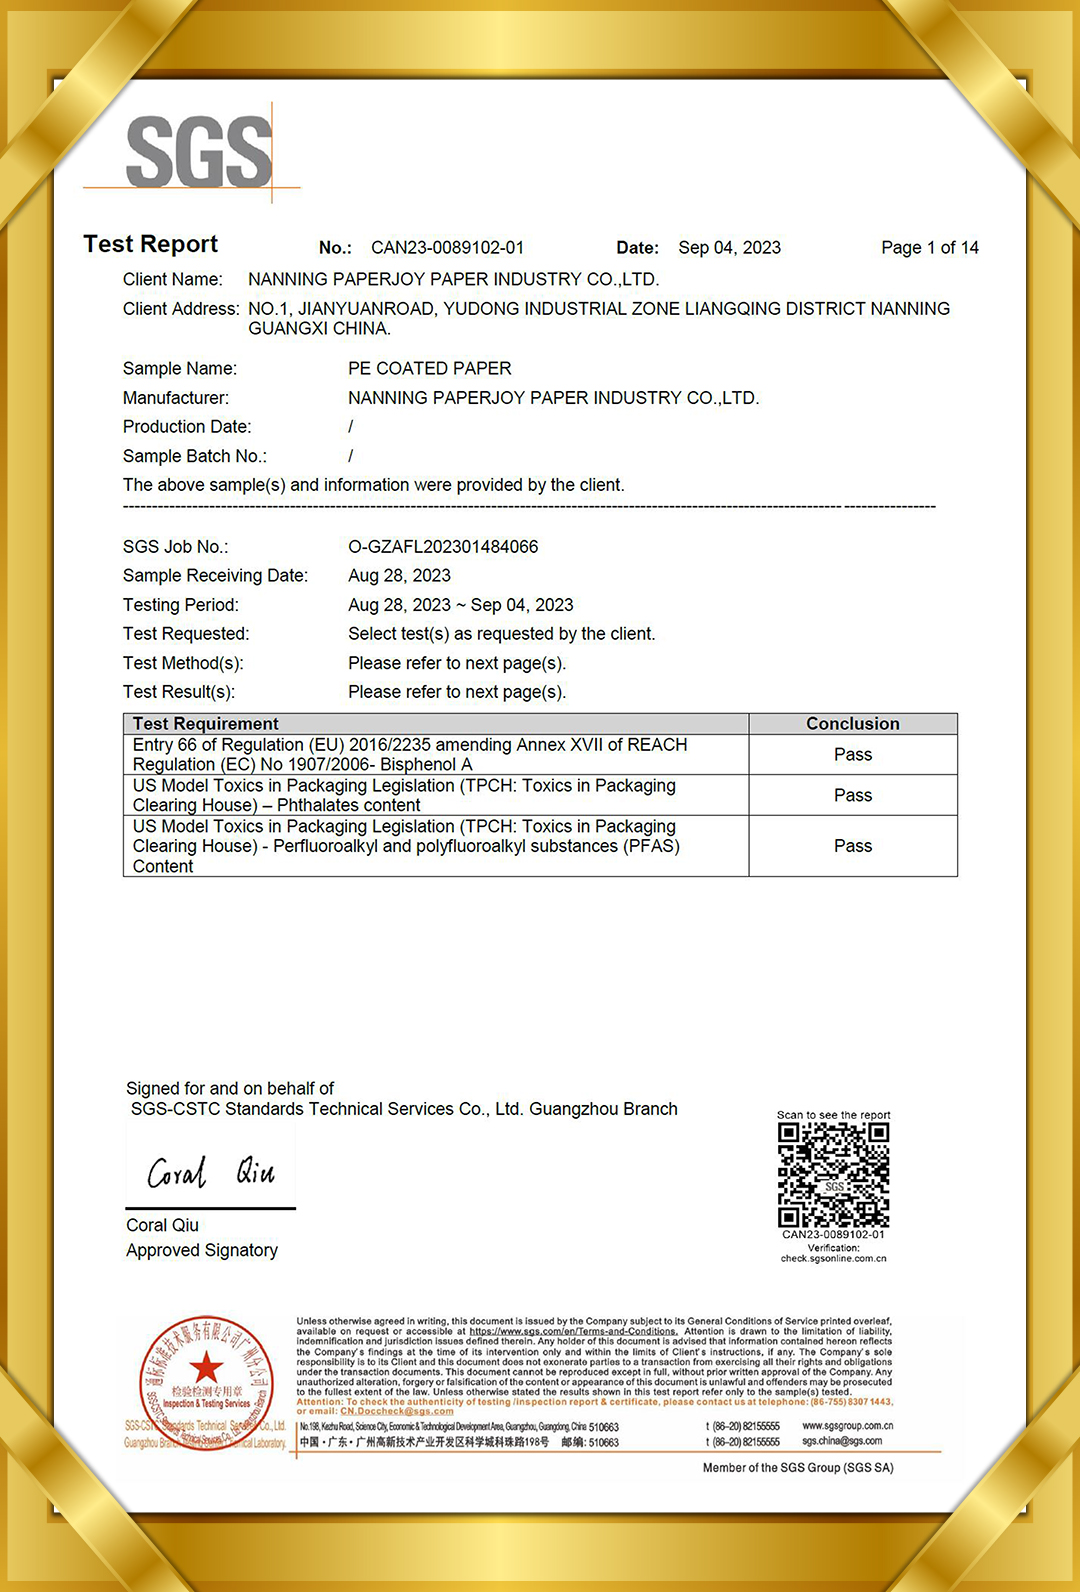
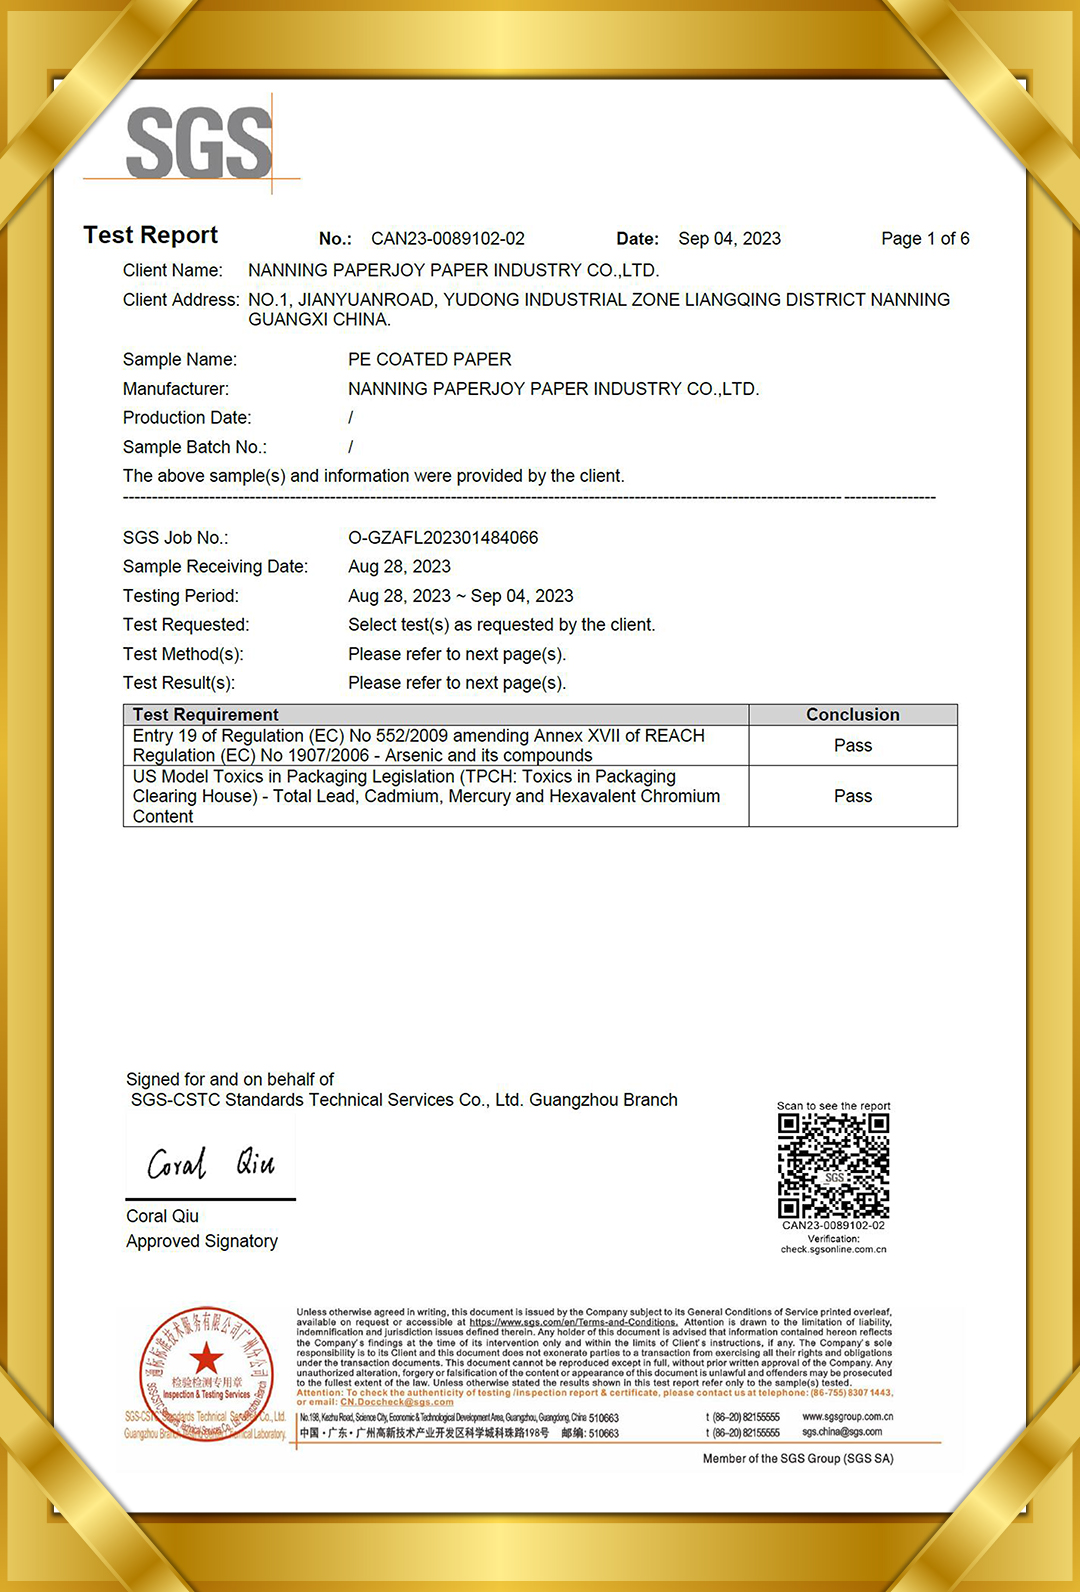
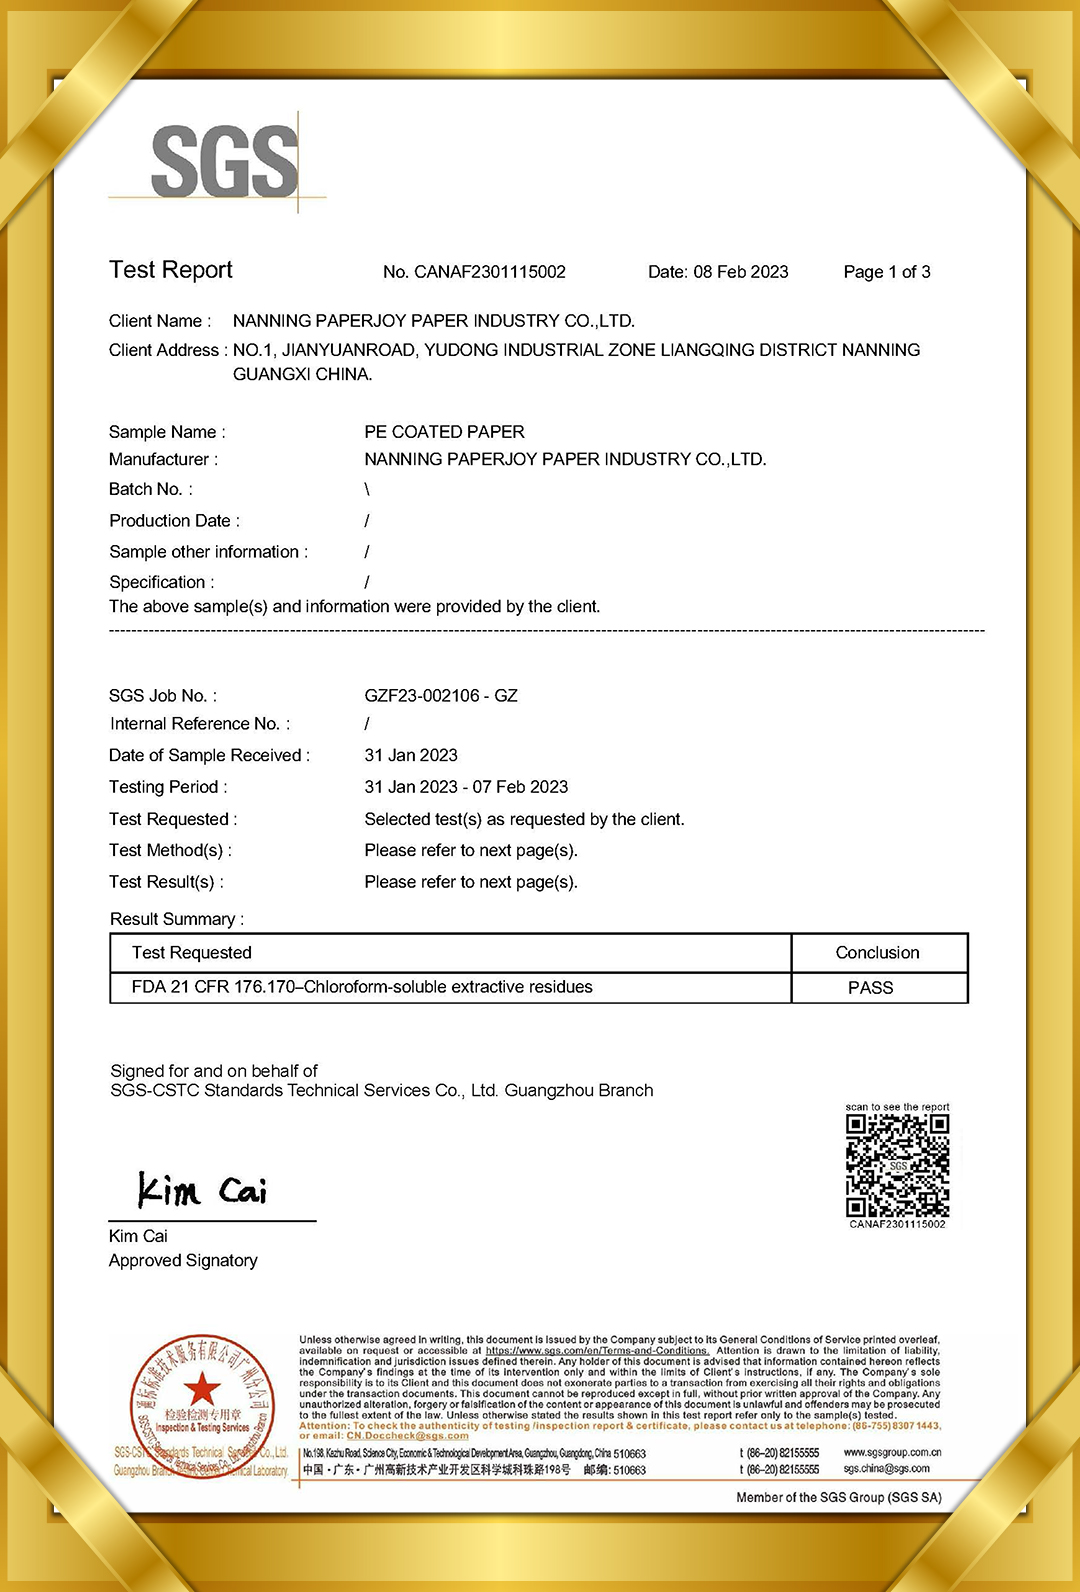
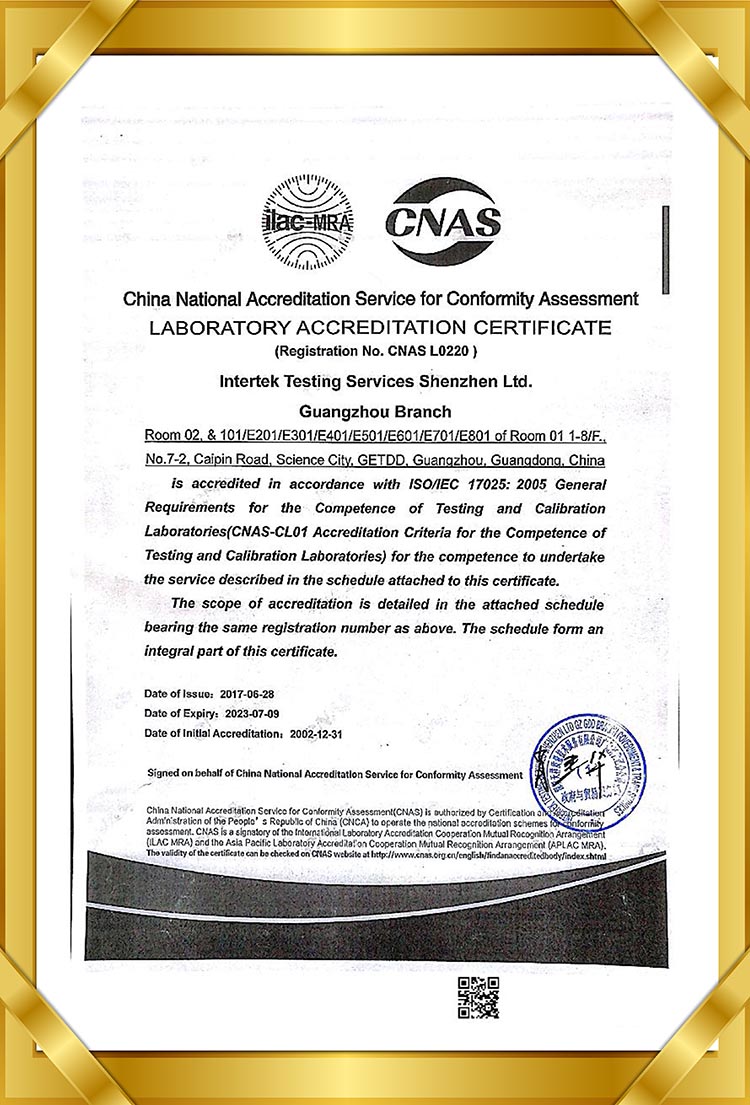 CNAS Laboratory Tested & Approved Food Contact Safety
Enterprise Honors & Community Recognition
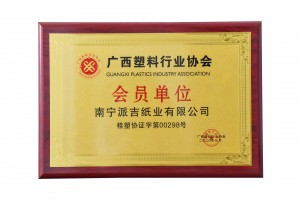
Plastics Association Member
Official designated processing unit for food-grade composite packaging.
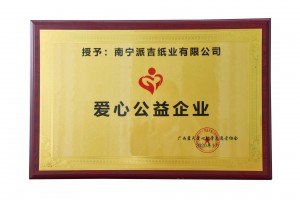
Charitable Enterprise Award
Committed to social welfare, environmental sustainability, and regional education.
Alibaba Gold Verified Supplier
Audited manufacturing capability, on-time delivery guarantee, and trade assurance.
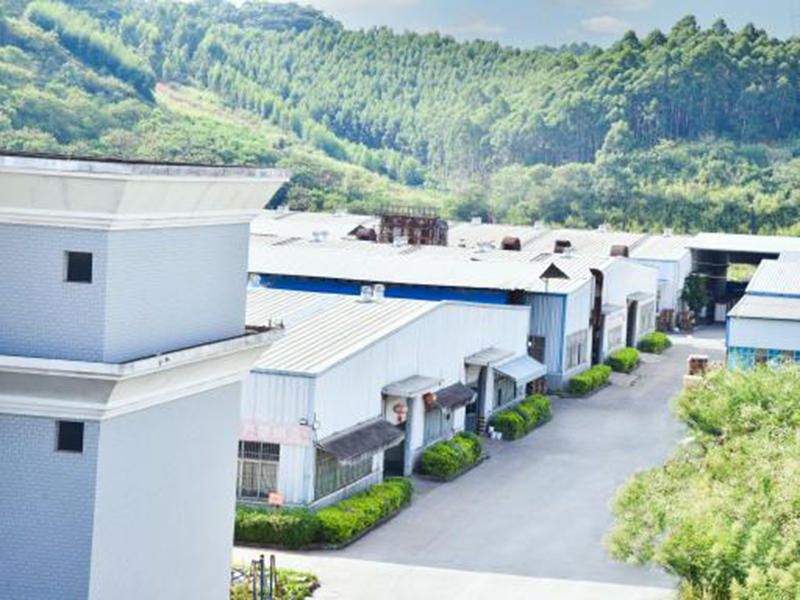
Factory Tour: Advanced Processing Equipment & Infrastructure
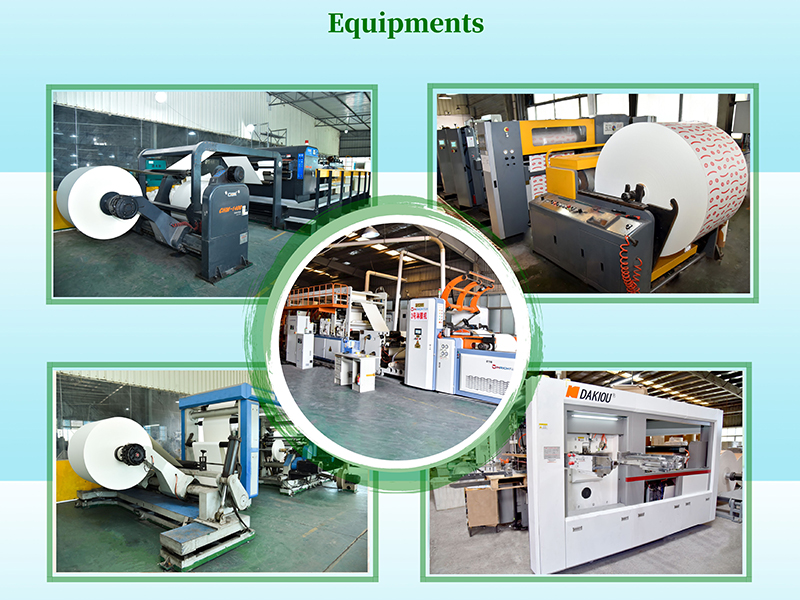
Equipped with over 45 sets of world-class automated machinery across 15,000 square meters of specialized clean production area.
Cutting-Edge Machinery Portfolio
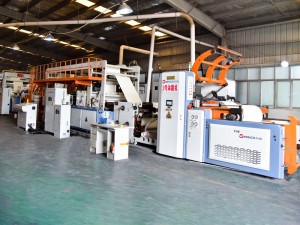
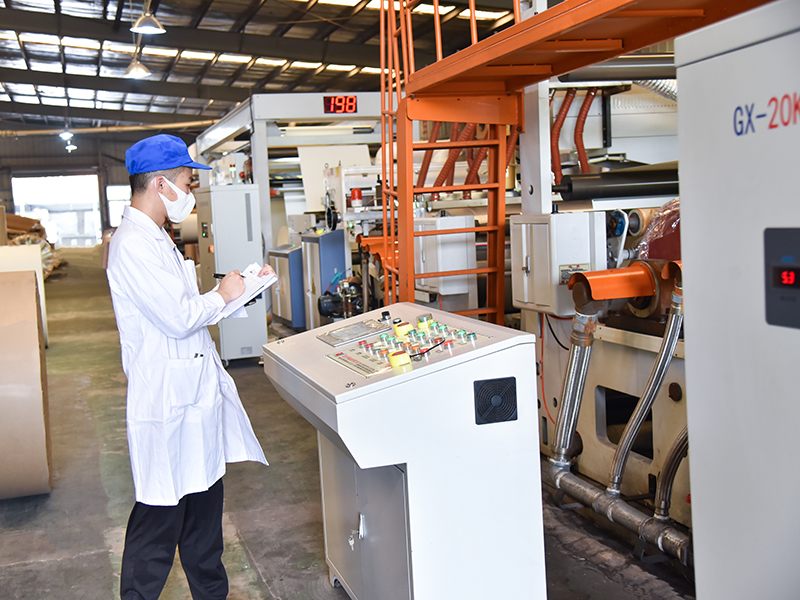
1. Three Extrusion Laminating Machines
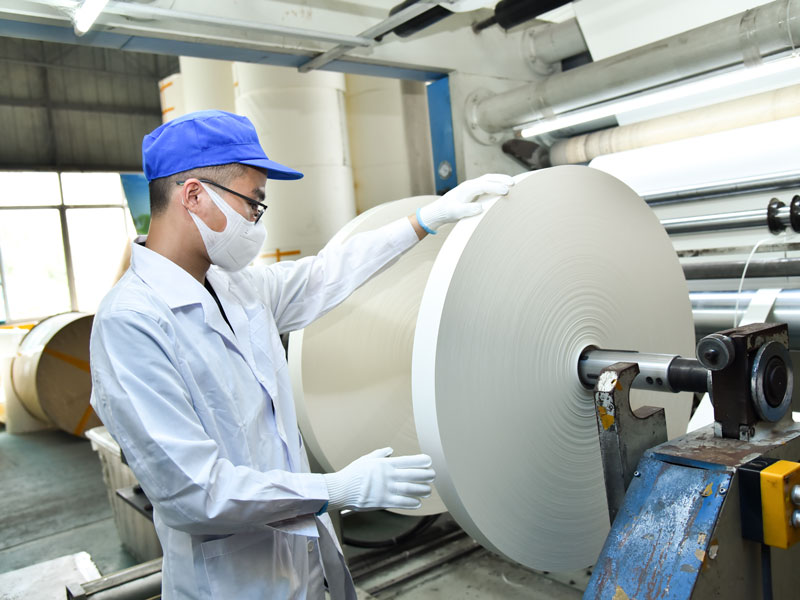
Used to produce premium single/double PE coated paper rolls. High-speed automatic lines designed for high-capacity bulk demand.
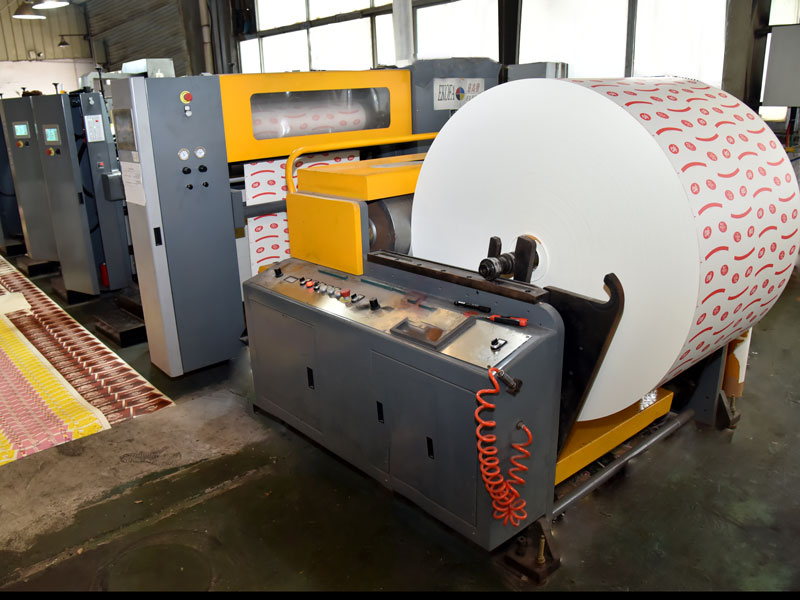
2. Three Six-Color Flexo Printing Lines
High-speed flexographic printing for paper cup fans and wrapping wrappers with water-based non-toxic food inks.
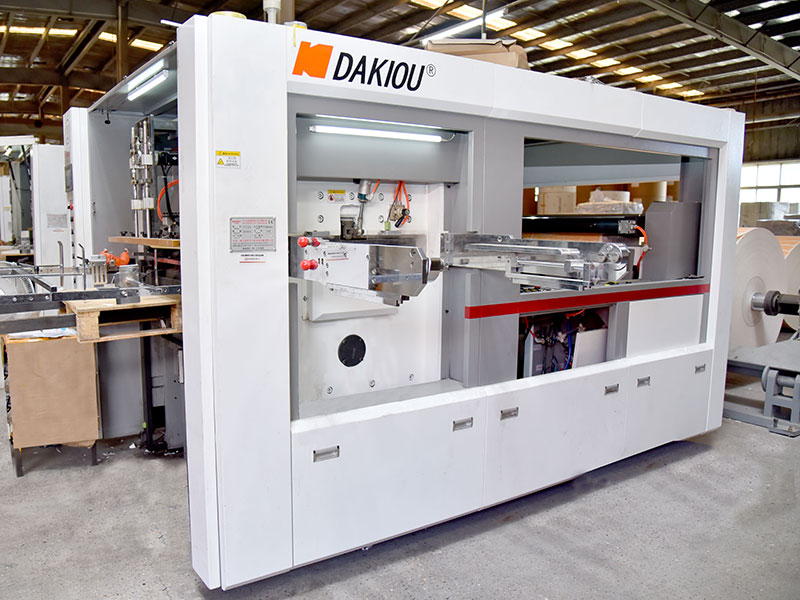
3. Eight Automatic Die-Cutting Units
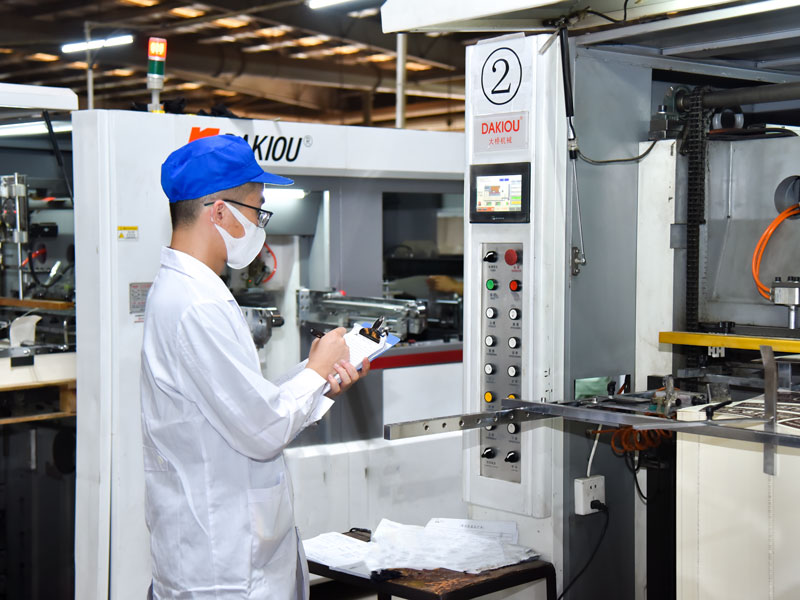
Ultra-fast die-cutting for fan blanks and wrapping sheets with an exceptional speed exceeding 280 sheets/min.
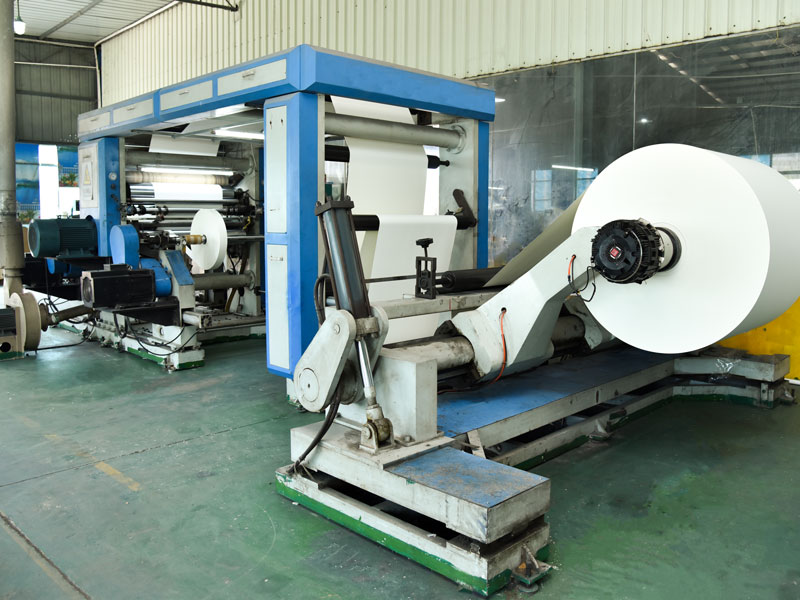
4. Precision High-Speed Slitting Machine
Custom width slitting engineered for making continuous paper cup bottom rolls and tape rolls.
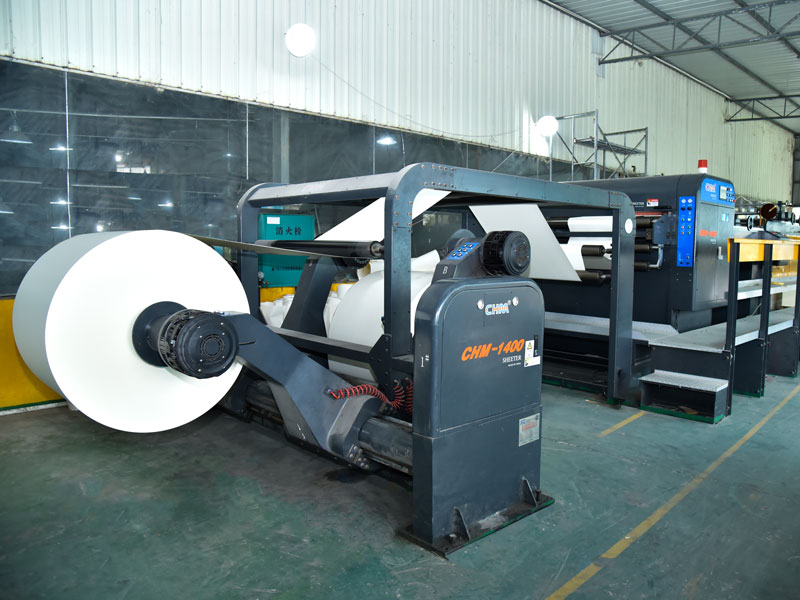
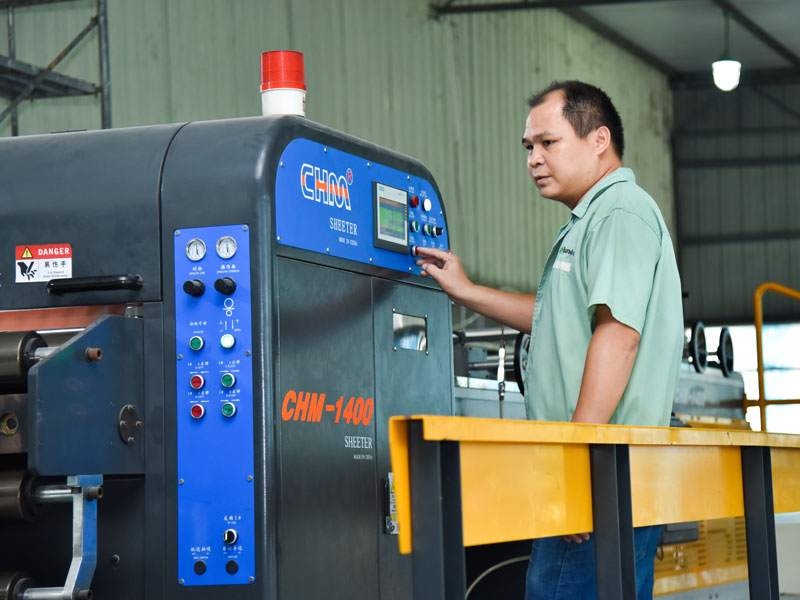
5. High-Speed Sheet Cross-Cutting Machine
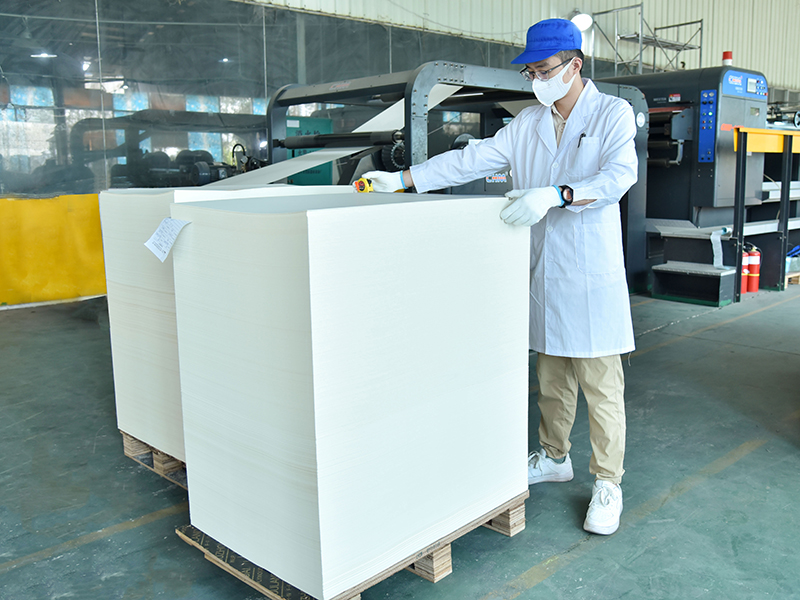
Precision cutting of custom size PE coated paper sheets for food wrapping and box conversion.
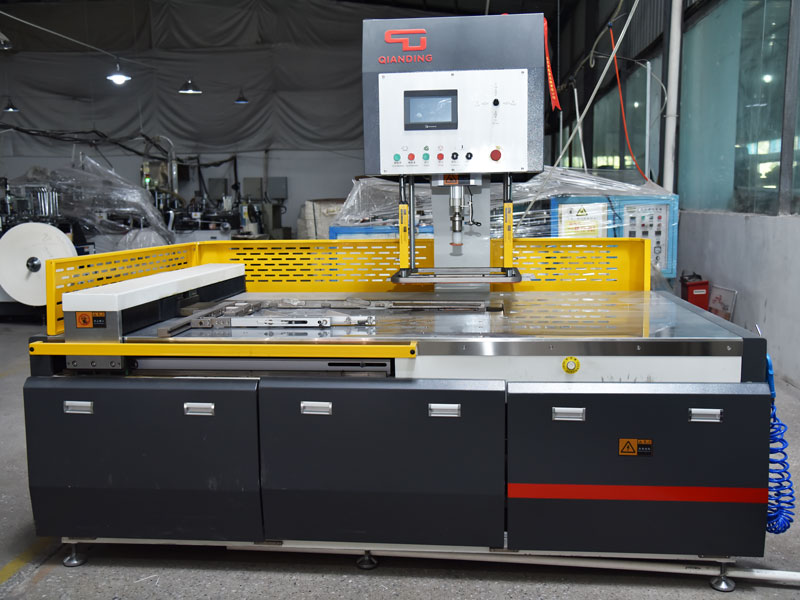
6. Eleven Standard Waste Stripping Units
Automatic stripping machines remove edge scrap rapidly to deliver clean, ready-to-use cup blanks and wrapping sheets.
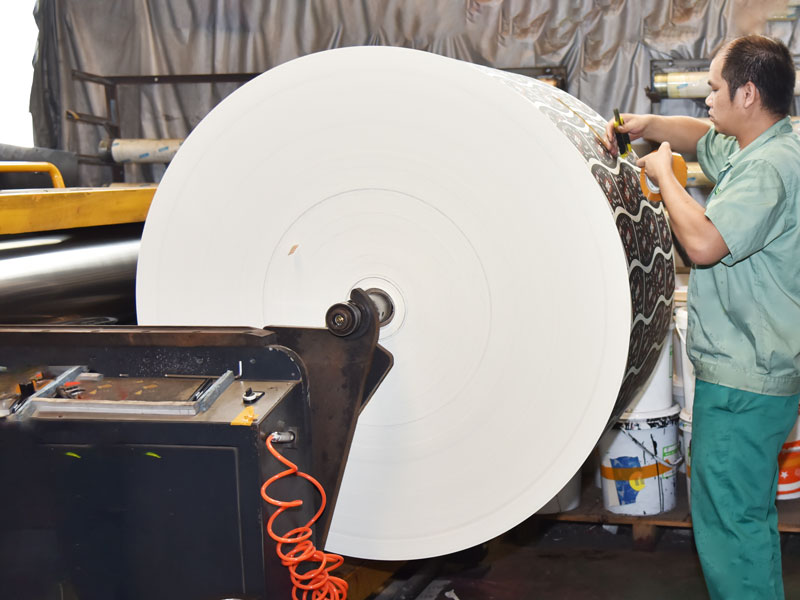
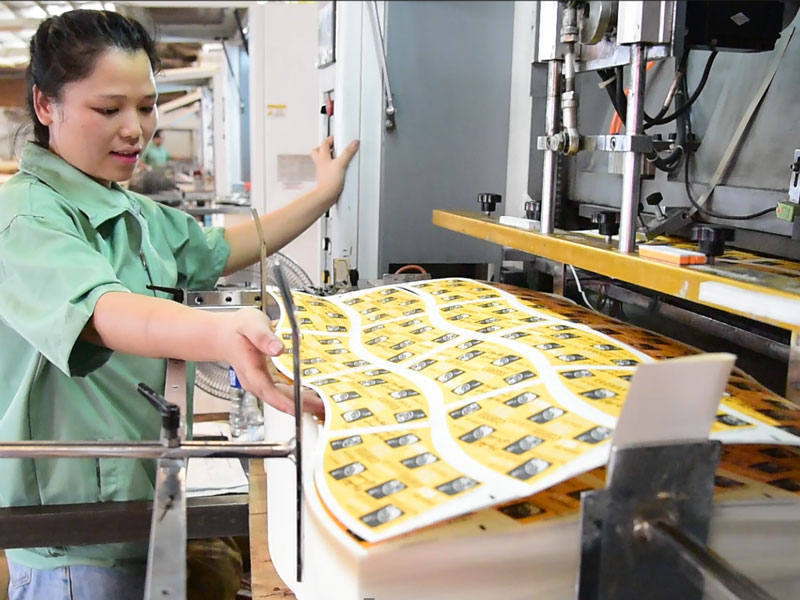
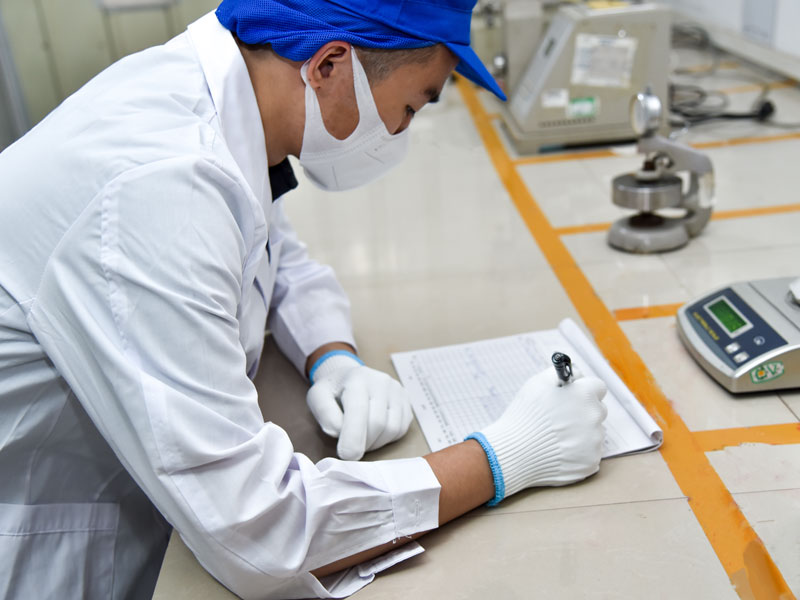
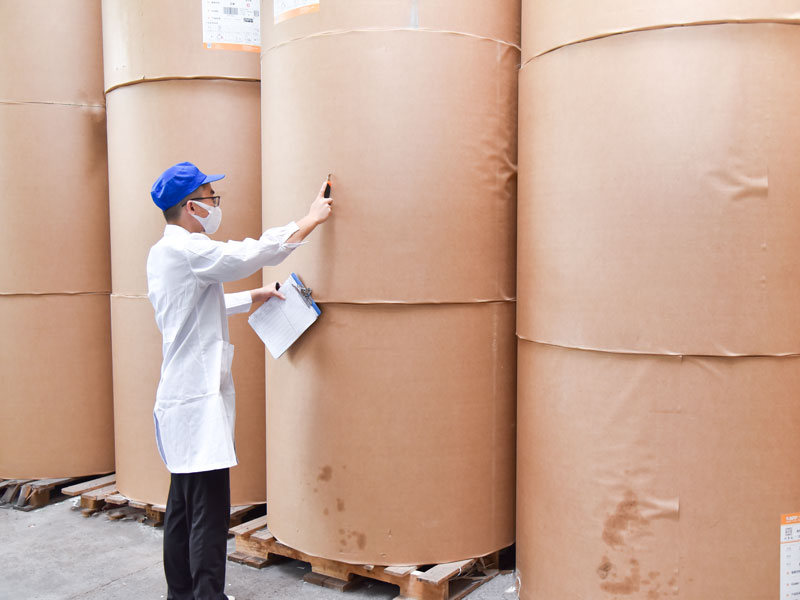
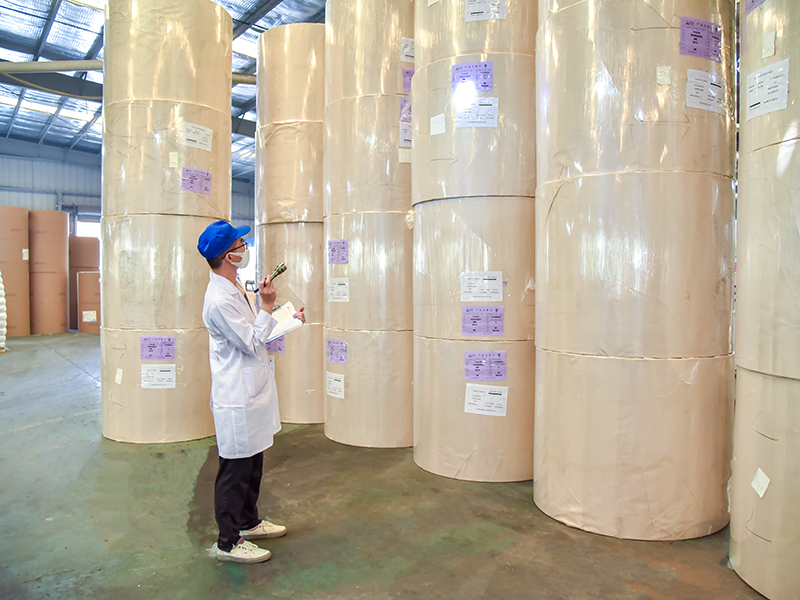
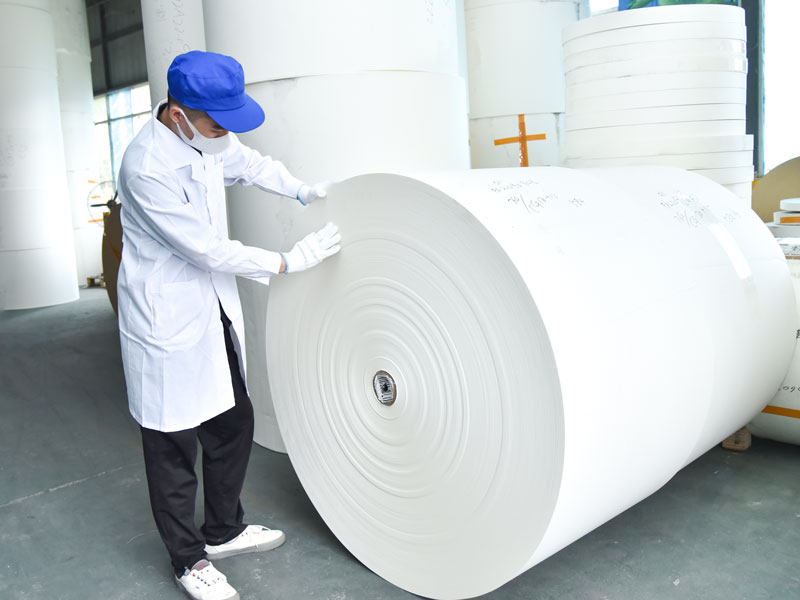
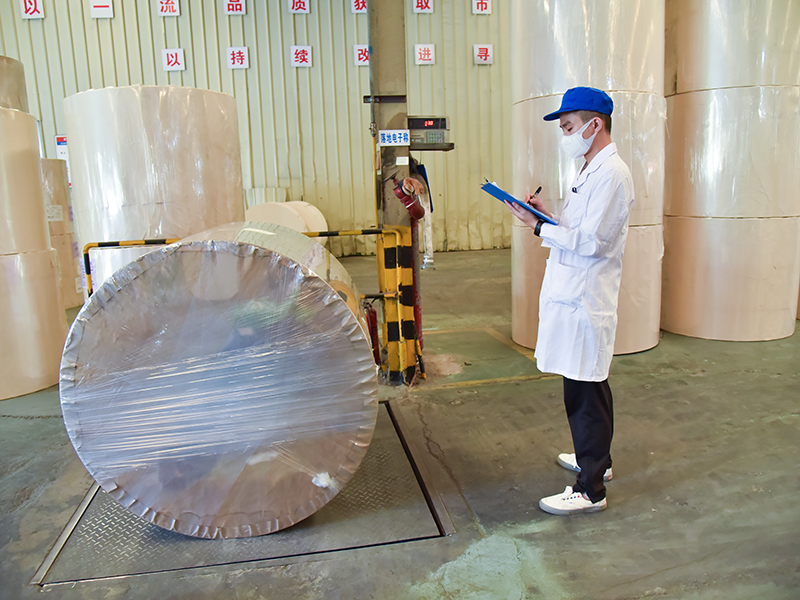
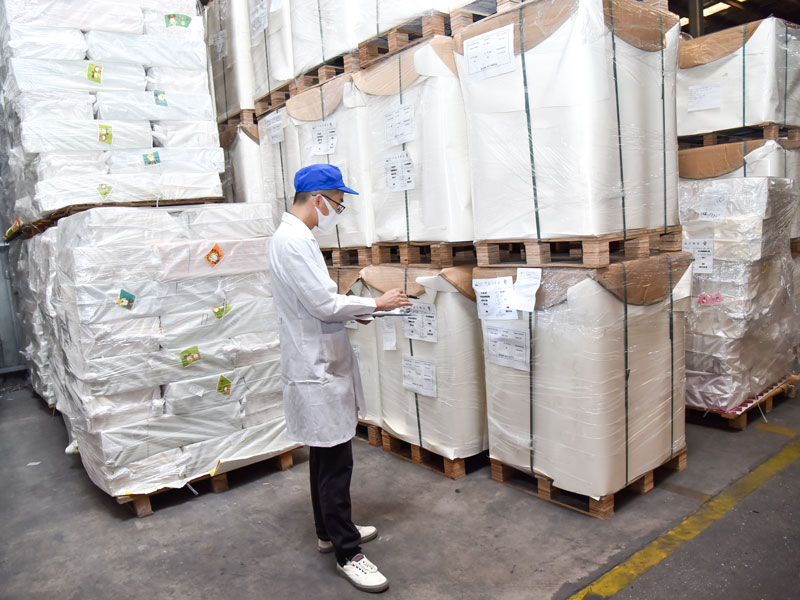
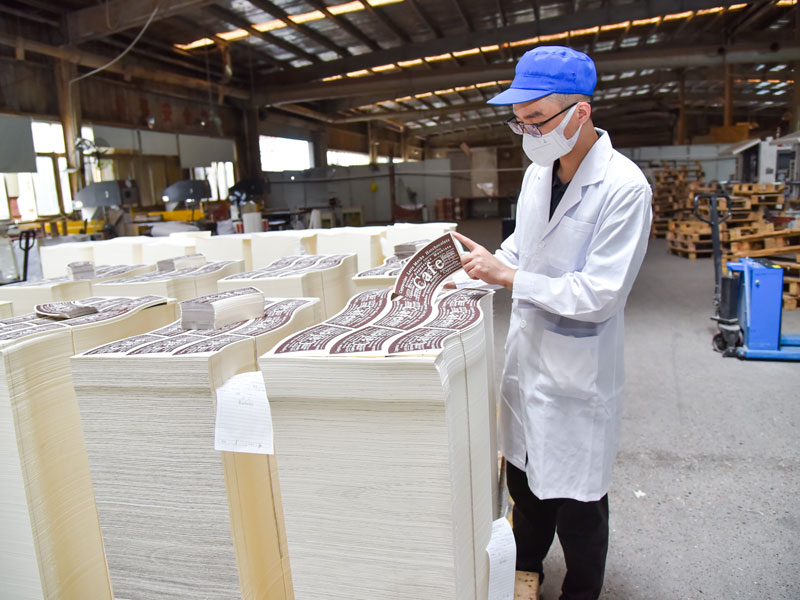
Personnel Operation & Flow Execution
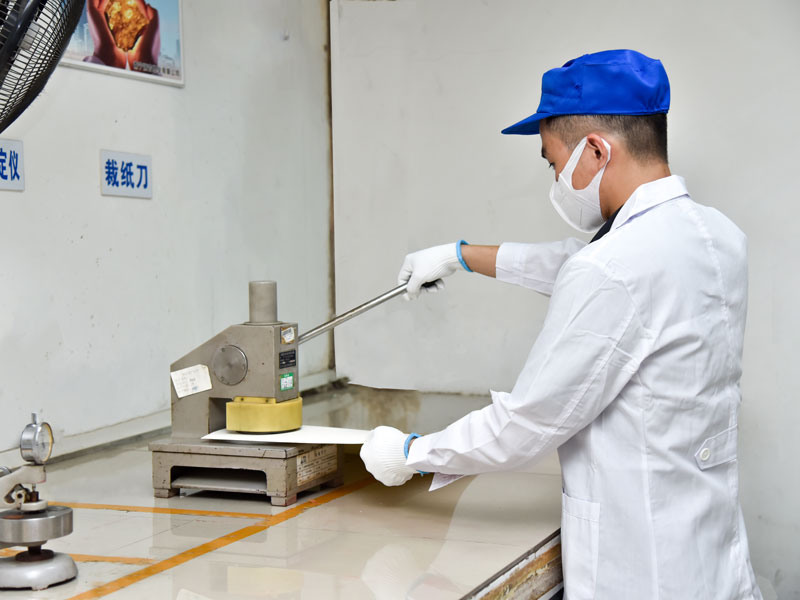
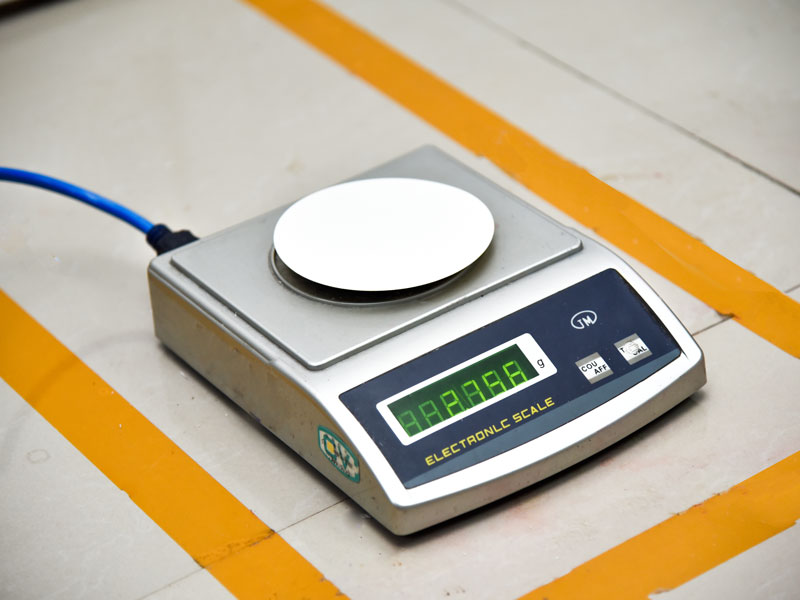
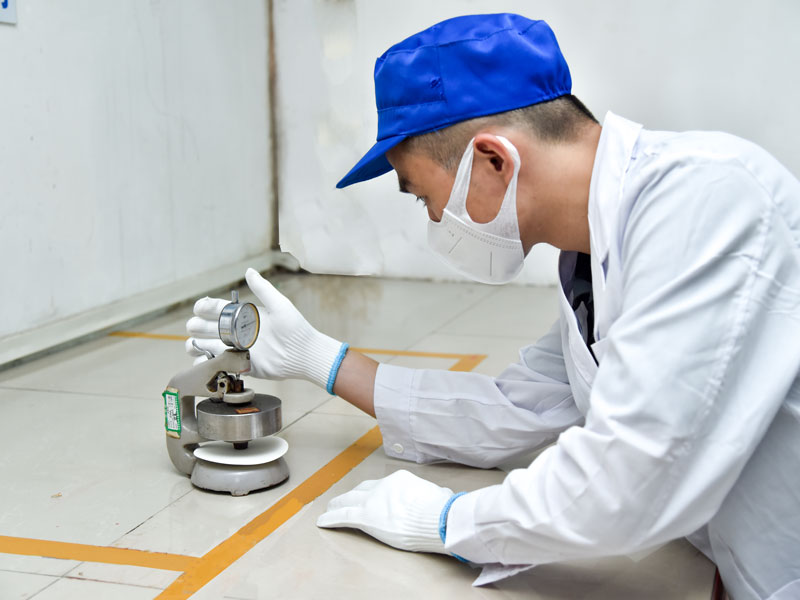
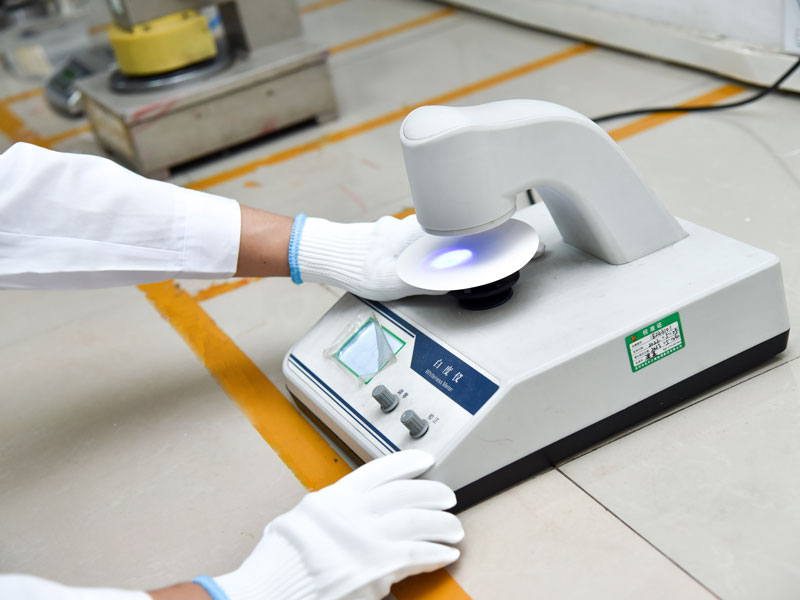
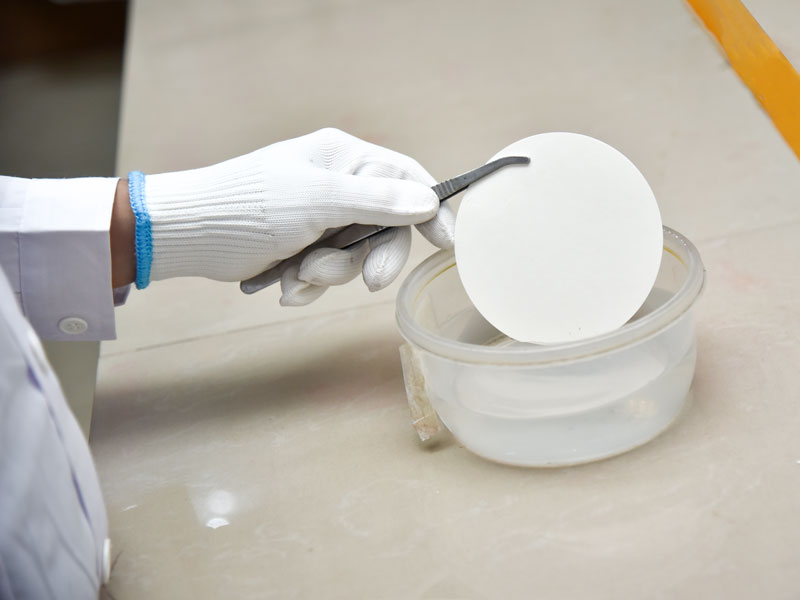
Multi-Stage Quality Inspection & Testing Rigor
Every single master batch undergoes strict laboratory verification to ensure 100% defect-free barrier reliability and food safety compliance.
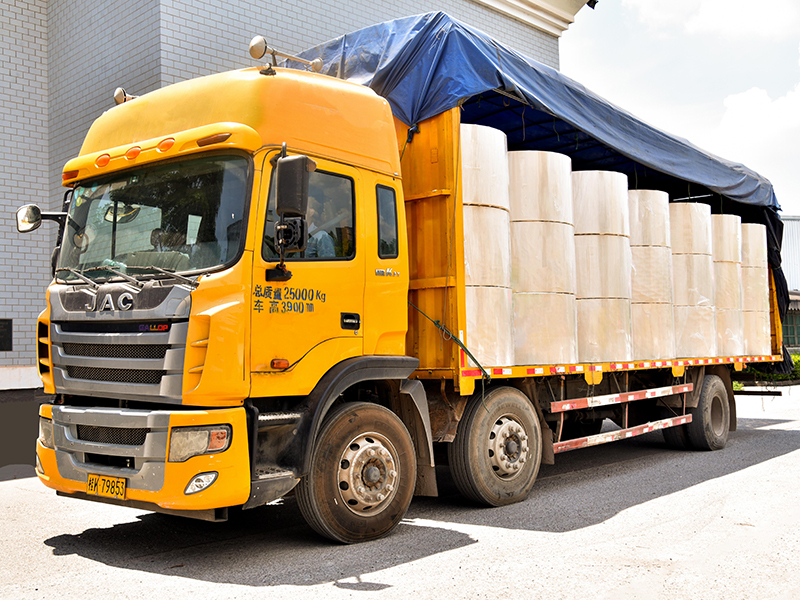
Packaging & Seaworthy Global Logistics
Triple-layer moisture protection, reinforced corner protection, and fumigated pallets ensure your cargo arrives in pristine converting condition.
Why Choose Paperjoy as Your Primary Food Wrapping Partner?
Empowering packaging distributors, box converters, and food chains with unmatched reliability, bespoke engineering, and factory-direct pricing.
Customized Base Paper & Sizing
We provide customers with customized paperboard raw material products matching specific caliper (150g – 400g), custom sheet dimensions, and slit widths to suit diverse food packaging applications.
Broad Product Portfolio
We offer a comprehensive range including PE Coated Paper Rolls, PE Coated Paper Sheet, Cup Fans, C1S Ivory Board, and Kraft Paper Roll for all packaging conversions.
Free Samples & Fast Quotes
We provide free samples and rapid quotes to ensure customers can test paper curl, heat sealability, barrier performance, and flexo print clarity firsthand before ordering.
Fast Lead Times & Urgent Delivery
With an integrated production workflow and strategic raw base paper reserves, standard large orders ship within 7-15 working days, ensuring your converting lines never stop.
Technical Process Consulting
Our veteran paper engineers assist with machine calibration, die-cutting tooling design, optimum PE grammage selection, and ultrasonic sealing parameter optimization.
24/7 Dedicated Support
Dedicated bilingual customer support teams provide personalized order tracking, container optimization, documentation assistance, and responsive after-sales service.
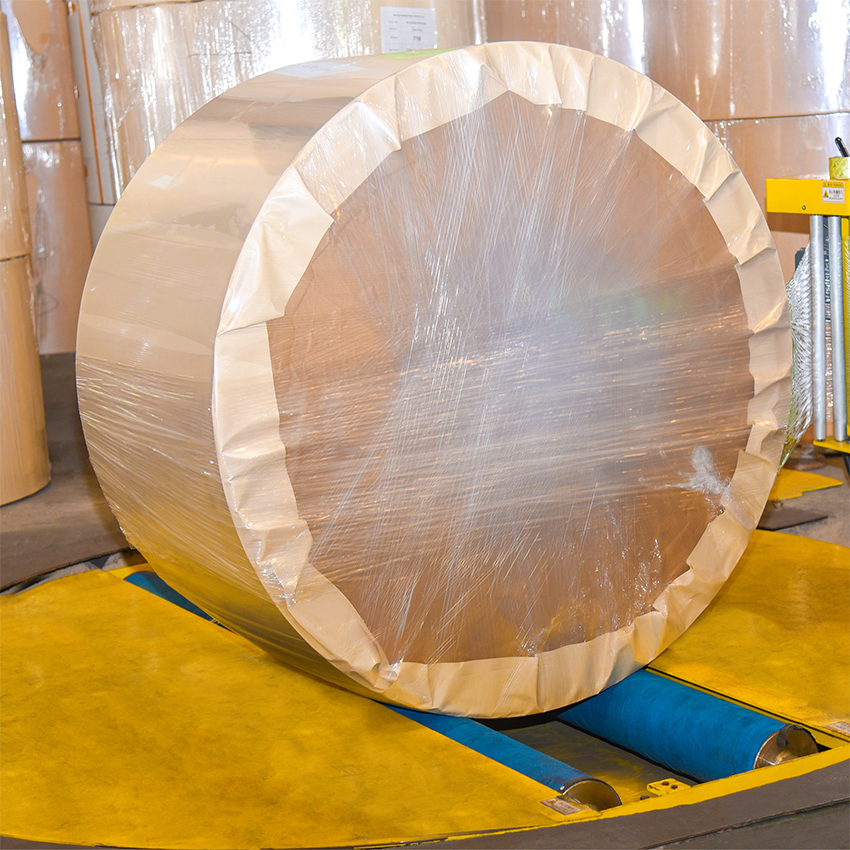
Strict Quality Control System
Source wood pulp verification to final burst resistance.
- Raw material inspection: High-purity virgin pulp & pure resin polymers.
- Real-time web monitoring: Automated optical inspection during coating.
- Finished product testing: Tensile, Cobb absorption, and grease testing.
- Batch sampling records: 100% full-process traceability for 3+ years.
Large-Scale Production Capacity
60,000 tons yearly output supporting bulk tenders.
- Multi-line extrusion: Rapid switching between 150g – 400g board.
- Expansive warehouse: 15,000 ㎡ modern covered manufacturing zone.
- Continuous R&D: Constant upgrade of extrusion coating heads.
- Direct factory pricing: Zero middlemen markups for maximum margin.
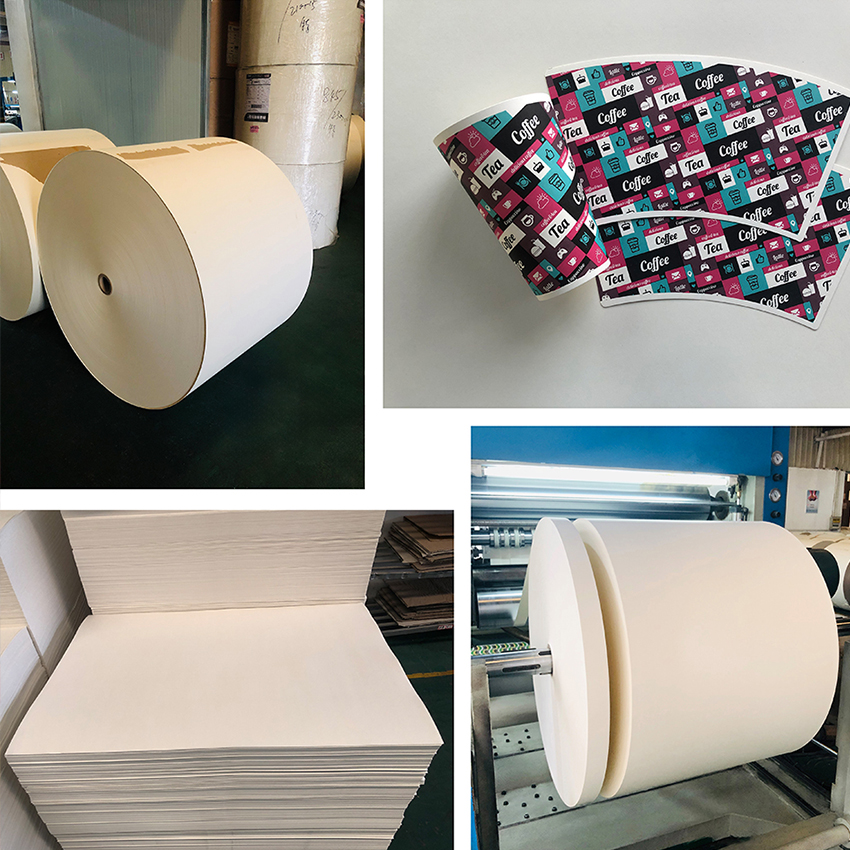
Tailored Converting Solutions
Engineered to match your exact converting parameters.
- Custom paperboard thickness: 150g – 400g with 10g – 35g PE coating.
- Custom surface finish: Matt, glossy, or embossed barrier textures.
- Food-grade flexo print: High-definition multi-color branding.
- Free pre-production proofing: Free sample rolls for machine trials.
Eco-Friendly & Sustainable
Sustainably managed forestry and low-carbon processing.
- 100% virgin pulp: Sourced strictly from certified sustainable timber.
- Odor-free extrusion: Non-toxic, safe for hot food wrapping.
- Biodegradable options: PLA and water-based barrier options available.
- Energy-efficient operations: Reduced carbon footprint manufacturing.
Explore Our Complete Food Grade Paperboard Product Catalog
Full spectrum of PE coated paper rolls, sheets, printed blanks, and cup raw materials available for immediate global export.