



High-Performance PE Coated Food Grade Substrates
Commercial Dynamics & Global Evolution of PE Coated Food Grade Wrapping Sheets
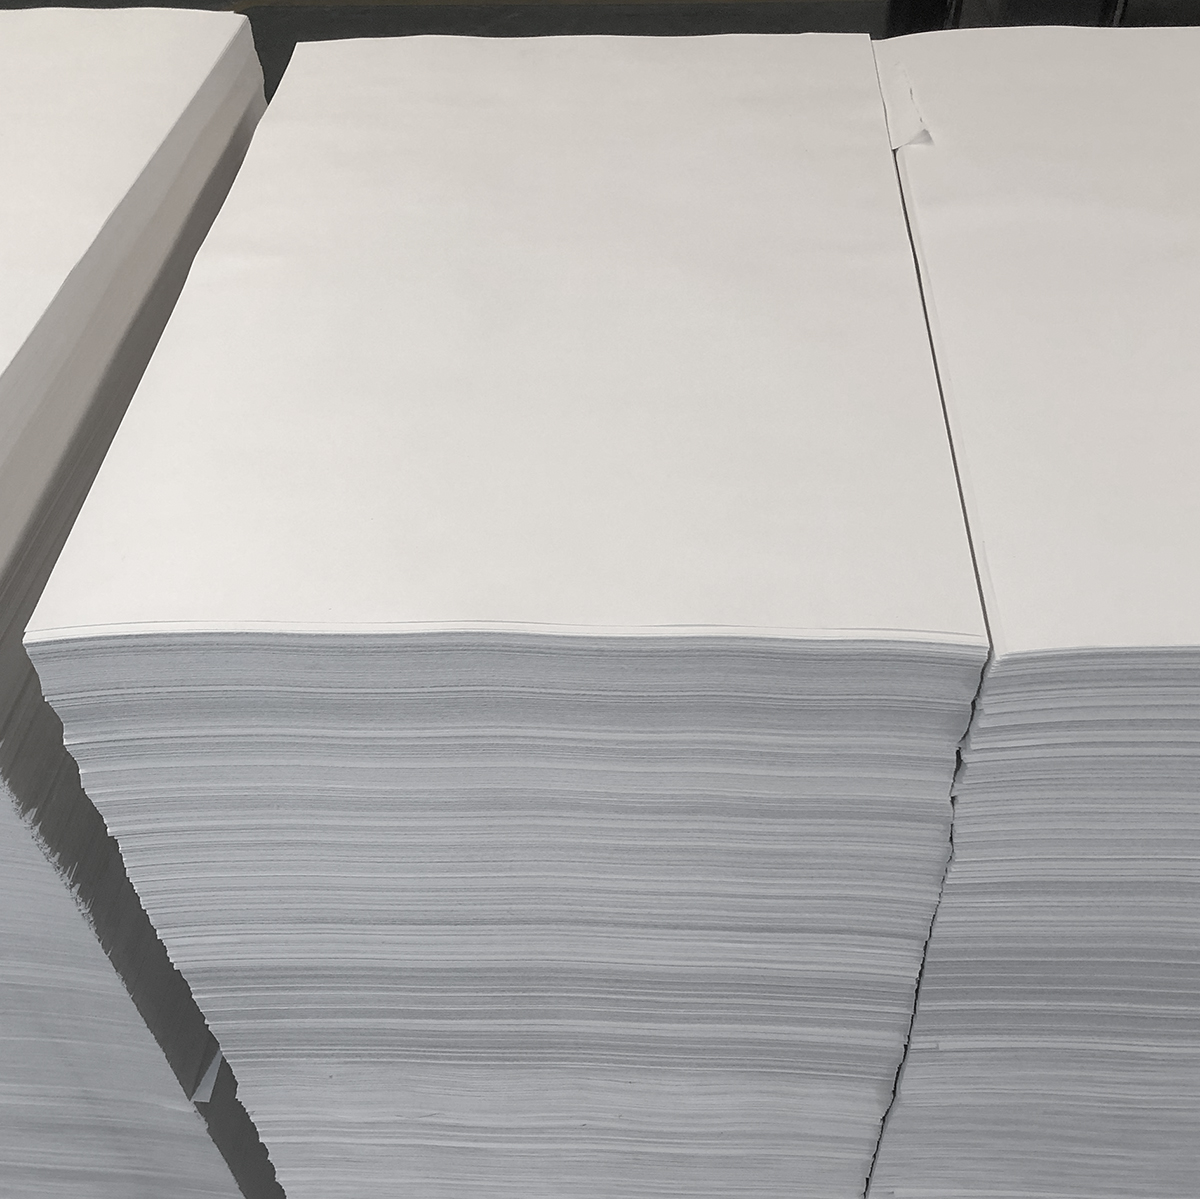
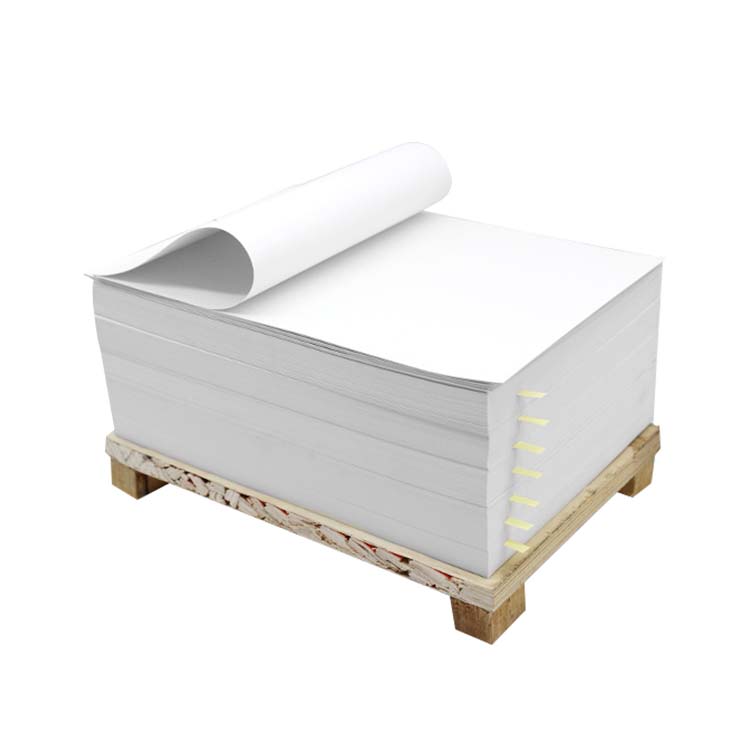
The global market for flexible food packaging continues to experience seismic structural adjustments, accelerated by worldwide single-use plastic restrictions, stricter food contact safety statutes, and evolving consumer habits in quick-service restaurants (QSR) and takeaway delivery logistics. Within this dynamic framework, PE coated paper sheet for food grade wrapping has cemented its standing as an indispensable barrier medium across modern food supply chains. By synergizing high-purity virgin wood pulp paperboard with thin-film polyolefin extrusion coatings, these engineered sheets offer an optimal compromise between biological renewability, grease/moisture impermeability, cost competitiveness, and high-speed converting runnability.
From an industrial standpoint, the food grade wrapping sheets segment is transitioning rapidly beyond generic waxed and silicone-treated sheets toward precision-engineered multi-layer extrusion structures. Traditional greaseproof papers often suffer from grease pinholes, poor heat sealability, or susceptibility to moisture softening. Conversely, polyethylene (PE) extrusion lamination deposits a continuous, non-porous thermoplastic barrier film directly onto the cellulose substrate without toxic adhesives or hazardous solvents. This creates a hydrophobic, lipophobic shield that satisfies the strictest migration thresholds established by global regulatory authorities such as the US Food and Drug Administration (FDA) and the European Food Safety Authority (EFSA).
The Crucial Regulatory Driver: Elimination of Fluorochemicals (PFAS)
Historically, commercial grease resistance in food wrapping was frequently achieved through per- and polyfluoroalkyl substances (PFAS)—so-called “forever chemicals” that impart severe oil repellency. However, landmark legislative bans across North America, the European Union, and Australasia have outlawed intentionally added PFAS in food contact materials due to bioaccumulation and toxicological hazards. This regulatory vacuum has triggered massive enterprise procurement demand for food grade PE coated paper sheets. PE extrusion functions as a purely mechanical, continuous polymeric barrier layer, requiring zero fluorinated additives while achieving superior grease resistance (Kit Test Rating 12/12) and unmatched water vapor retention.
Hermetic Barrier Defense
Continuous pinhole-free polyethylene coating creates an impermeable seal against high-temperature hot grease, organic acids, animal fats, and water vapor migration.
100% Non-Toxic & PFAS Free
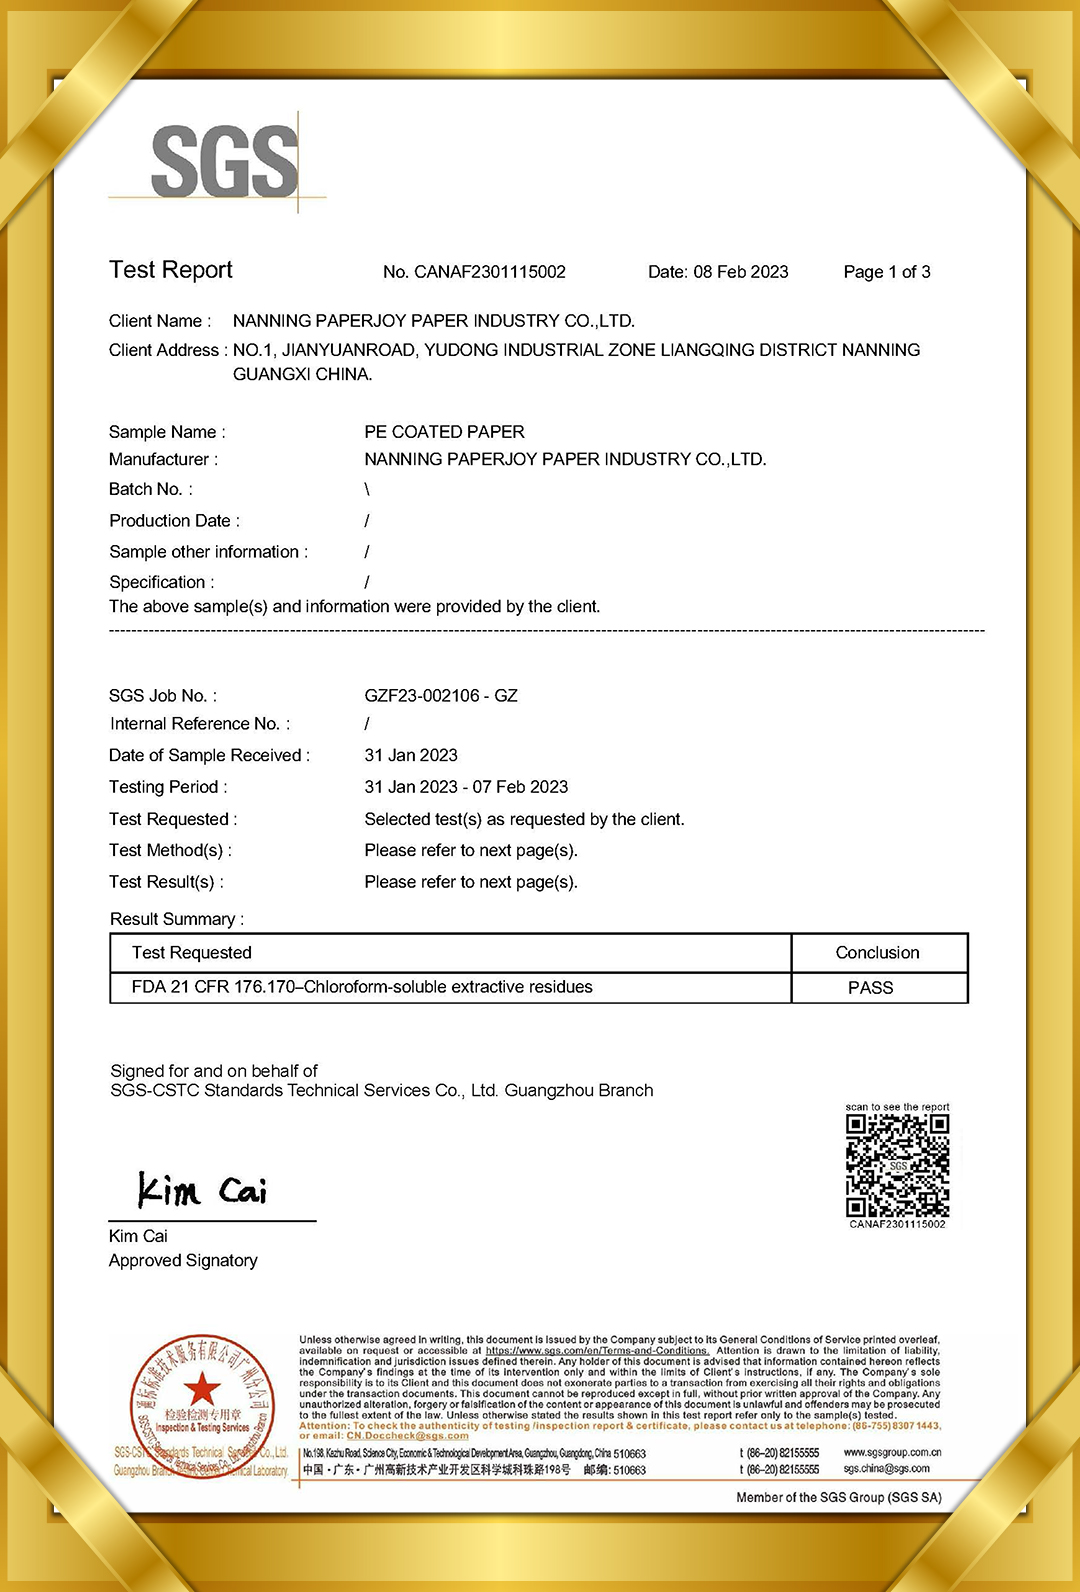
Synthesized without fluorochemicals, phthalates, or Bisphenol A (BPA), fully verified under strict FDA 21 CFR 176.170, REACH, and TPCH safety standards.
High-Yield Converting Pulp
Formulated with premium virgin wood pulp fibers that yield exceptional tensile strength, fold endurance, and tear resistance under automated sheet-fed packaging lines.
Deep Industrial Analysis: Food Service & Industrial Wrapping Scenarios
PE coated paper sheets are not universal commodities; their structural specifications must be dialed in according to thermodynamic, chemical, and physical packaging environments. The integration of single PE (1S) or double PE (2S) coating on base paper weights ranging from 35 gsm up to 400 gsm unlocks a vast spectrum of specialized commercial use cases:
| Application Sector | Base Paper Grammage | PE Coating Spec | Key Barrier & Functional Requirements |
|---|---|---|---|
| QSR Burger & Sandwich Wraps | 28 – 45 gsm Virgin Kraft / White Kraft | 10 – 15 gsm LDPE (Gloss/Matt) | High grease holdout (Kit 12), thermal vapor breathability, easy creasing without cracking. |
| Fried Chicken & Deli Liners | 40 – 65 gsm Food Grade MG Paper | 12 – 18 gsm LDPE | Complete oil proofing, high wet burst resistance, hot grease temperature tolerance (up to 100°C). |
| Fresh & Frozen Meat Interleaving | 50 – 90 gsm Bleached Kraft Paperboard | 15 – 20 gsm HDPE / LDPE Blend | Low-temperature anti-sticking release, blood and moisture containment, condensation barrier. |
| Bakery & Pastry Box Liners | 45 – 80 gsm Cupstock / Ivory Board | 10 – 14 gsm Single PE | Butter and shortening resistance, non-stick release properties, neutral aroma and odor index. |
| Formed Takeaway Tray & Clamshells | 190 – 350 gsm C1S Ivory / GCU Board | 15 – 25 gsm Single/Double PE | High flexural rigidity, deep-draw die cut score retention, ultrasonic & thermal heat sealability. |
1. Fast-Food & QSR High-Grease Sandwich Wrapping
In high-volume fast-food environments, burger wraps and taco wrappers must prevent molten animal fats and condiment sauces (mayonnaise, ketchup, mustard) from penetrating the exterior. A leak ruins brand impression and soils consumer clothing. Simultaneously, the wrapping substrate must allow controlled moisture vapor egress to prevent steaming the bun into a soggy texture. Engineered low-gsm virgin kraft laminated with 10–12 gsm LDPE delivers the exact micro-porosity and crease-retention required, ensuring crisp folds that remain intact during delivery transit.
2. Fresh & Frozen Protein Interleaving Sheets
In meatpacking plants and industrial butcher operations, sliced beef, poultry, and fish fillets require interleaving divider sheets. If paper fibers absorb moisture, they tear during peeling and contaminate food. PE coated paper sheets engineered with hydrophobic polymer formulations provide clean release at sub-zero blast-freezing temperatures (-20°C to -40°C), preventing inter-patty adhesion while locking in hydration and maintaining hygiene compliance.
3. Commercial Bakery Shortening & Sugar Glaze Protection
Pastries, donuts, croissants, and butter cakes present a dual challenge: high butterfat percentages combined with abrasive sugar crystallization. Uncoated papers wick lipids across their surface within minutes, causing unsightly dark spots. PE coated paper sheets provide a clean, non-absorptive release plane that preserves decorative icings and keeps outer display cartons crisp and structurally rigid.
Nanning Paperjoy Paper Industry Co., Ltd.
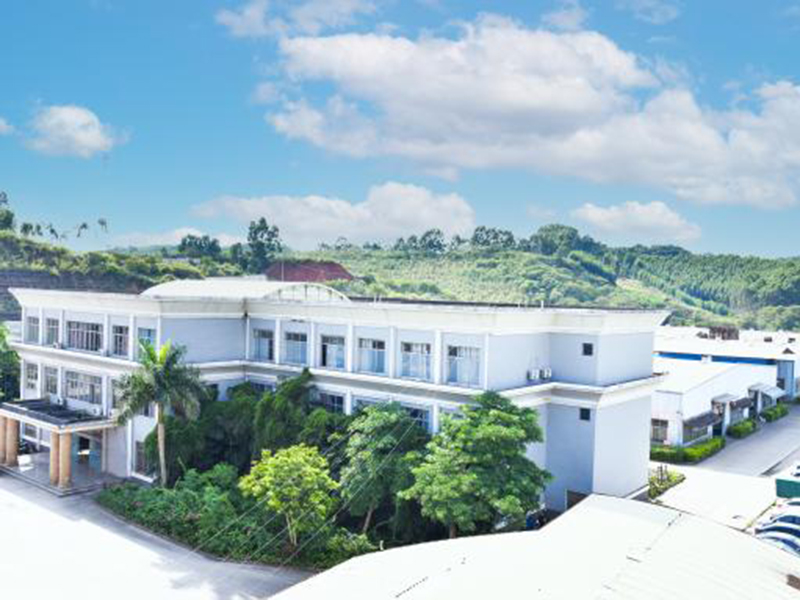
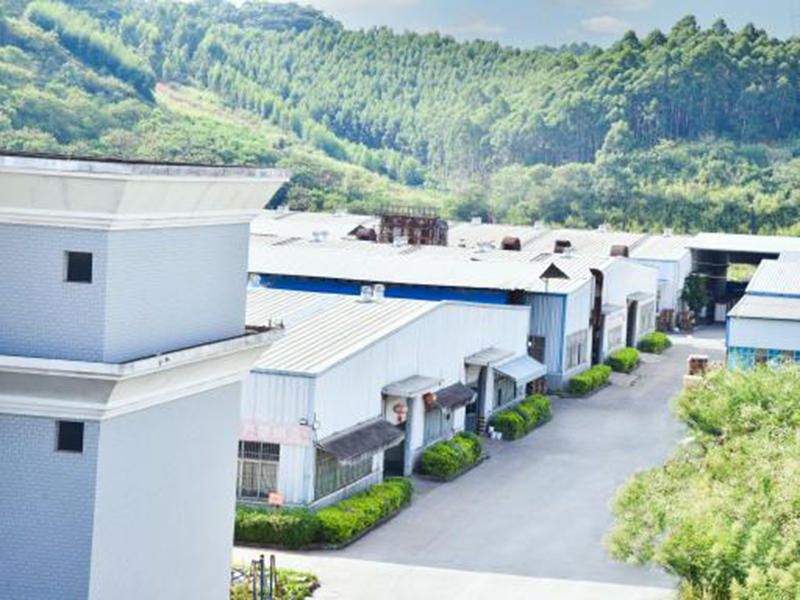
Nanning Paperjoy Paper Industry Co., Ltd. (“Paperjoy”) was established in 2006, with 200 employees and covers over 15000㎡. Paperjoy is a professional manufacturer of raw materials for paper cup and packaging box, especially the PE coated paper roll, paper cup fan, cup bottom reel and C1S ivory board. We are specializing in producing different kinds of PE coated paper raw materials. The annual production capacity is 60,000 tons.
Our factory ideally located at the heart of Nanning city economic zone, which is very near to Qinzhou port, Beibu Gulf at the South of China. Our 200 well-trained and technically sound staff are motivated towards accomplish a common goal of customer satisfaction and devoted to achieve “Honesty, Mutual benefit, Win-Win cooperation” business philosophy.
Corporate Development Path
Set up in 2006, engaged in paper cup paper PE coating industry. Paperjoy, means good luck and happiness.
Developing B2B overseas market. Expanded international footprint, targeting Asia, Africa, Europe, North America, etc.
Commissioned brand-new high-speed extrusion coating lines; production capacity doubled to 60,000 tons/year.
2022-Our products have been used in more than 2,000 converter factories and exported to over 60 countries since 2006.
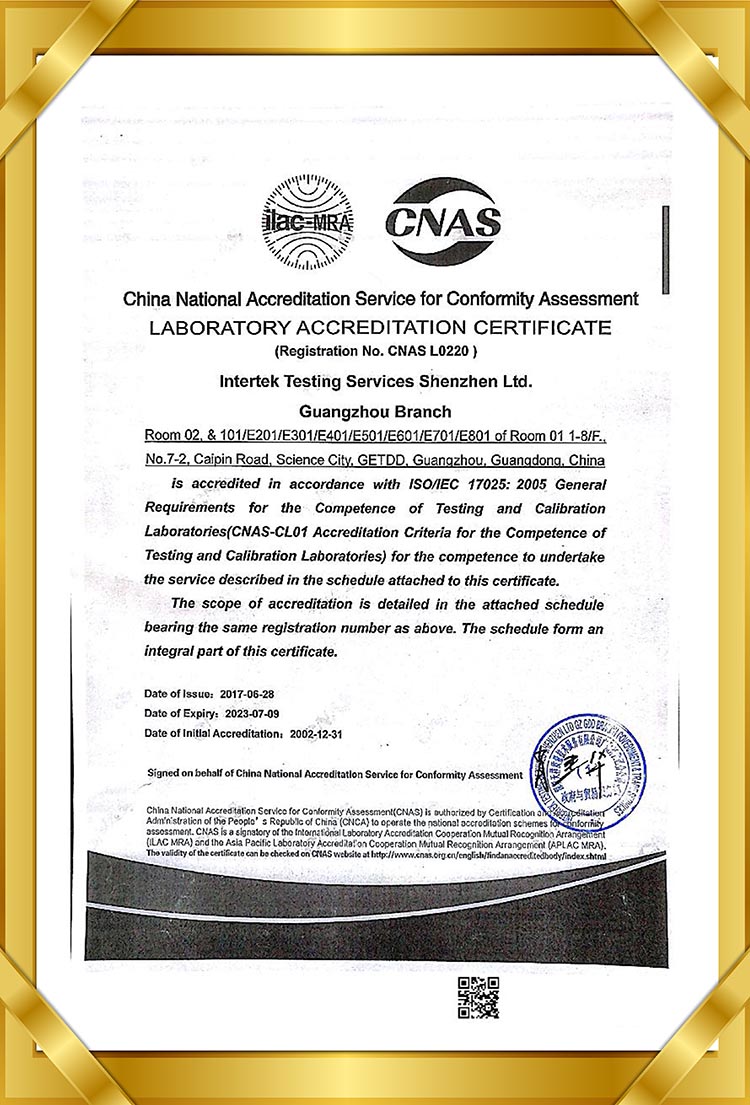
International Certification System
PaperJoy’s quality assurance system applies to all of our processes and products. Our quality management program ensures that every product delivered meets or exceeds the quality standards required by our global customers.
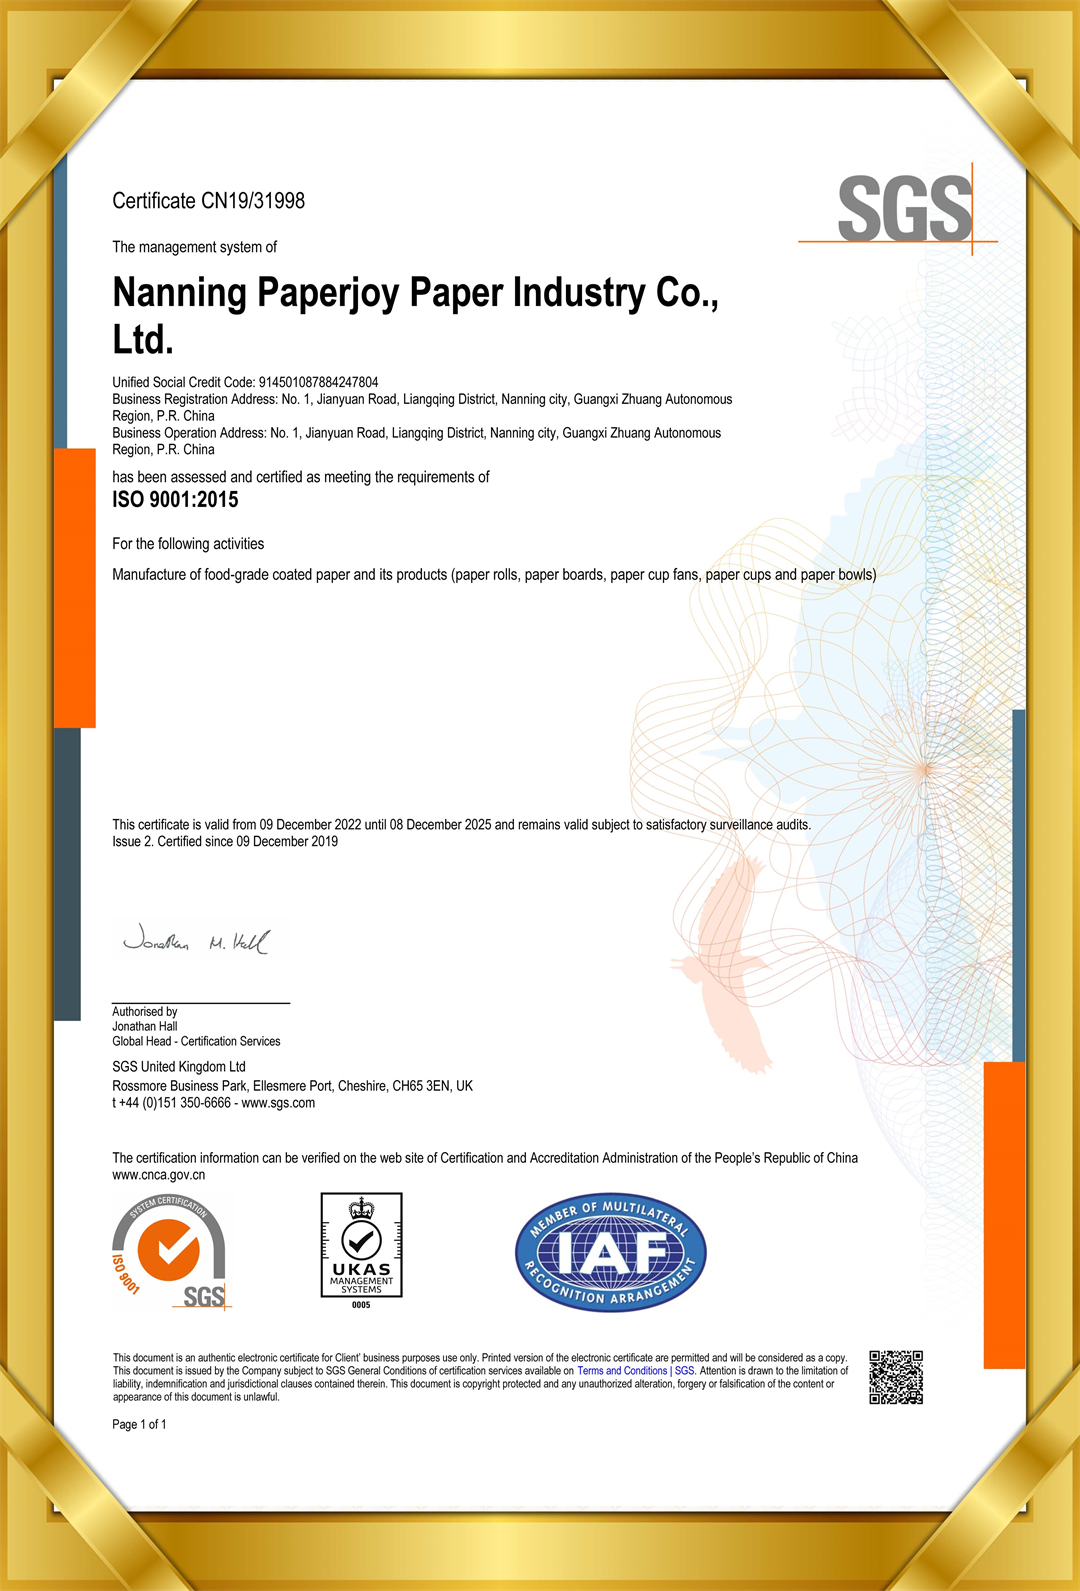
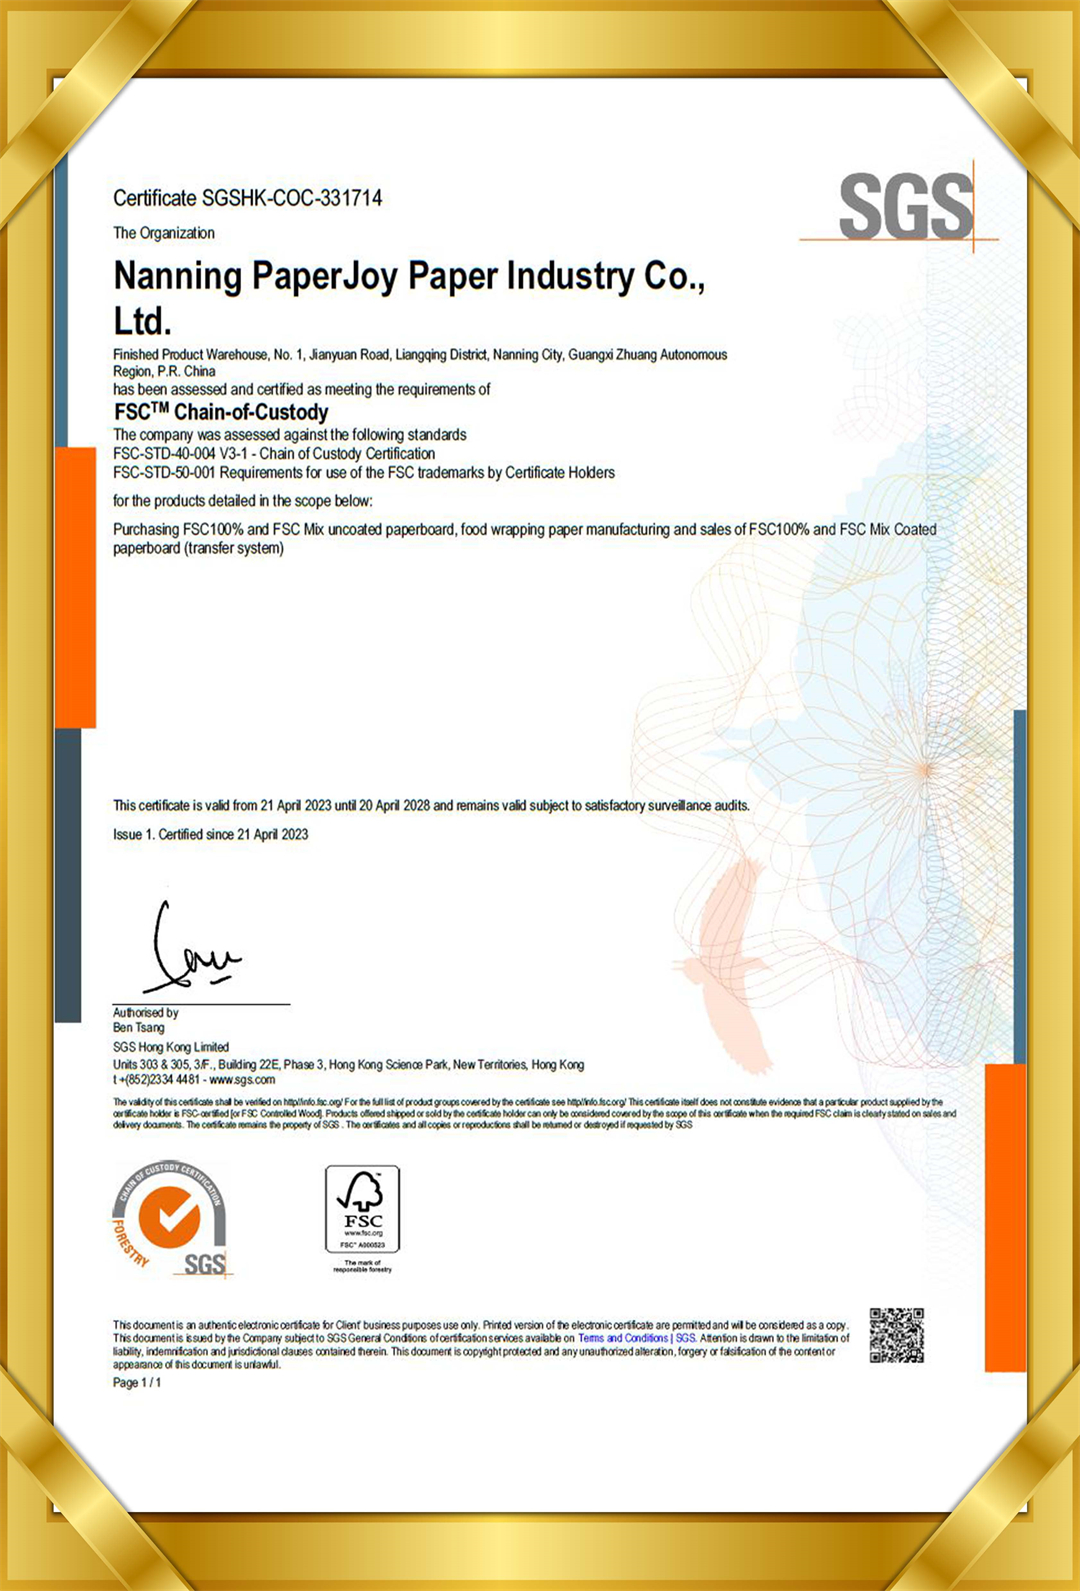
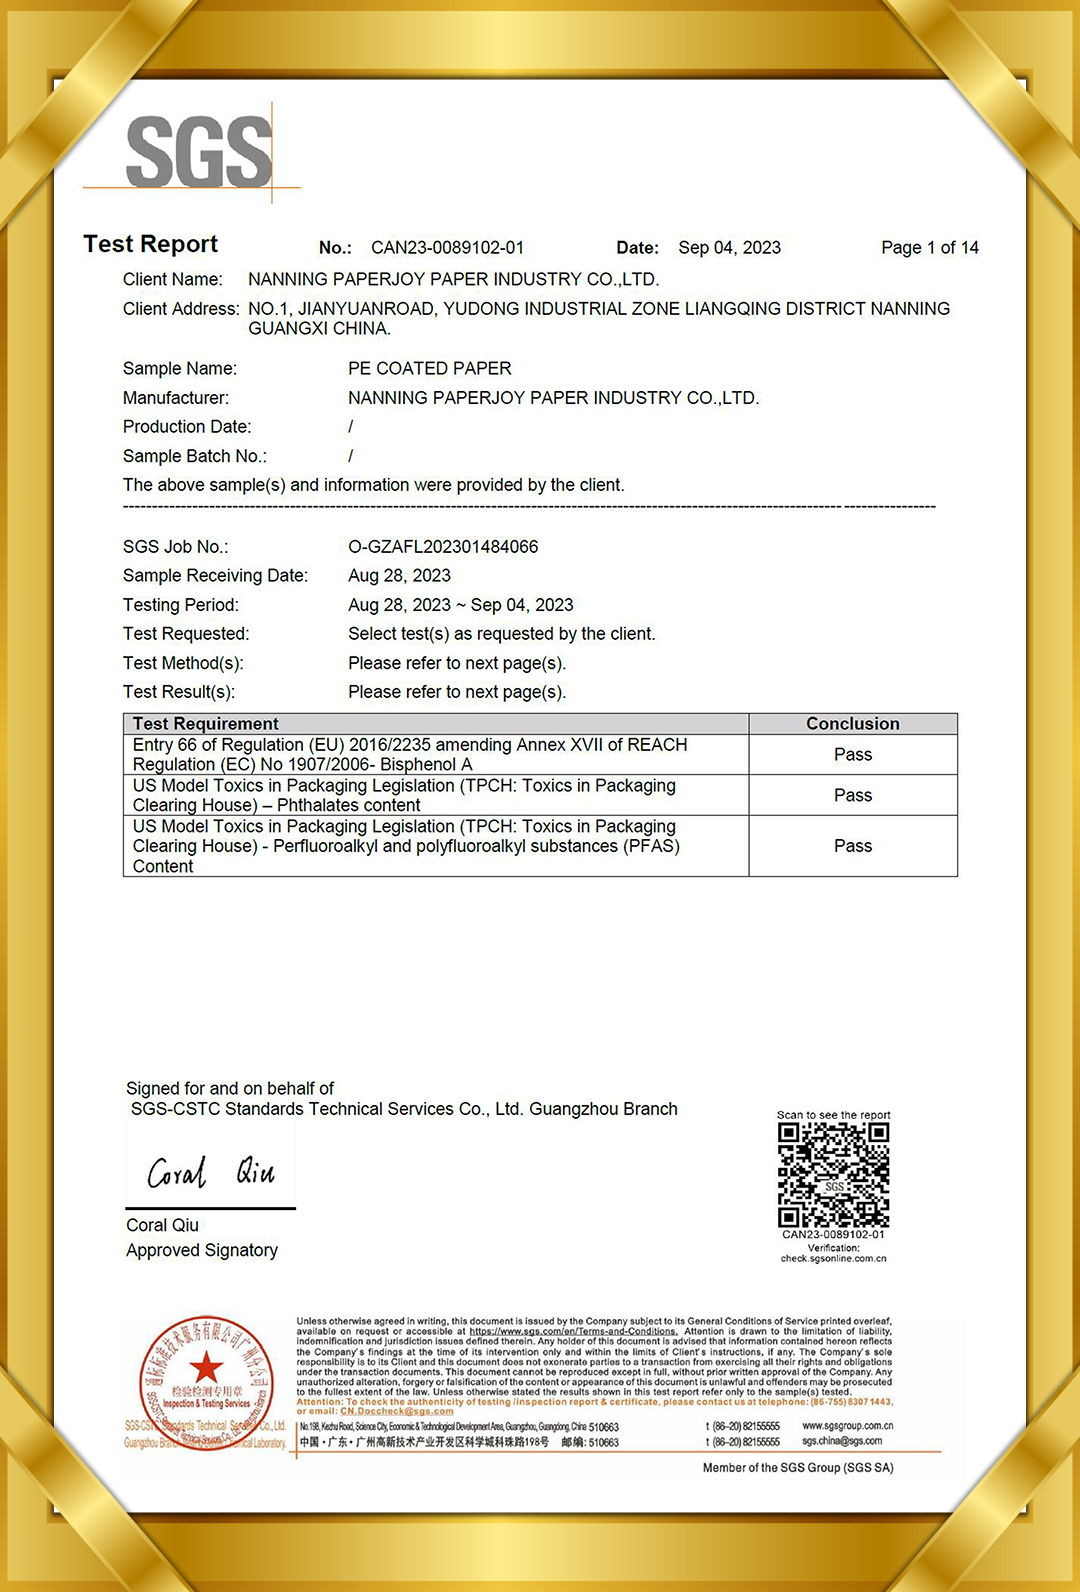
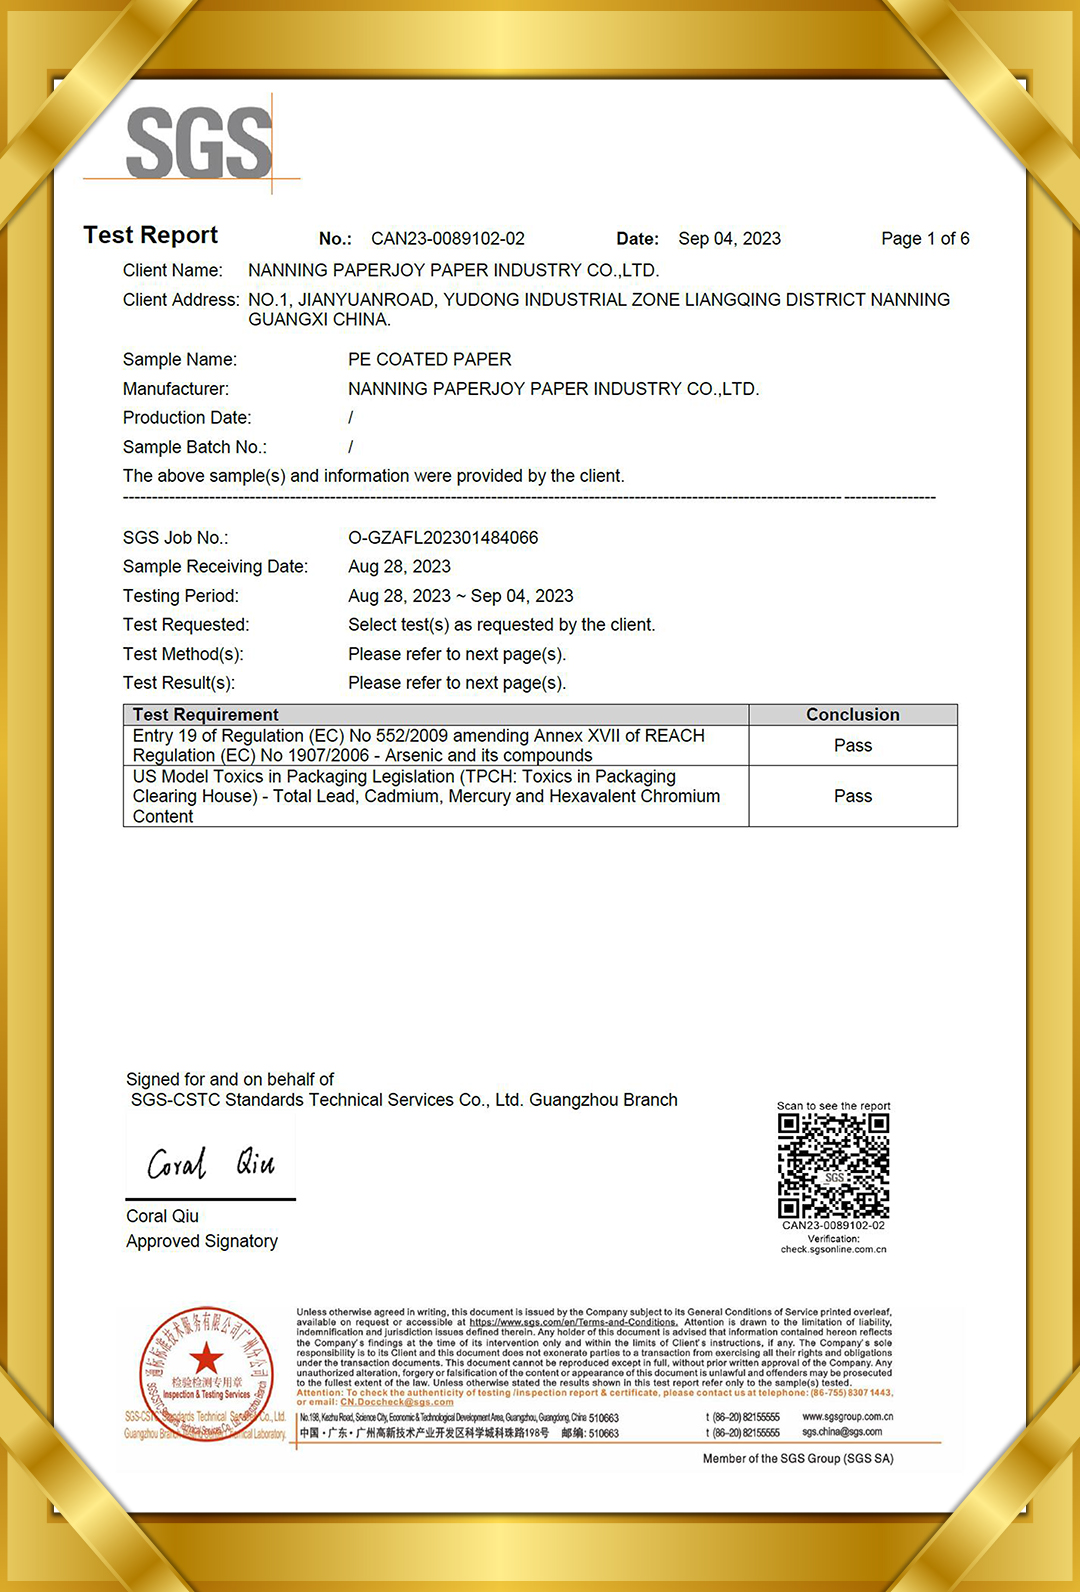
Core Supply Chain & Processing Advantages
Paperjoy factory located very near to several famous paper mill brands. Stora Enso, Sunpaper, APP, Yibin paper, and FiveStar paper are our regular base paper suppliers.
We have built a comprehensive strategic partnership with SunPaper Groups; reliable base paper consistency, high stiffness, and steady delivery schedules are permanently guaranteed.
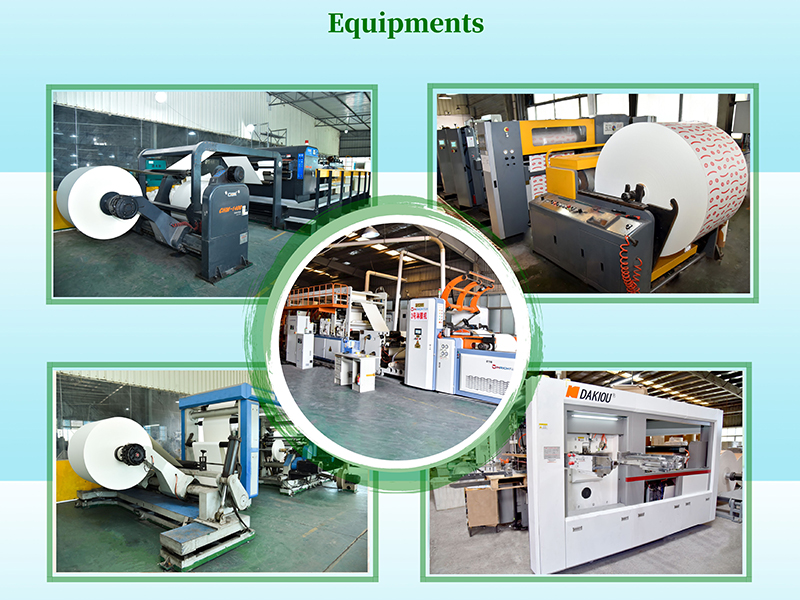
With complete devices and equipment, we are capable of providing one-stop service of PE coating, flexo printing, die cutting, scrap cleaning, and precision rotary slitting.
Corporate Vision & Strategic Mission
Our Vision
Bring health & environmental protection to food packaging systems across the entire world.
Mission 1
To be the premier global supplier of paper cup raw materials, food packaging sheets, and custom barrier paperboards.
Mission 2
To be an empowering, rewarding, and happy home for all Paperjoy team members and stakeholders.
PaperJoy Global Service Matrix
Customized Products
We provide tailored paperboard raw material products configured to exact target caliper, PE thickness, width, sheet dimension, and performance parameters.
Diverse Product Lineup
We offer diverse raw materials including PE coated Paper Rolls, PE Coated Paper Sheet, Paper Cup Fans, C1S Ivory Board, and Kraft Paper Roll to satisfy varied converting requirements.
Free Quotations & Samples
We provide free sample swatches and rapid quotes so partners can inspect grammage consistency, sealability, and barrier coatings firsthand before placing volume orders.
Fast Delivery Execution
Backed by lean workflow management, close proximity to deep-water shipping hubs, and raw inventory buffer stocks, we ensure prompt manufacturing and quick cargo dispatch.
Technical Consulting
Our packaging engineering team provides specialized consultations spanning base paper grammage selection, PE density factors, die-cutting dynamics, and flexo ink compatibility.
Professional Technical Support
Dedicated after-sales teams deliver comprehensive technical follow-up, guiding container forming line calibration, cup bottom sealing adjustments, and waste reduction.
Advanced Machinery & Converting Equipment
High-precision laminating machines producing PE coated paper rolls with uniform corona treatment and micro-gap thickness control.
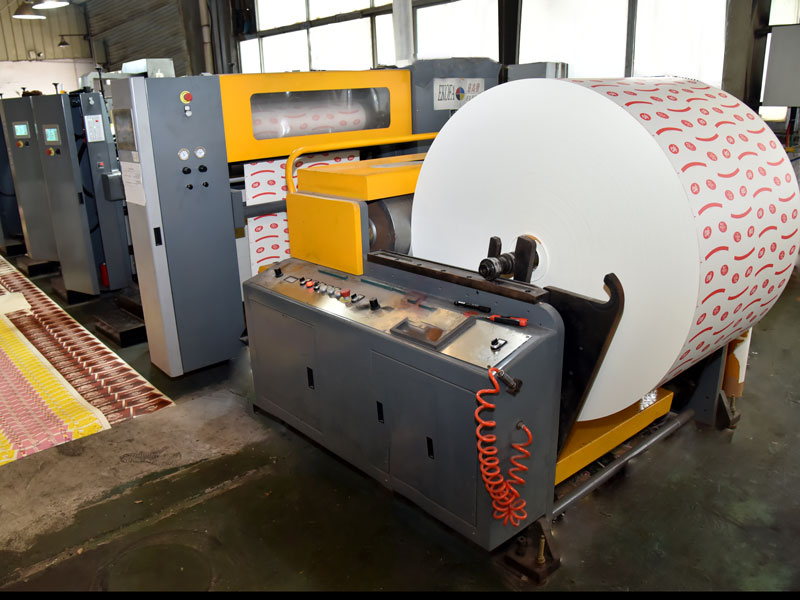
Six-color flexographic printing machines for roll-fed paper cup fans using water-based, odorless food grade inks.
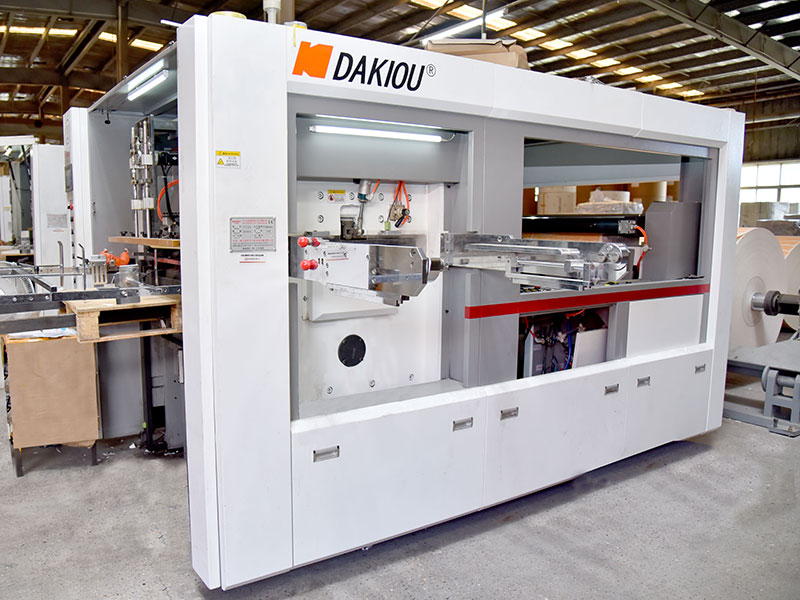
Precision flatbed and rotary die-cutters running at high throughput exceeding 280 strokes/minute with razor-sharp edge precision.
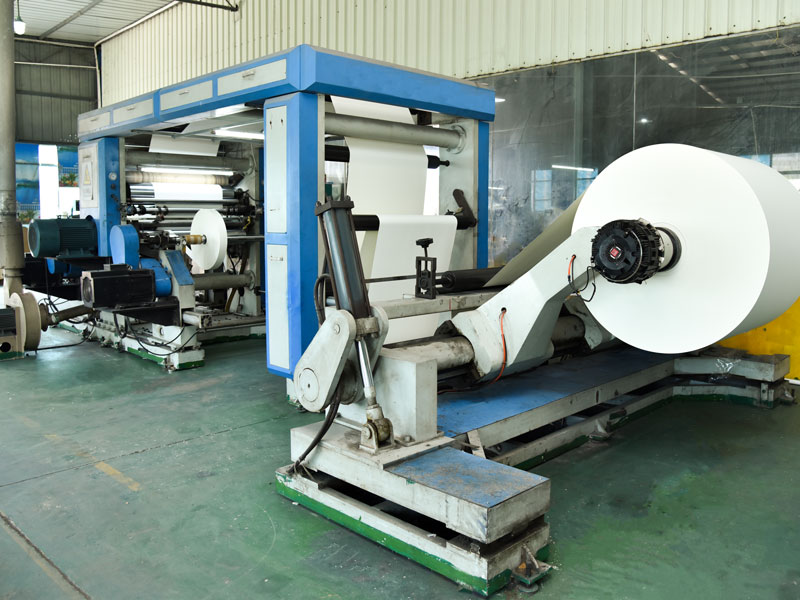
Precision slitting units producing tight, cleanly edged paper cup bottom rolls with consistent winding tension.
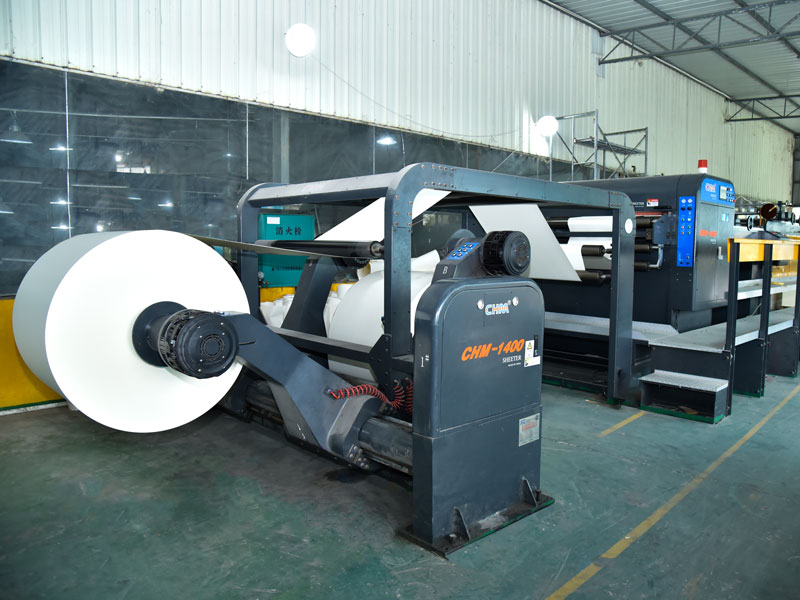
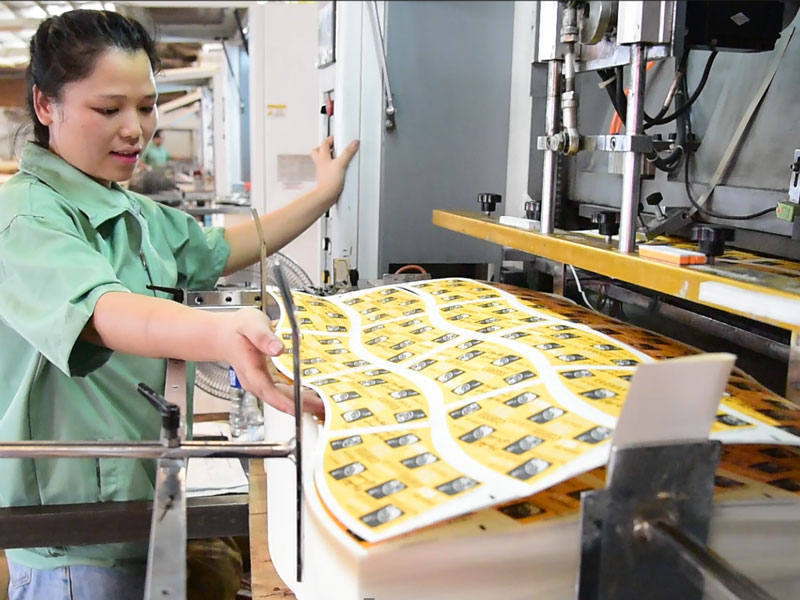
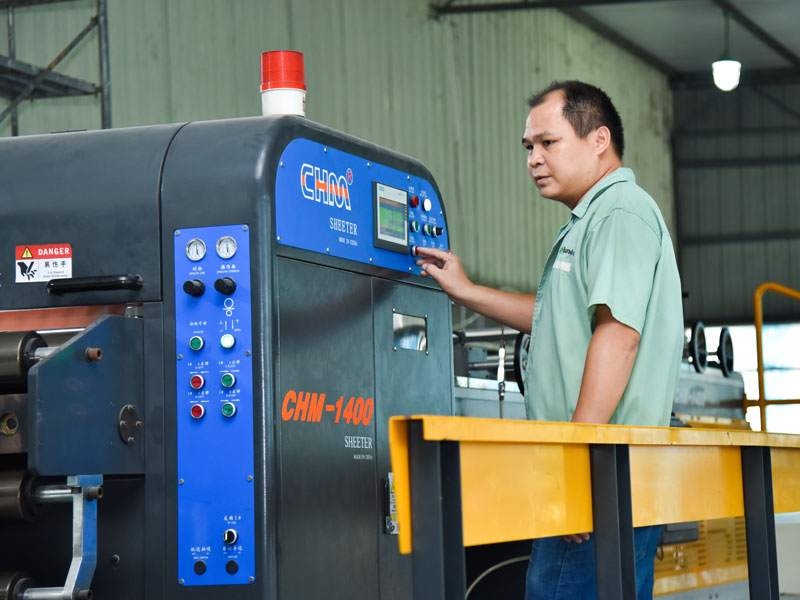
Dedicated rotary sheeter designed for square, burr-free conversion of PE coated paper sheets in custom client dimensions.
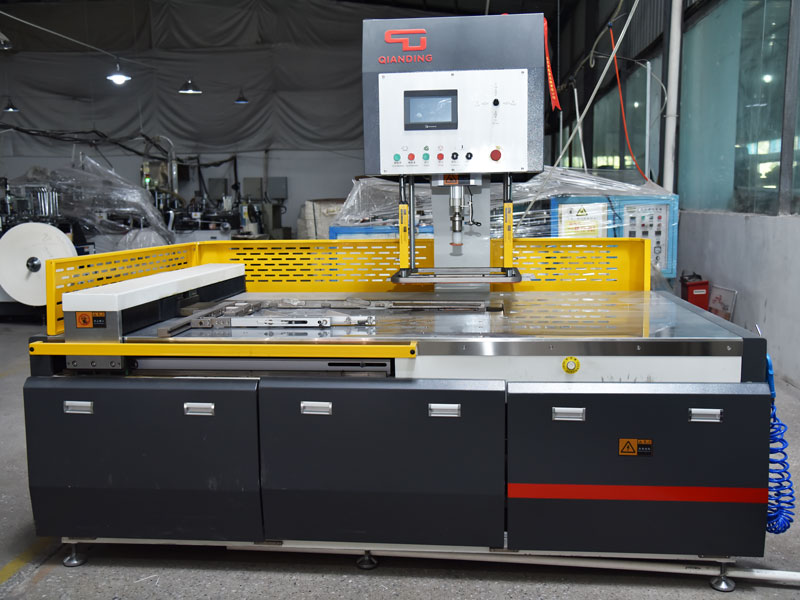
Automated stripping machines clearing trim scrap from converted blanks to ensure smooth, jam-free loading in cup machines.
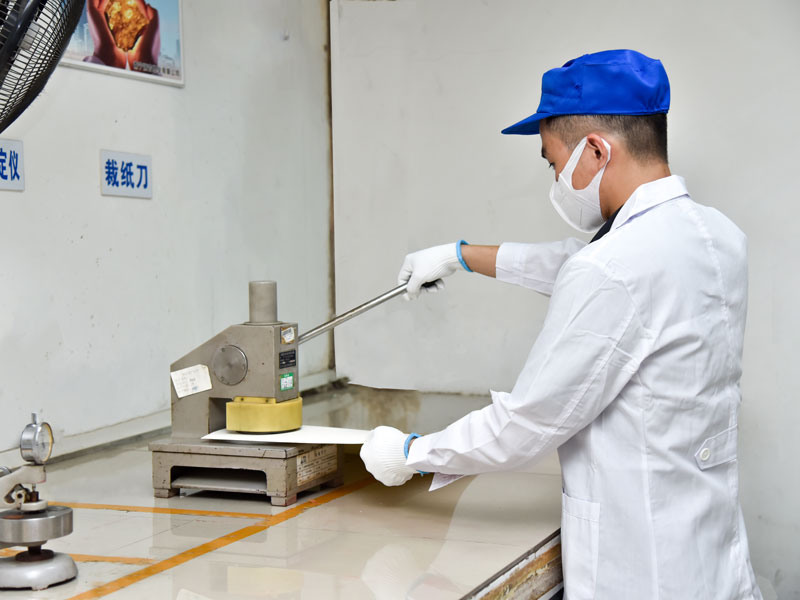
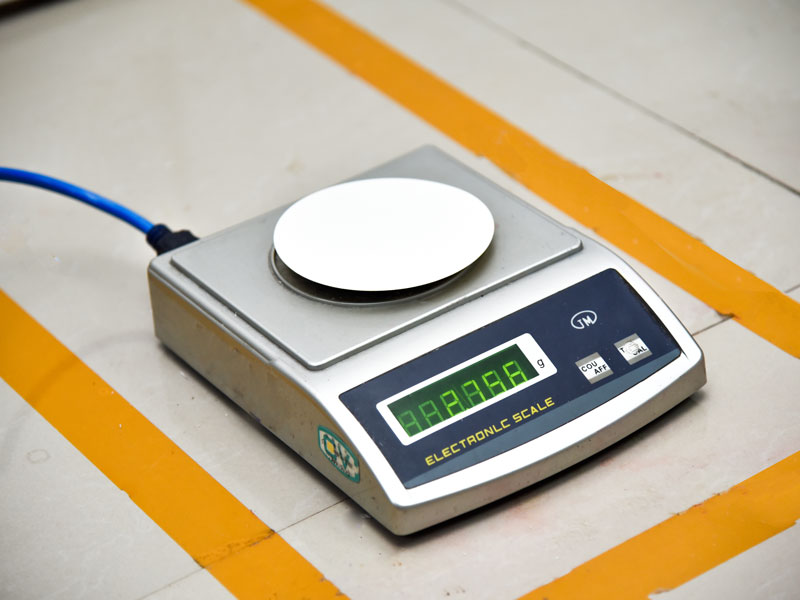
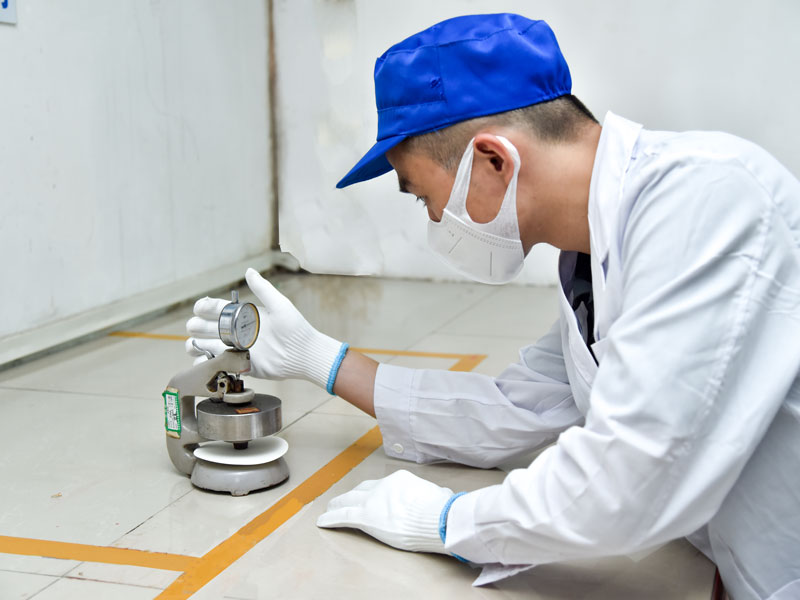
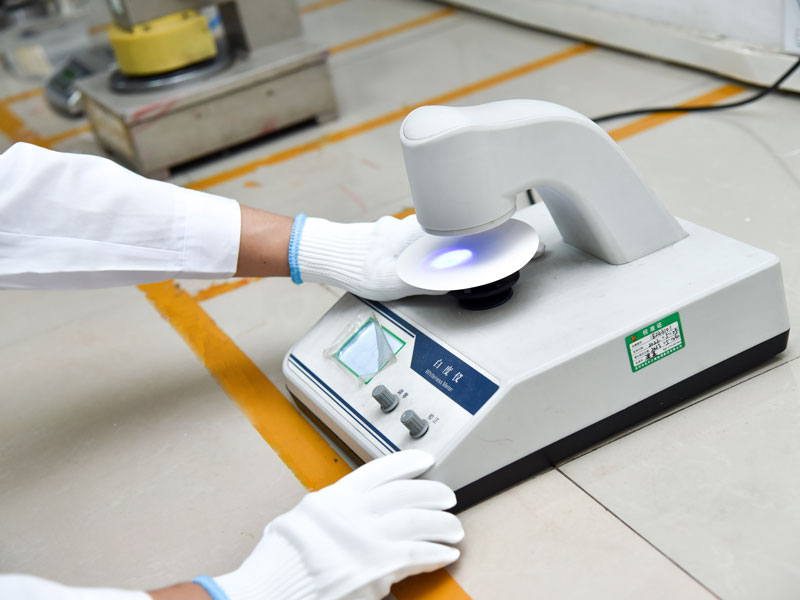
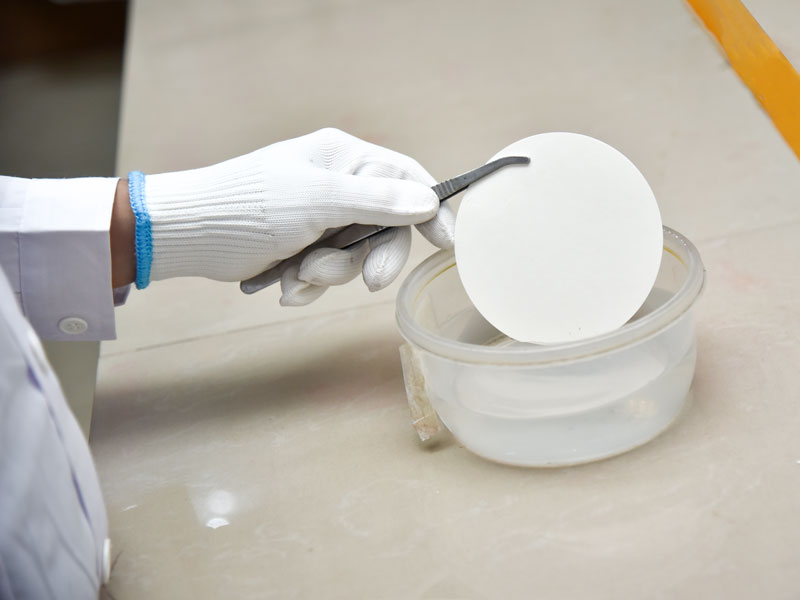
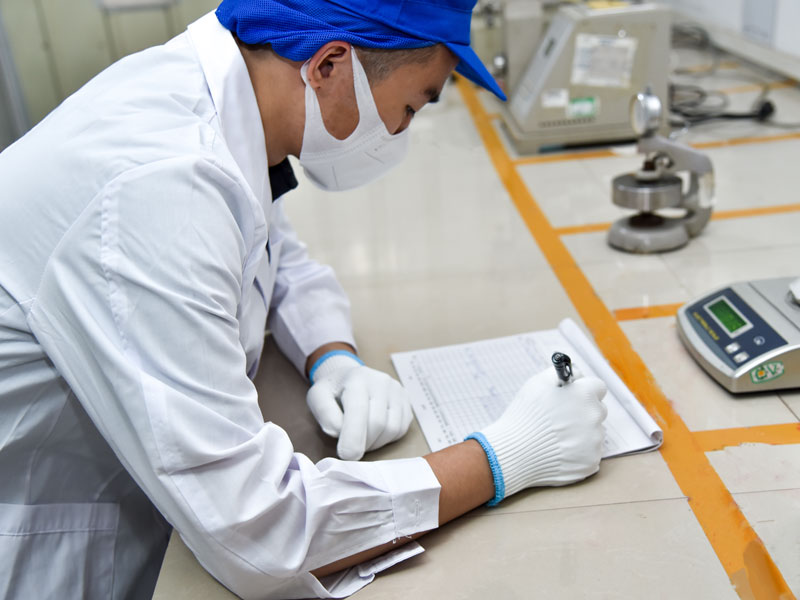
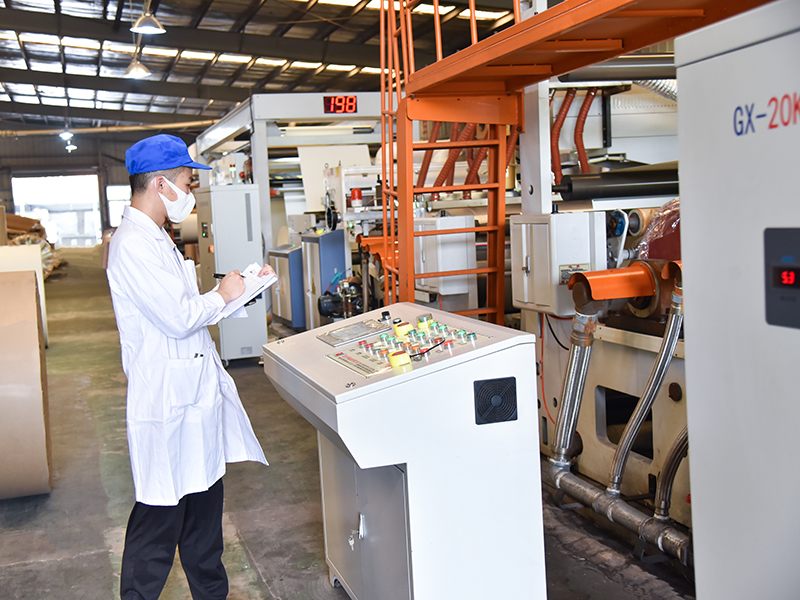
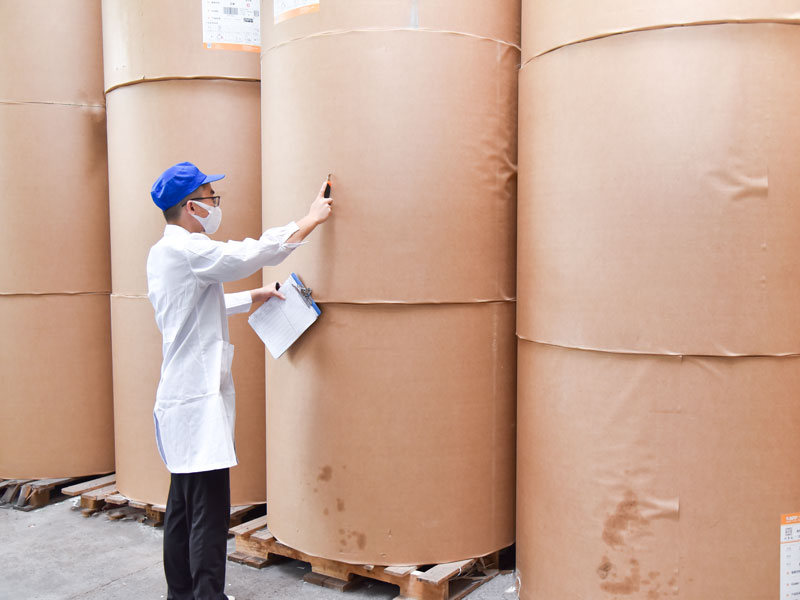
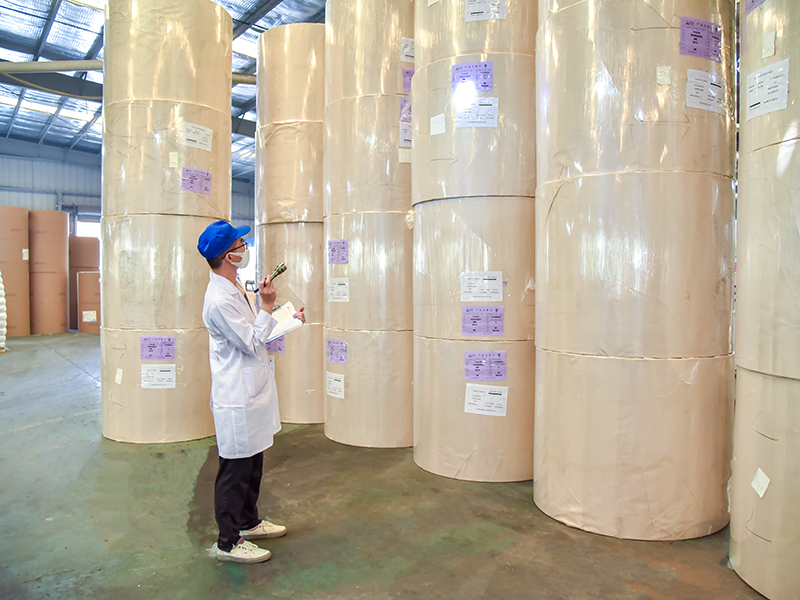
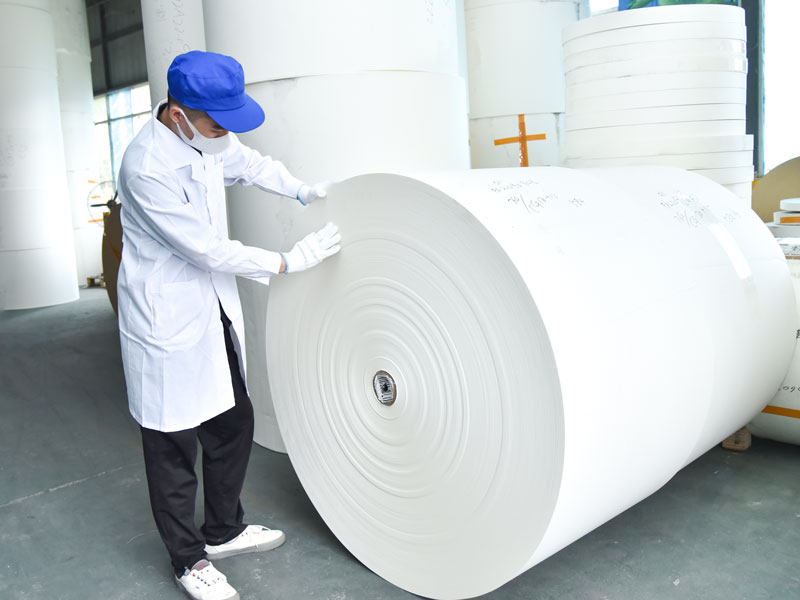
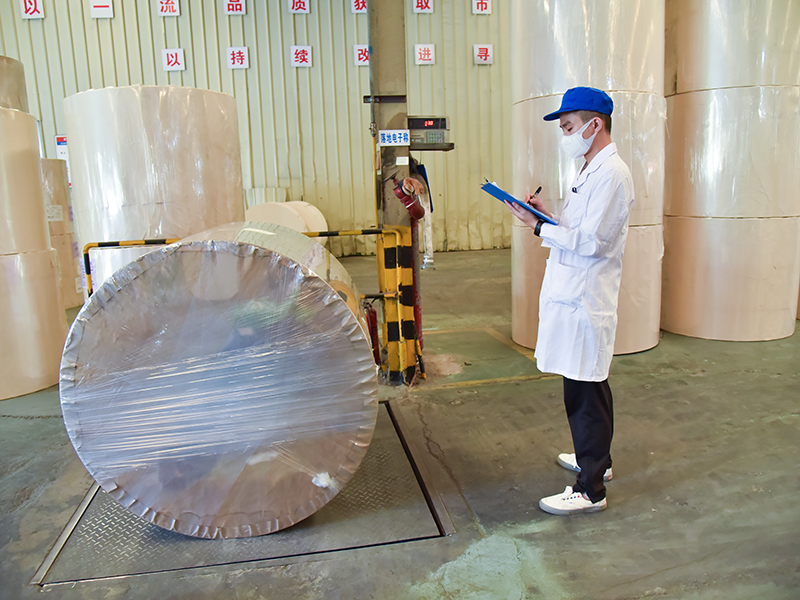
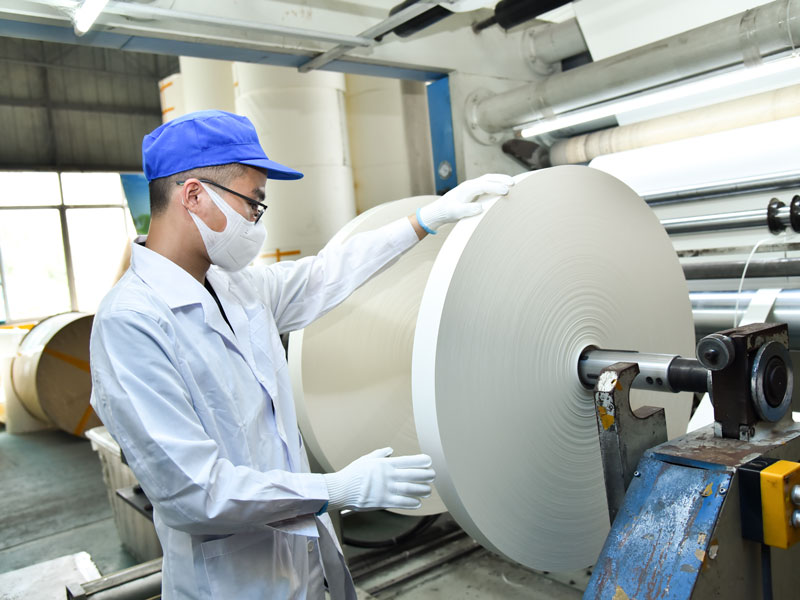
Comprehensive Quality Inspection & Testing Center
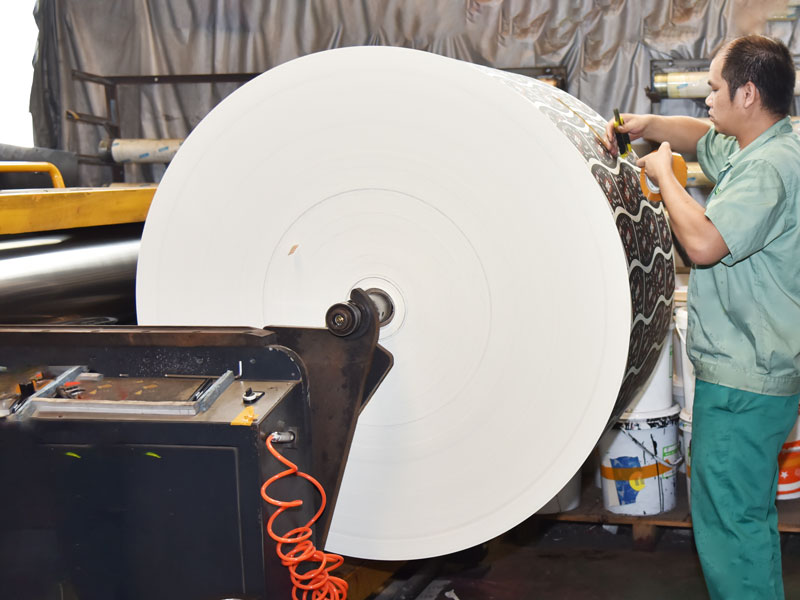
From raw virgin wood pulp arrival to final skid packaging, every batch undergoes mechanical, thermal, and barrier testing to guarantee performance on high-speed converting machinery.
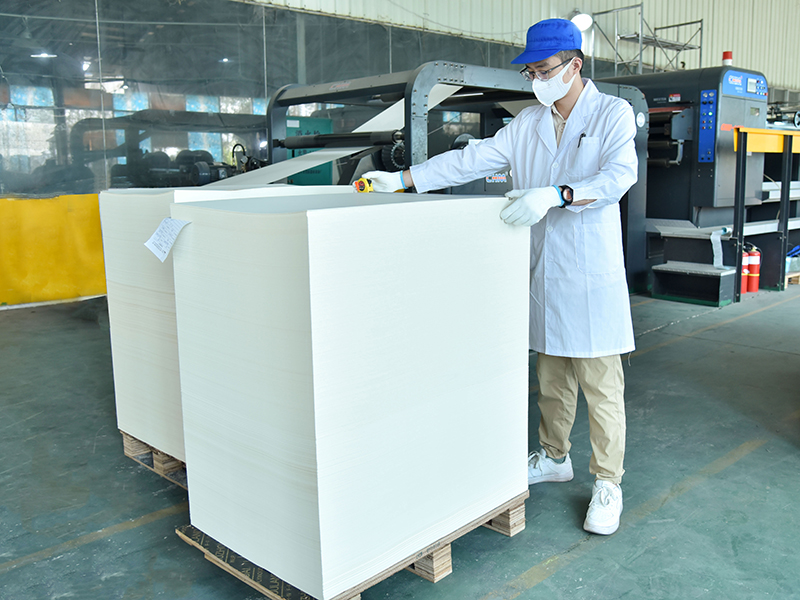
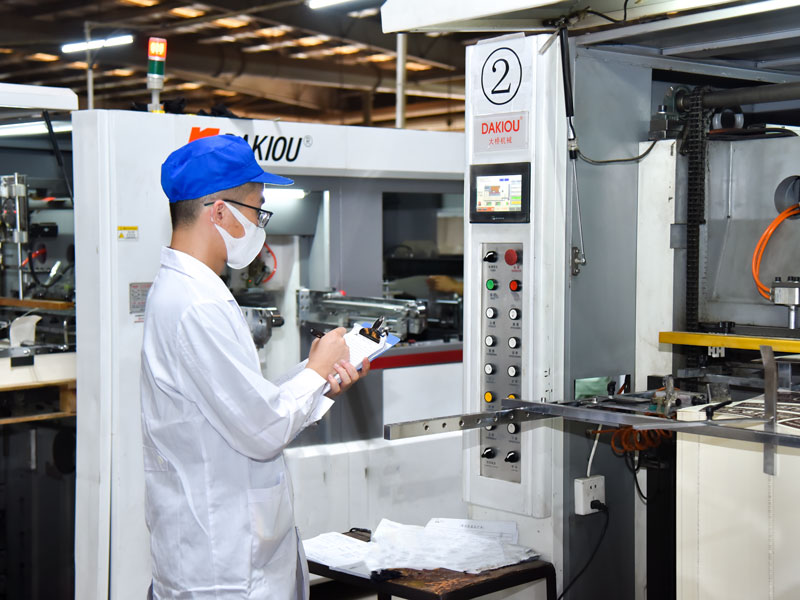
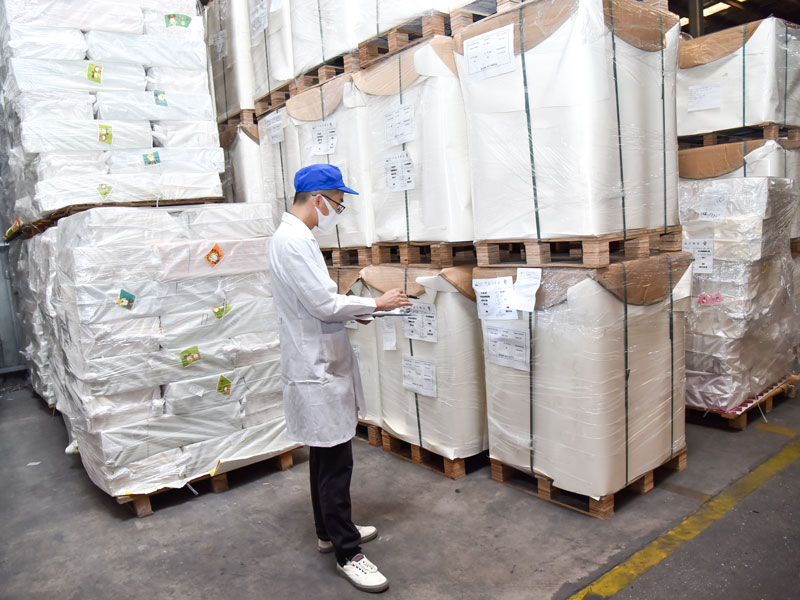
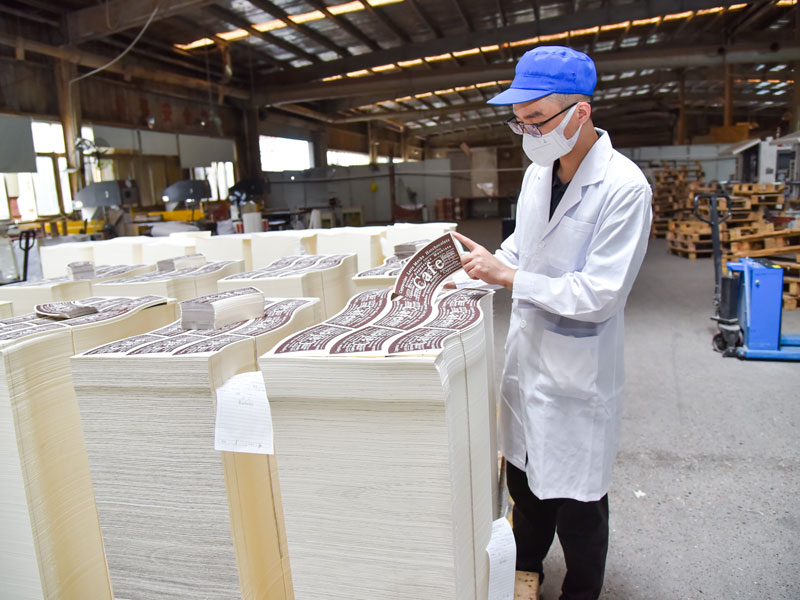
Factory Operational Overview
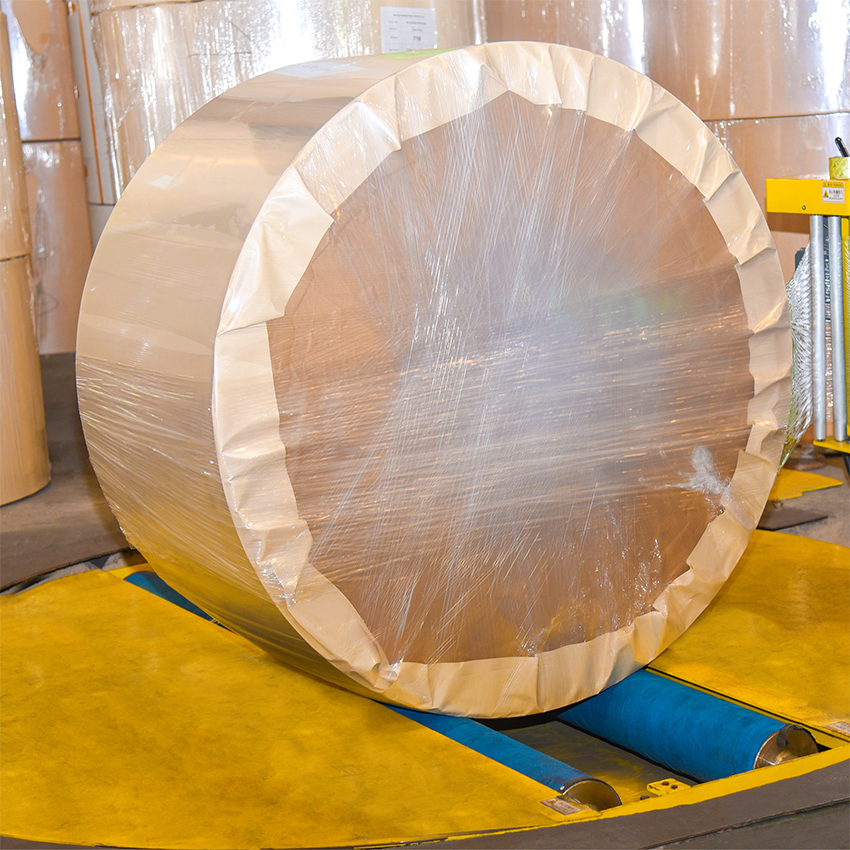
Strict Quality Control Processes
• Raw material inspection: Select virgin wood pulp and pure food-grade PE resin.
• Real-time monitoring across extrusion coating, flexo printing, and die-cutting.
• Batch retention sampling and full digital barcoding for entire lifecycle traceability.
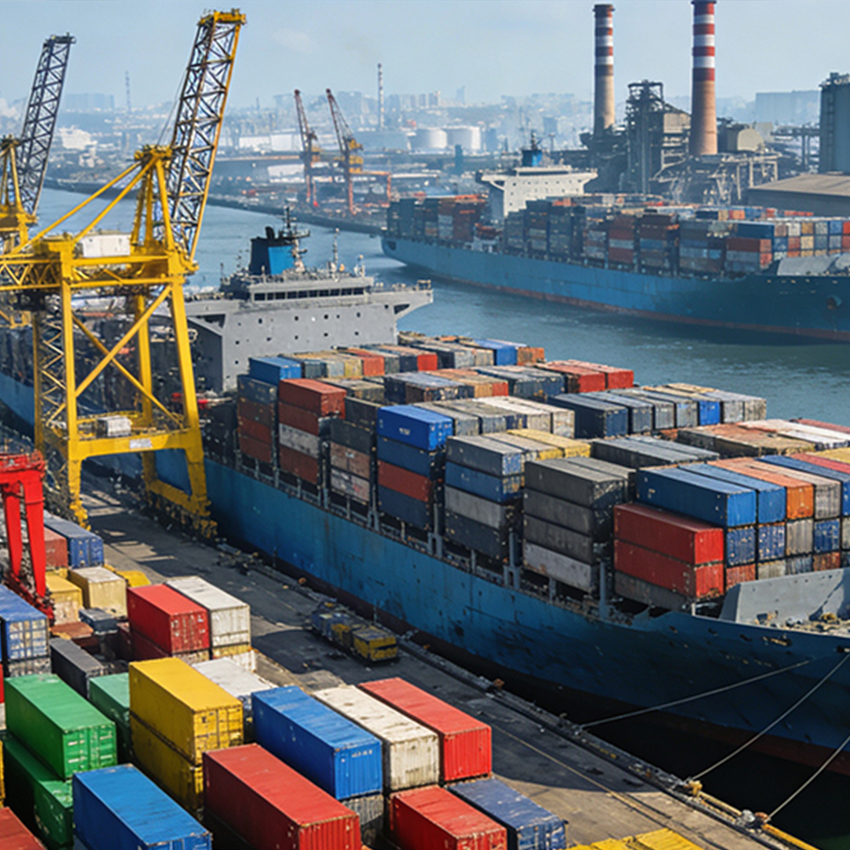
Advanced Production & Supply Capacity
• Multiple automatic extrusion lines delivering 60,000 tons annual throughput.
• 15,000 ㎡ clean workshop ensuring continuous raw paper roll storage buffer.
• Expedited manufacturing: Standard and custom orders fulfilled in 7-15 business days.
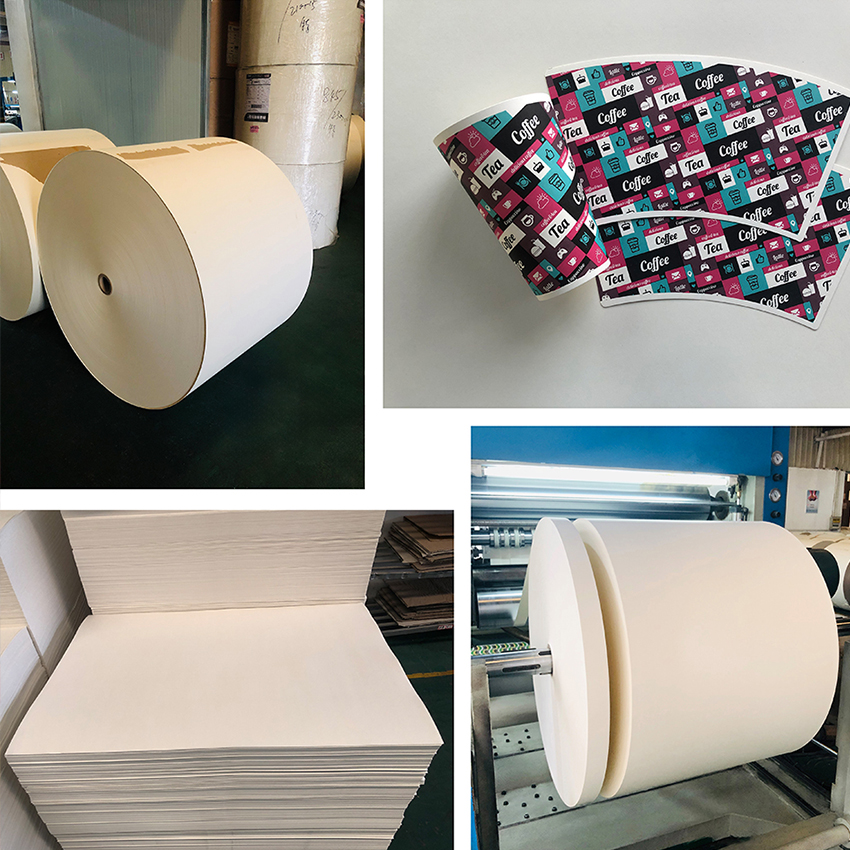
Tailored Engineering Options
• Substrate grammages ranging from 150g up to 400g to cover diverse container designs.
• Single/Double PE coating (10-30 gsm) in glossy or matte finishes.
• High-definition printing up to 6 colors with odorless water-based formulations.
Sustainable & Responsible Practices
• 100% sustainably managed forest pulp certified under FSC chain-of-custody.
• Food contact coatings certified non-toxic under FDA, REACH, and TPCH regulations.
• Low carbon footprint production systems featuring thermal recuperation oxidizers.
Factory Tour & Workflow Overview
Office Environment & Commercial Hub
Personnel Standard Operating Procedures (SOP)
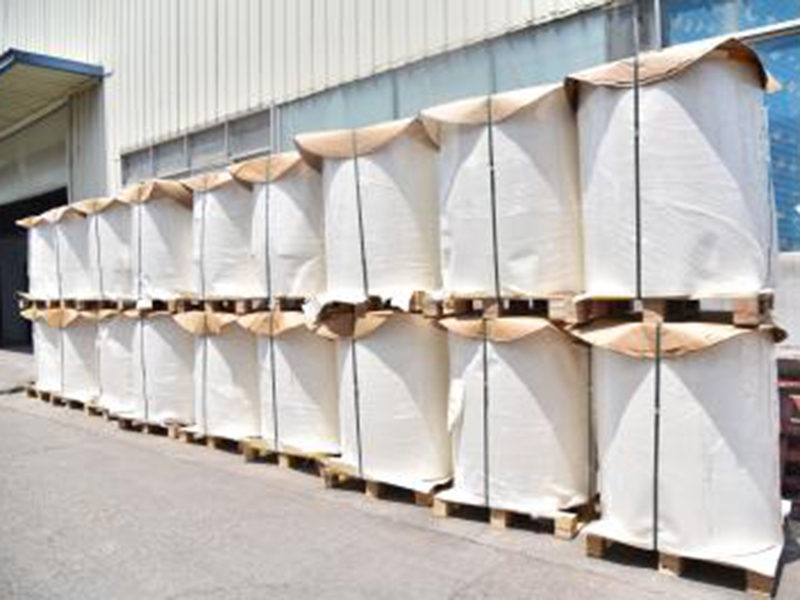
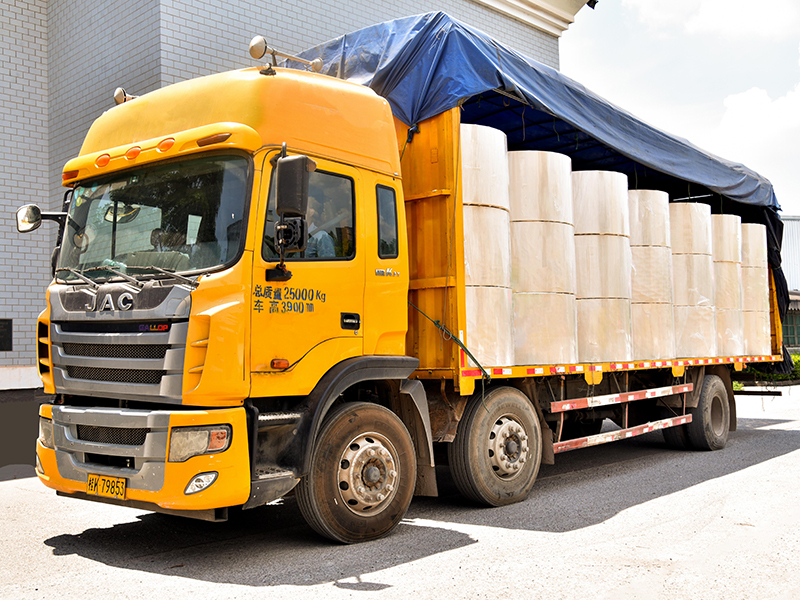
Export Packaging & Logistics Execution
Industry Recognition & Corporate Honors
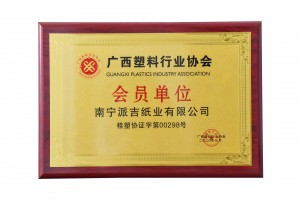
Plastics Association Member Unit
Official enterprise member adhering to industry coating purity and technical processing standards.
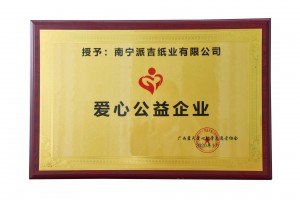
Charitable Enterprise
Recognized corporate social responsibility contributor dedicated to community welfare and employee wellbeing.
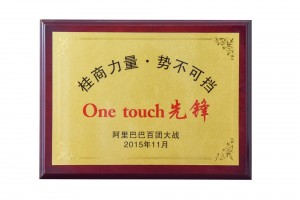
Alibaba Verified Gold Partner
Independently audited manufacturing facility verifying financial standing, export capability, and production scale.
All Food Grade PE Coated Substrates & Converted Materials
Browse our full selection of virgin paperboard reels, custom-cut wrapping sheets, and precision die-cut cup fans manufactured for global converters.
Get Free Samples and Customized Technical Quotations
Your Reliable Global Partner for High-Quality Professional Paper Cup Raw Materials Supplier and Manufacturer & Professional Solutions.