High-Performance Paper Cup Raw Materials
Direct factory supply of virgin wood pulp cupstock paperboard and precision-laminated PE coated rolls for versatile commercial food packaging conversions.
The Global Evolution of Paper Cup Raw Material For Food Packaging Use
The global transition away from single-use plastics has propelled paper cup raw material for food packaging use to the forefront of modern sustainable packaging engineering. Driven by stringent environmental regulations across Europe, North America, and Asia-Pacific, quick-service restaurant (QSR) chains, specialty beverage corporations, and ready-to-eat food manufacturers are massively replacing synthetic polymers with renewable, high-performance cellulose fiber substrates.
Modern food packaging demands more than just basic containment; it requires sophisticated functional barrier properties, thermo-mechanical endurance, impeccable hygienic safety, and compatibility with high-speed automated forming machines. The base substrate—commonly referred to as cupstock board—is paired with advanced lamination technologies like Single Polyethylene (1PE), Double Polyethylene (2PE), Polybutylene Succinate (PBS), or water-based dispersion barriers to withstand hot liquids, freezing temperatures, grease, and acidic condiments without structural deformation.
Technical Milestone: High-bulk cupstock paper achieves a 15% reduction in basis weight while maintaining identical tensile strength, edge-wicking resistance, and cup stiffness, significantly optimizing global freight costs and carbon footprint.
Key Drivers Accelerating Paper Cup Raw Material Demand:
- Booming On-the-Go Beverage Culture: Rapid proliferation of specialty coffee shops, bubble tea franchises, and iced beverage outlets globally requiring millions of leak-free, custom-printed paper cups daily.
- Rise of Prepared & Instant Food Sectors: Expanded application of paperboard packaging in instant noodle cups, oatmeal bowls, microwavable hot soup tubs, and fried chicken buckets.
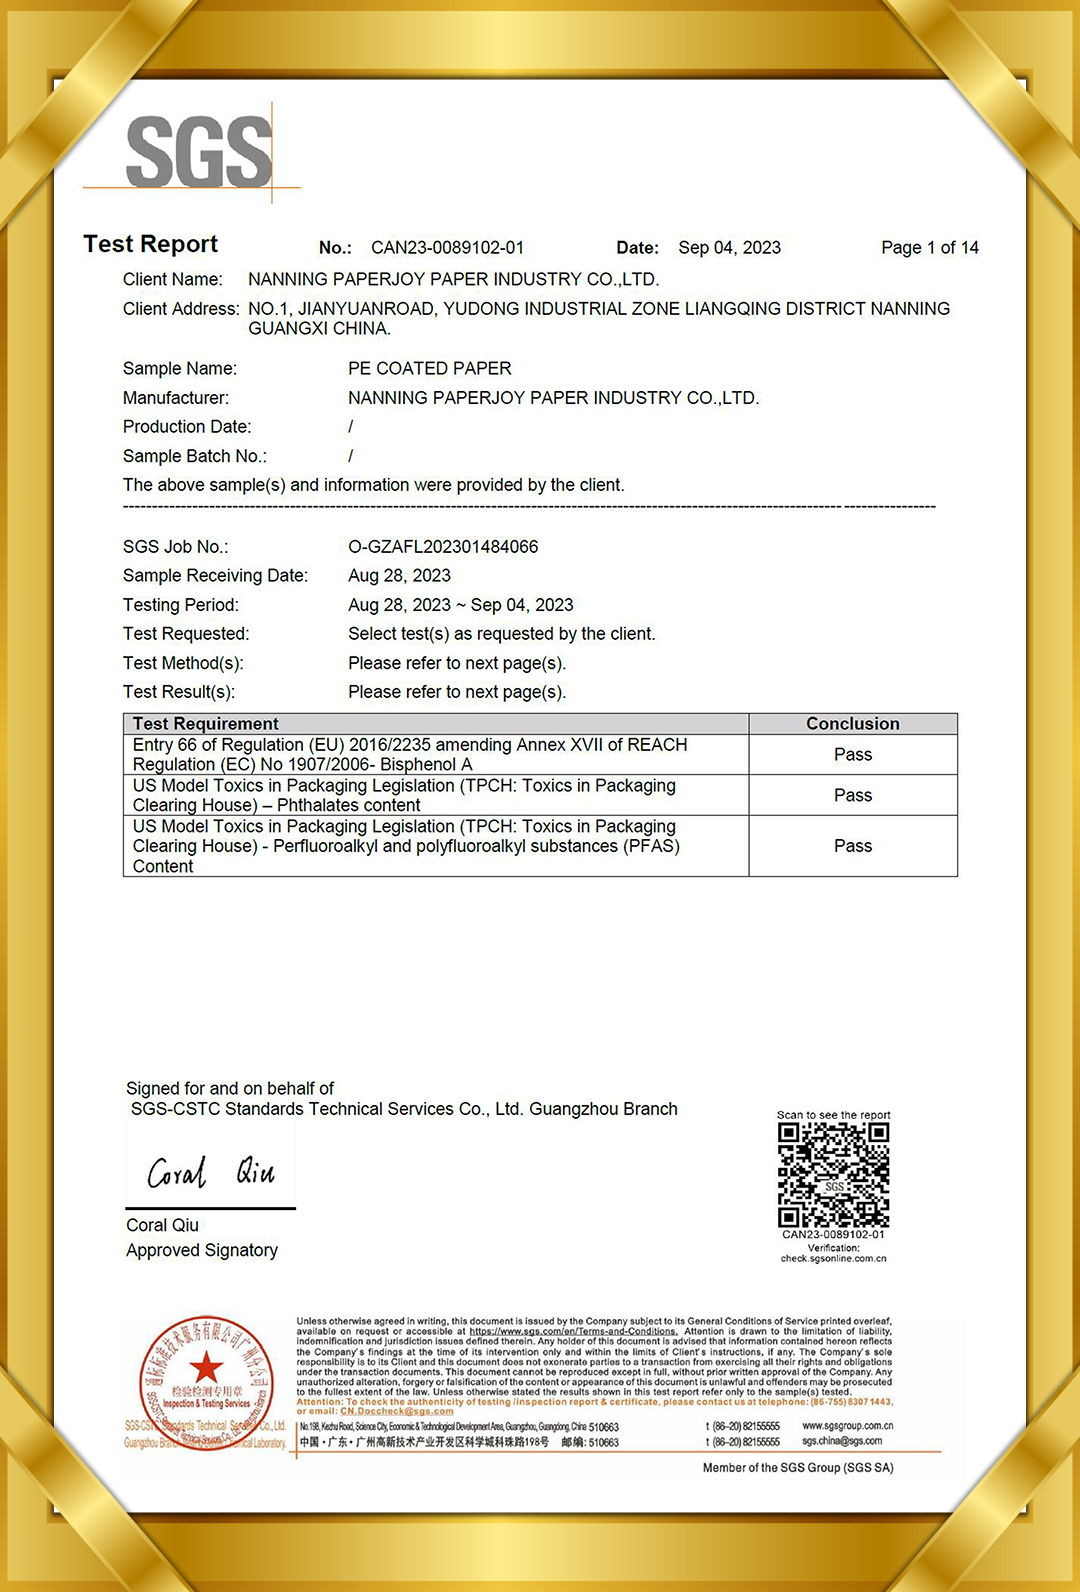
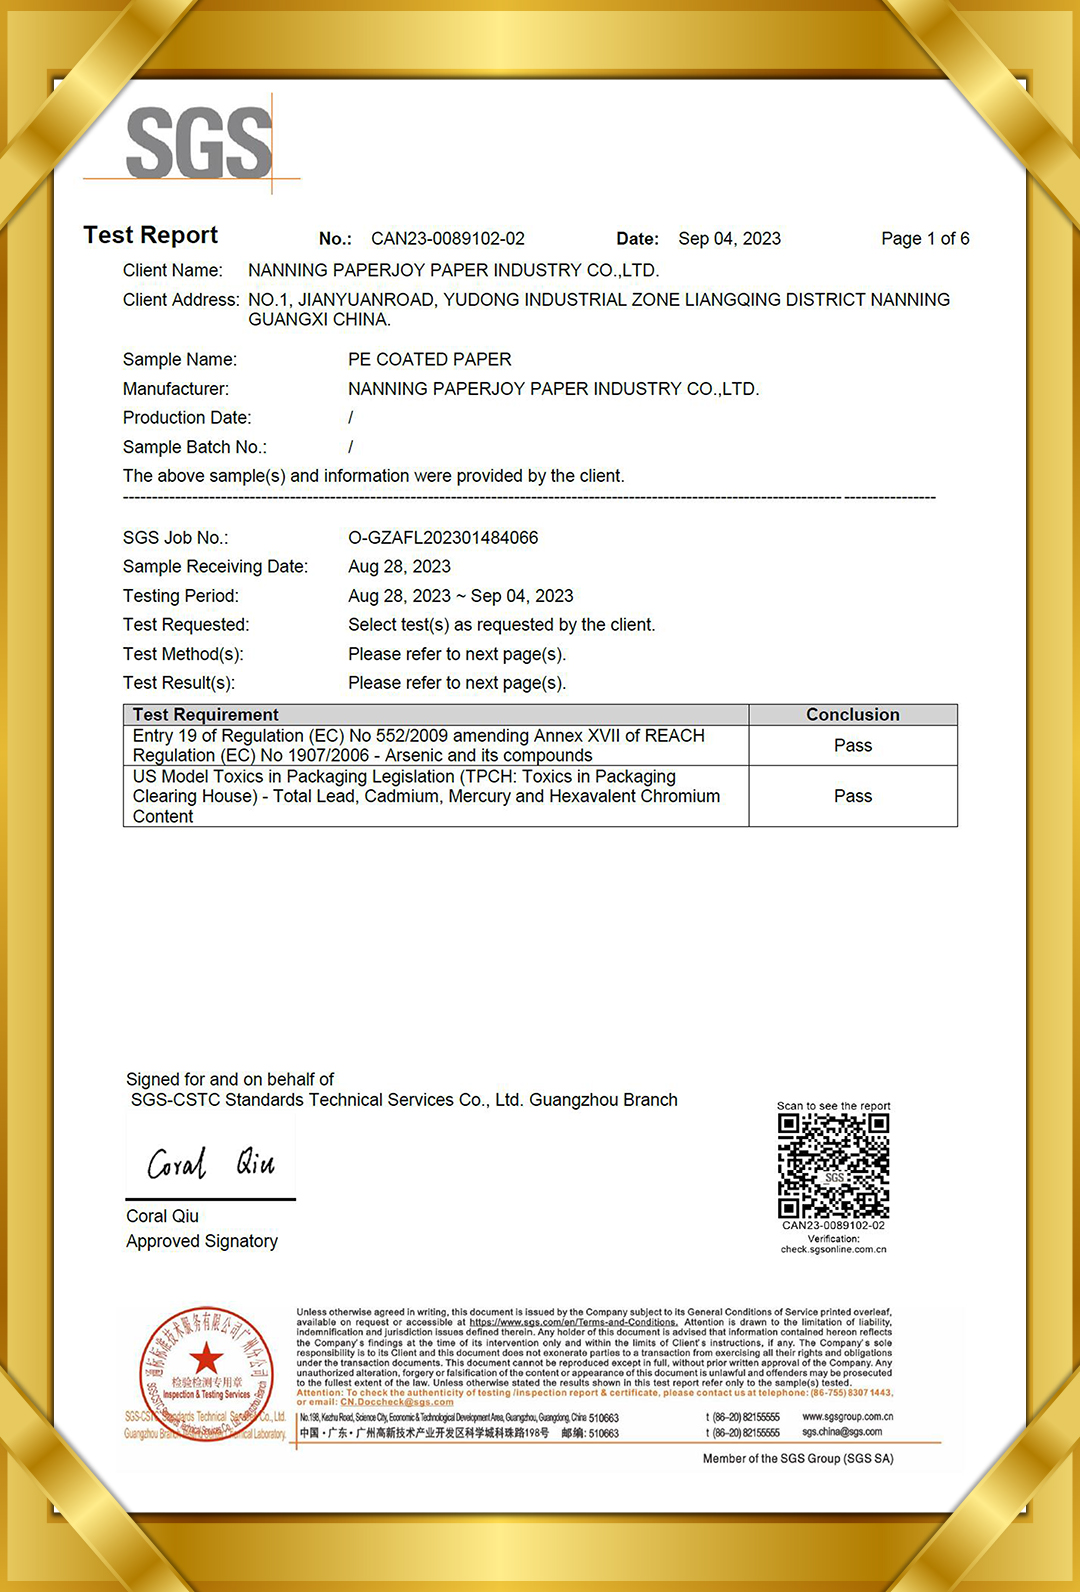
- Stringent Food Safety Standards: Heightened regulatory mandates enforcing zero-migration barriers, eliminating hazardous substances such as PFAS, phthalates, and bisphenol compounds.
- Recyclability & Circular Economy Mandates: Global EPR (Extended Producer Responsibility) schemes driving adoption of FSC-certified virgin wood pulp and repulpable barrier coatings.
Comprehensive Technical Specifications & Material Performance
Selecting the precise paper cup raw material specification ensures optimal conversion efficiency on high-speed cup-forming machinery running at speeds exceeding 180 to 280 units per minute. Below is an engineered breakdown of physical and chemical parameters for food packaging substrates:
| Parameter / Property | Standard Specification Range | Testing Standard | Functional Significance in Food Packaging |
|---|---|---|---|
| Base Paper Grammage (GSM) | 150 gsm – 400 gsm (±3%) | ISO 536 / TAPPI T410 | Determines cup wall rigidity, stackability, and crush resistance. |
| PE Coating Weight | 10 gsm – 25 gsm (Single / Double Side) | ISO 3801 | Provides liquid barrier, heat sealability, and grease resistance. |
| Cobb Value (Water Absorbency) | ≤ 15 g/m² (10 min test) | ISO 535 / TAPPI T441 | Prevents edge wicking and cup softening during liquid containment. |
| Tensile Strength (MD/CD) | ≥ 7.5 kN/m / ≥ 4.2 kN/m | ISO 1924-2 | Ensures smooth tension during web unwinding and high-speed die-cutting. |
| Bending Stiffness (Taber) | 1.8 – 14.5 mN·m (dependent on GSM) | ISO 2493 | Prevents cup collapse when gripped by consumers; ensures rigid rim curling. |
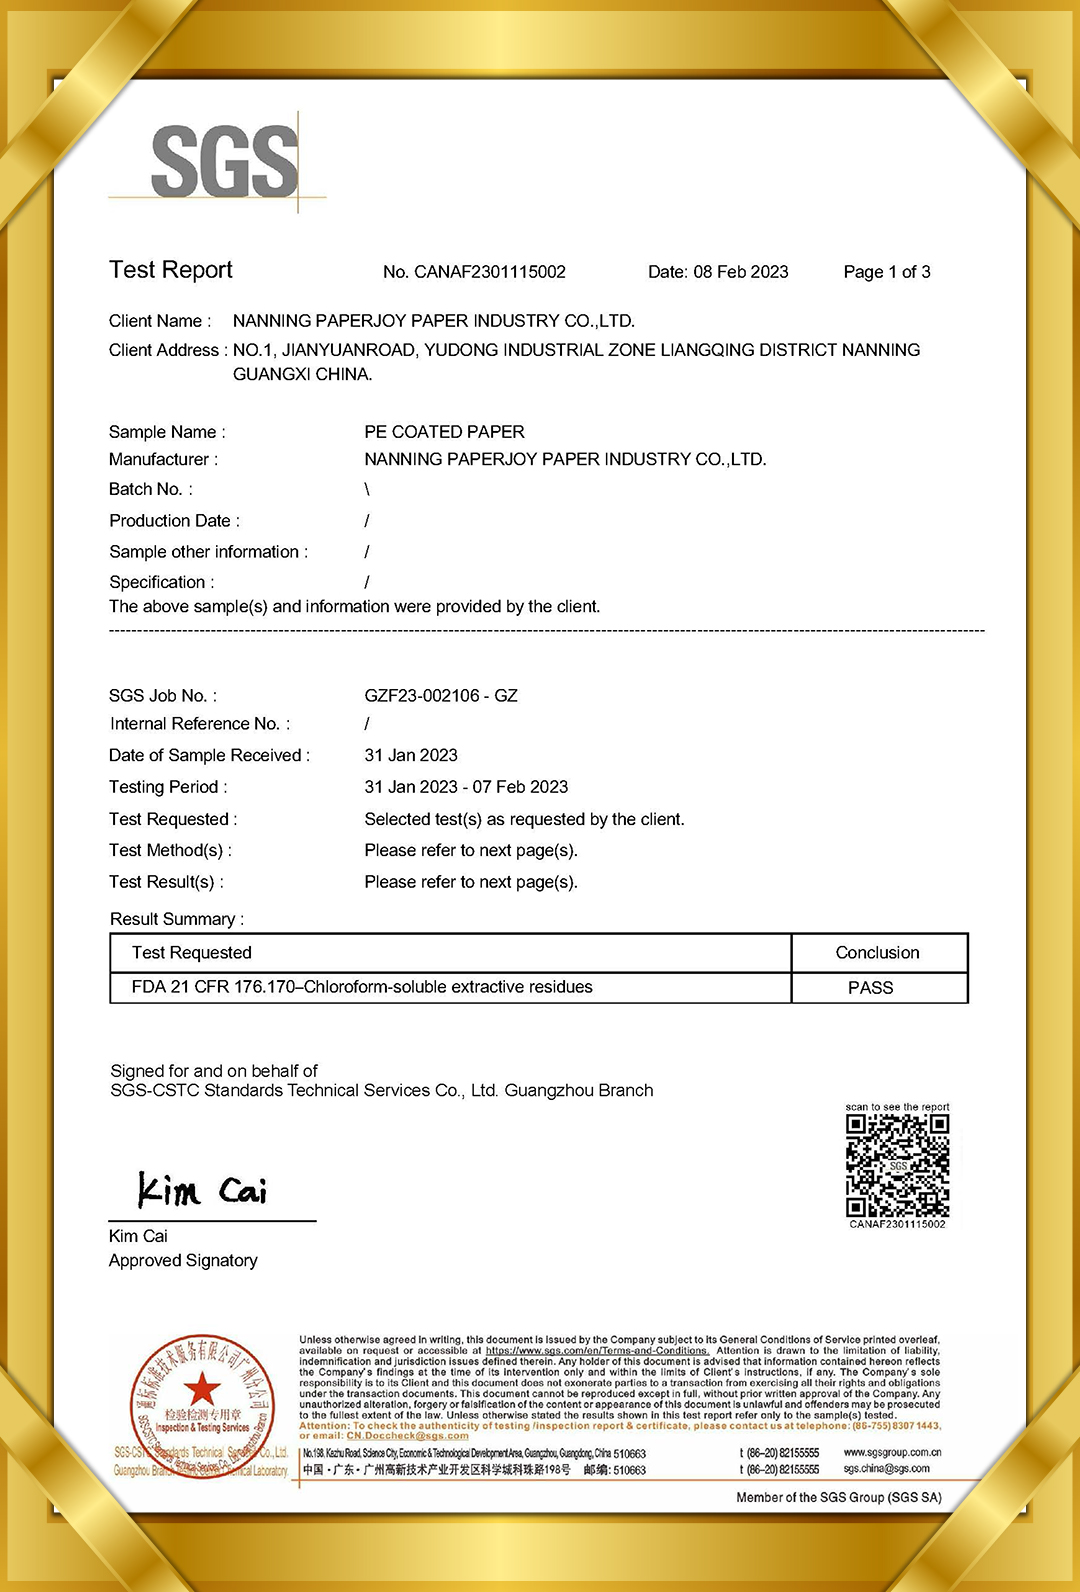
| Food Contact Safety | BPA Free, PFAS Free, Non-fluorescent | FDA 21 CFR 176.170 / REACH | Guarantees zero toxic chemical migration into hot or fatty food substances. |
Deep Analysis of Food Packaging Application Scenarios
From boiling espresso to deep-frozen ice cream, engineered paperboard raw materials meet distinct thermal, mechanical, and moisture barrier requirements.
Hot Beverage & Specialty Coffee
Utilizes single-side PE coated paper (1PE) from 190gsm to 320gsm. The inner PE layer provides liquid containment up to 100°C, while the smooth untreated outer surface ensures sharp flexographic branding. Paired with double-wall or ripple sleeve structures for exceptional thermal insulation without external cup sleeves.
Cold Drinks & Carbonated Sodas
Requires double-side PE coated paper (2PE). When cold liquids with ice cause ambient condensation on the cup exterior, the outer PE layer prevents the paper fibers from absorbing water droplets, eliminating soggy cup walls, rim deformation, and structural collapse during extended usage.
Ice Cream & Frozen Desserts
Engineered for sub-zero freezer environments (-20°C to -40°C). Double PE lamination prevents moisture frost embrittlement. Premium gloss or matte corona-treated surfaces allow vibrant multi-color graphics that retain adhesion in refrigerated display retail cabinets.
Instant Noodles & Hot Soups
High-grammage cupstock (280gsm – 380gsm) reinforced with heavy-gauge PE or PP coatings designed to withstand boiling broth, chili oils, and high acid content. The material exhibits ultra-low edge wicking and superior bottom-sealing integrity to prevent scalding leaks.
Fast Food Takeout & Buckets
Heavyweight virgin paperboard and C1S folding boxboards formulated for family-sized fried chicken buckets, popcorn tubs, and pastry trays. Provides high ring-crush resistance, grease repellency (Kit Level 9-12), and smooth automated lid snap-fitting.
Aviation & Institutional Catering
Specialized high-density, compact-nesting cup fans engineered for airline inflight services, healthcare dispensaries, and vending machines. Guarantees anti-static de-nesting performance and tight dimensional tolerances for smooth automated dispensing.
Company Profile & Manufacturing Power
Nanning Paperjoy Paper Industry Co., Ltd. – A dedicated leader in high-grade food packaging raw materials since 2006.
Nanning Paperjoy Paper Industry Co., Ltd. (“Paperjoy”) was established in 2006, with 200 employees and covers over 15,000㎡. Paperjoy is a professional manufacturer of raw materials for paper cup and packaging box, especially the PE coated paper roll, paper cup fan, cup bottom reel and C1S ivory board. We are specializing in producing different kinds of PE coated paper raw materials. The annual production capacity is 60,000 tons.
Our factory ideally located at the heart of Nanning city economic zone, which is very near to Qinzhou port, Beibu Gulf at the South of China. Our 200 well-trained and technically sound staff are motivated towards accomplish a common goal of customer satisfaction and devoted to achieve “Honesty, Mutual benefit, Win-Win cooperation” business philosophy.
Set up in 2006, engaged in paper cup paper PE coating industry. Paperjoy, means good luck and happiness.
Developing B2B overseas market. Expand the international market, target on Asia, Africa, Europe, North America, etc.
Brand-new production line installed; production capacity doubled to reach 60,000 tons/year.
2022-Our products have been used in more than 2,000 factories and exported to 60+ countries since 2006.
Supply Chain Advantages & Integrated Capabilities
Premium raw pulp procurement combined with turnkey conversion equipment for end-to-end quality assurance.
Paperjoy factory located very near to several famous paper mill brands. Stora Enso, Sunpaper, APP, Yibin paper, and FiveStar paper etc… are our regular base paper suppliers.
Besides, we have built a comprehensive strategic partnership with SunPaper Groups, reliable paper quality and steady delivery time are guaranteed.
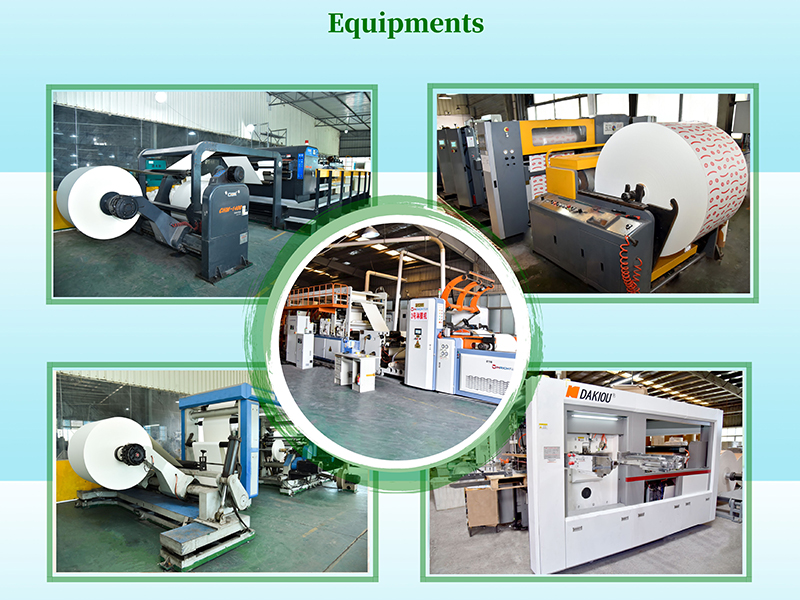
With complete devices and equipment, we are capable of providing one-stop service of PE coated, printing, die cutting, cleaning off and slitting.
Vision & Mission
Vision
Bring health and environmental protection to all over the world through sustainable cellulose food packaging solutions.
Mission 1
To be the best global supplier of paper cup raw material, offering world-class product quality and technical support.
Mission 2
To be the happy home for staffs, fostering talent growth, safety, and mutual prosperity.
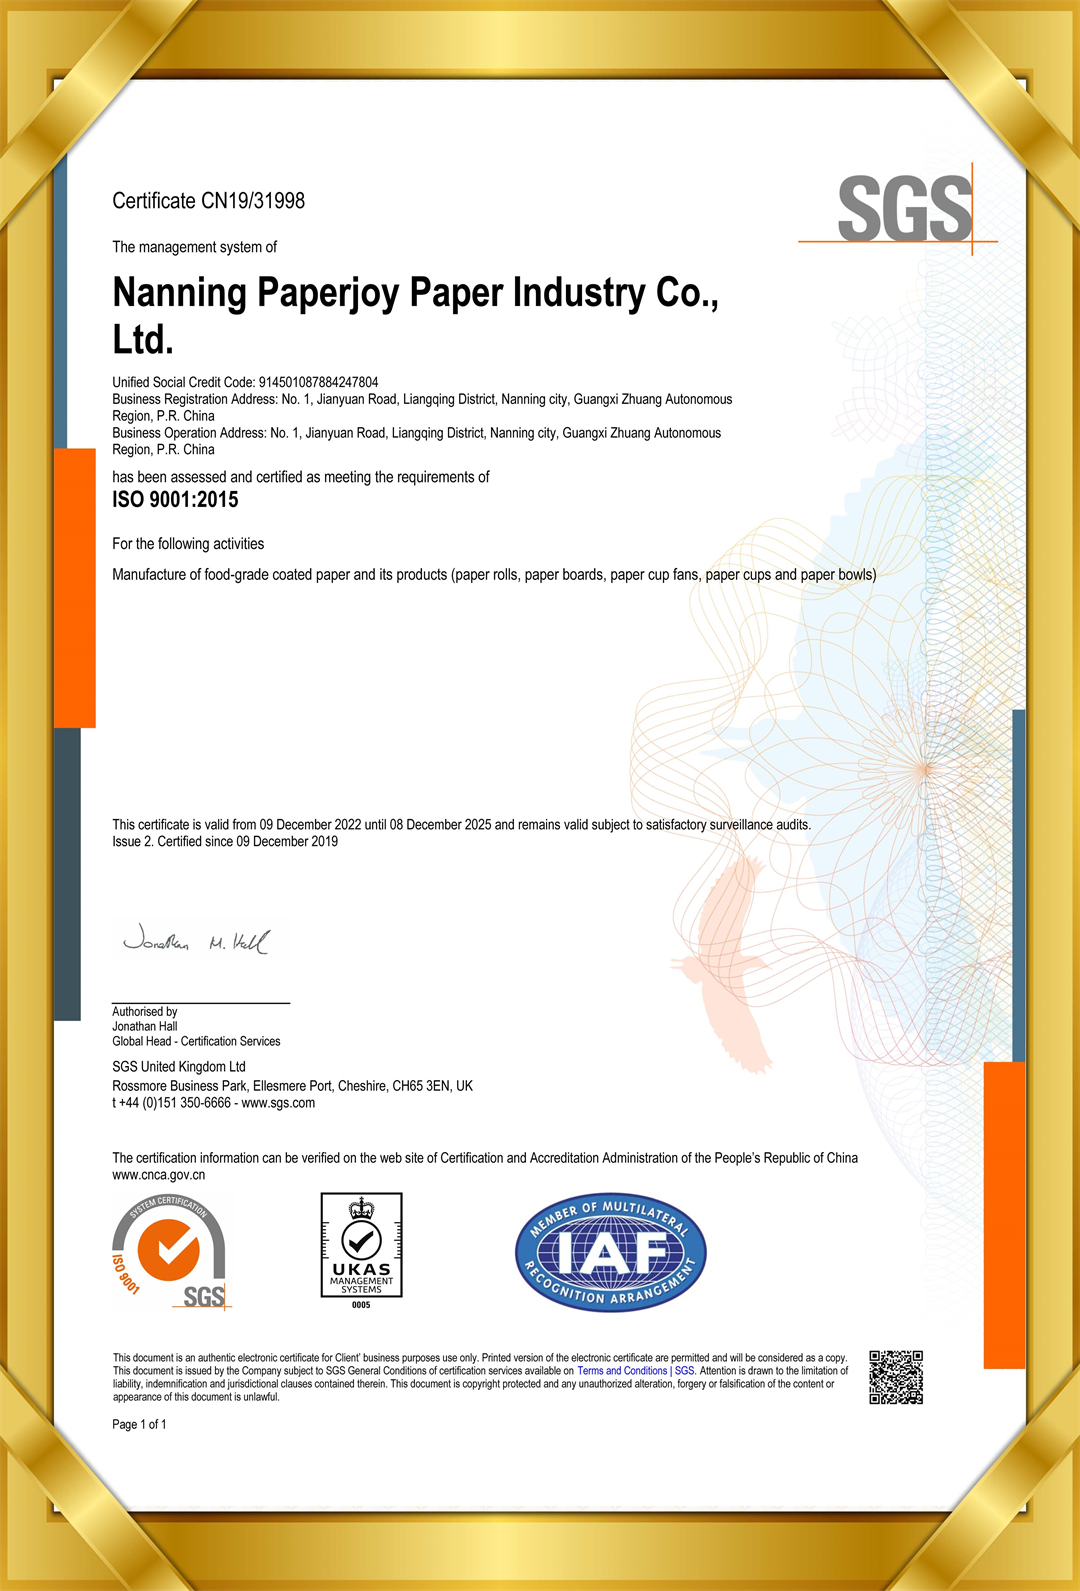
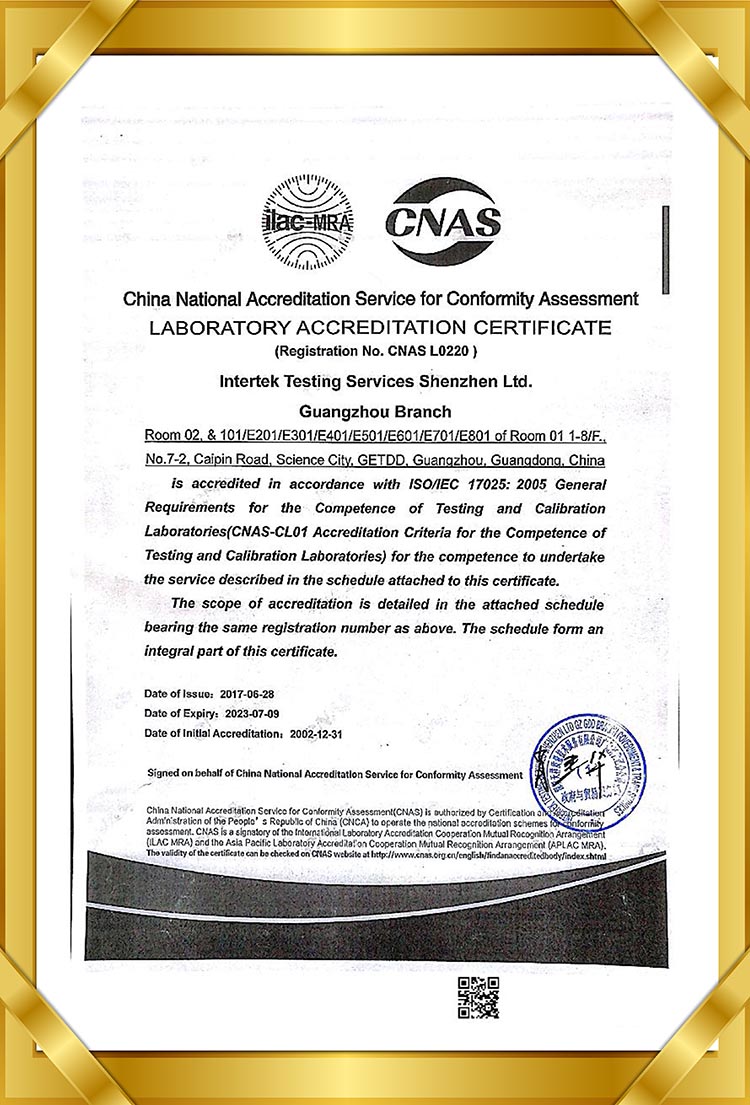
Certification System & Food Safety Standards
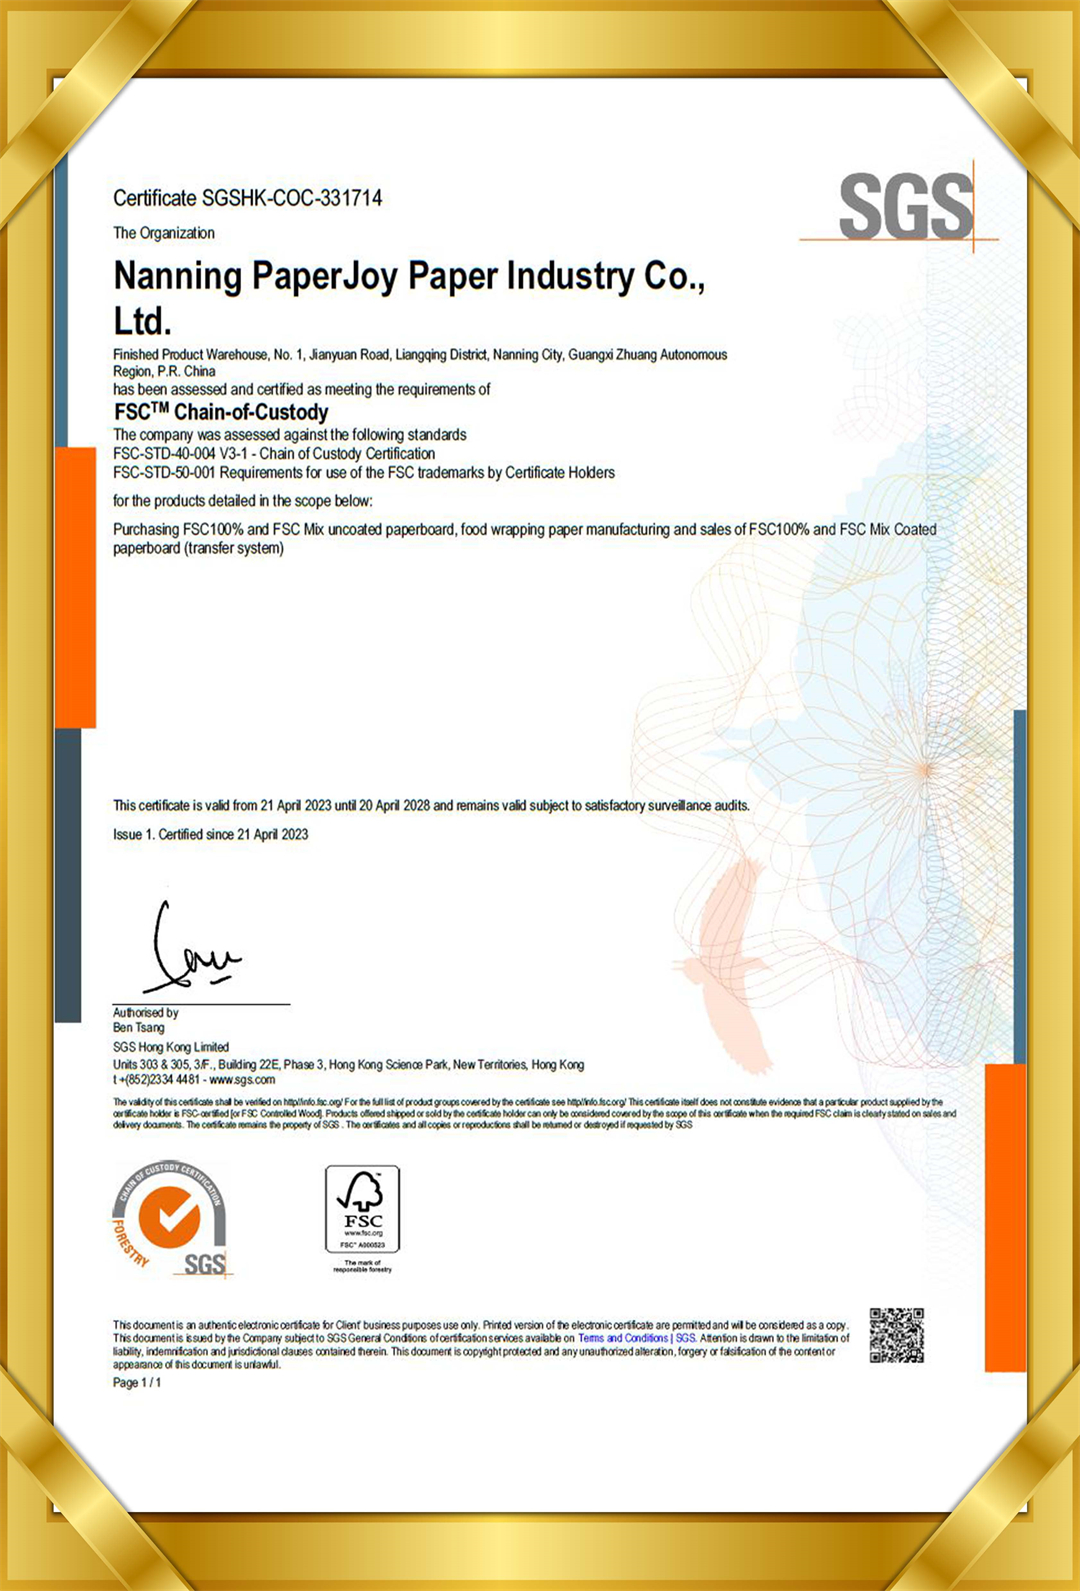
PaperJoy’s quality assurance system applies to all of our processes and products. Our quality management program ensures that every product delivered meets or exceeds the quality standards required by our customers.
Factory Tour, Processing & Equipment
High-speed extrusion laminators, multi-color flexographic printing presses, and automated die-cutters delivering consistent quality.
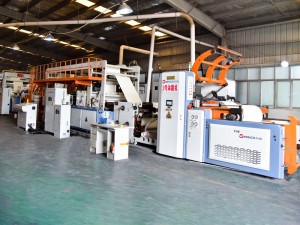
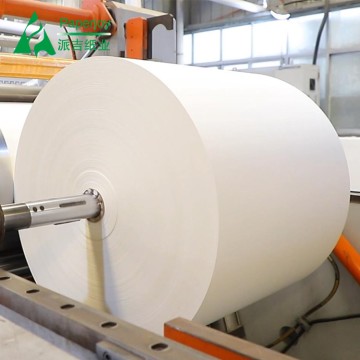
1. Three laminating machines are used to produce PE coated paper rolls. Auto high-speed production line, fit for fast delivery demand.
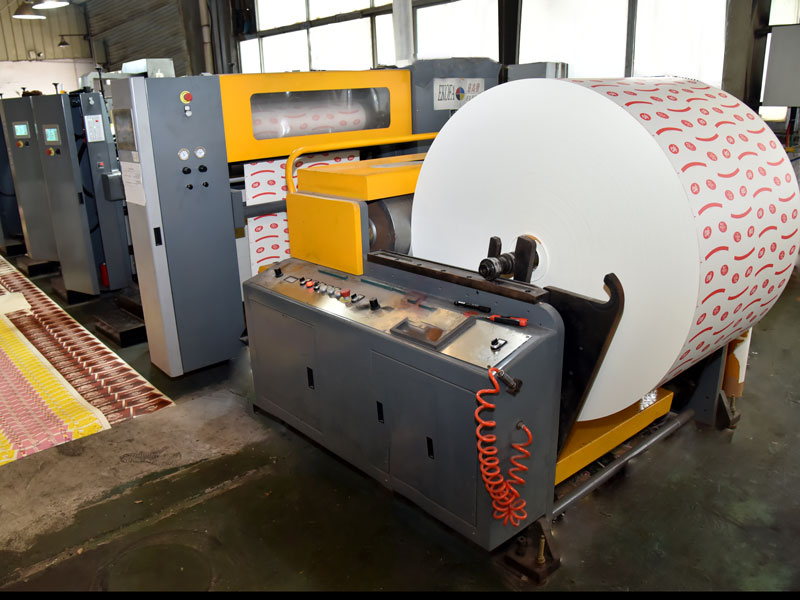
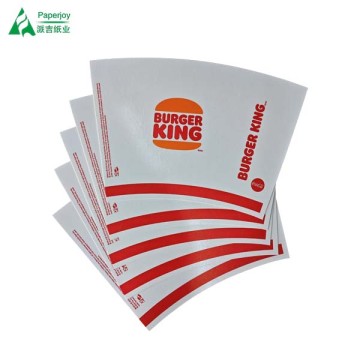
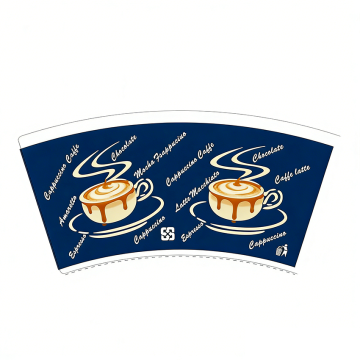
2. Three flexo-printing machines for printing paper cup fans in roll, six color high-speed flexo printing, running stable, printing clear.
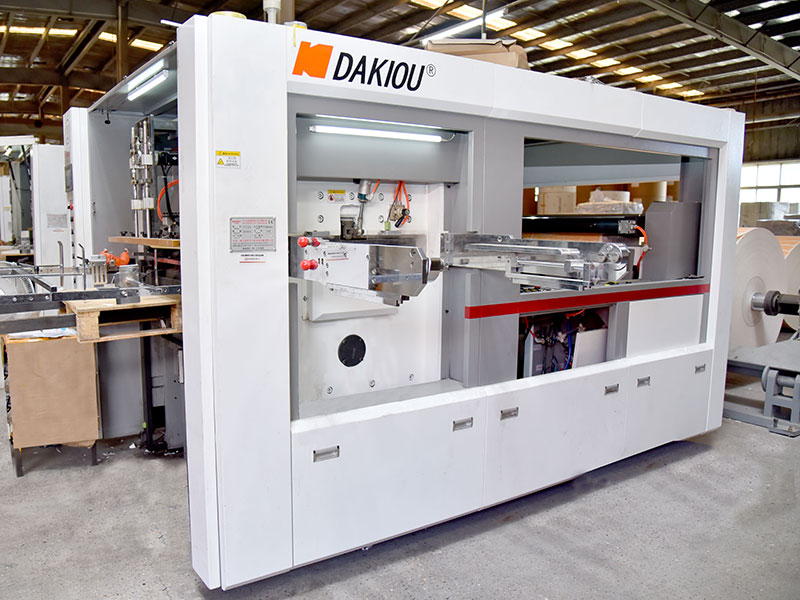
3. Eight die-cutting machines for die-cut paper cup fans. completely automatically, High speed, more than 280 sheets/min max.
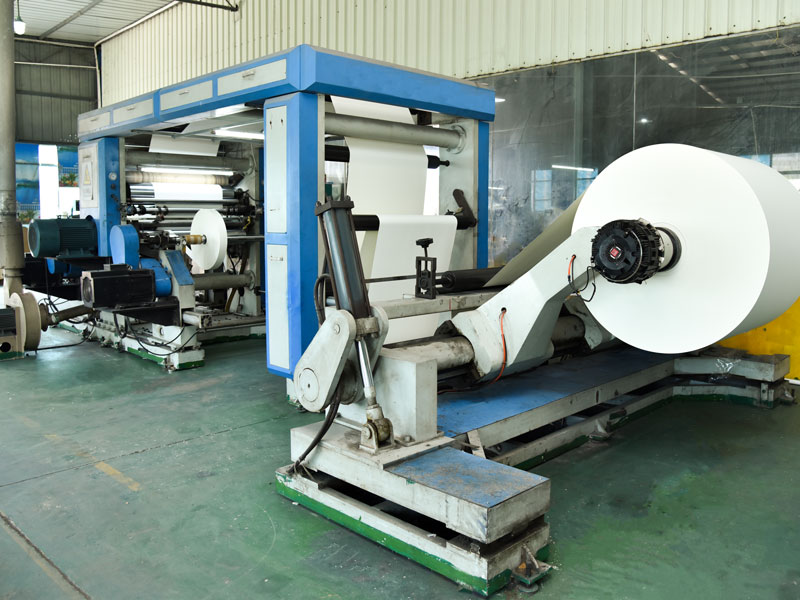
4. One high-speed slitting machine for produce paper cup bottom roll.
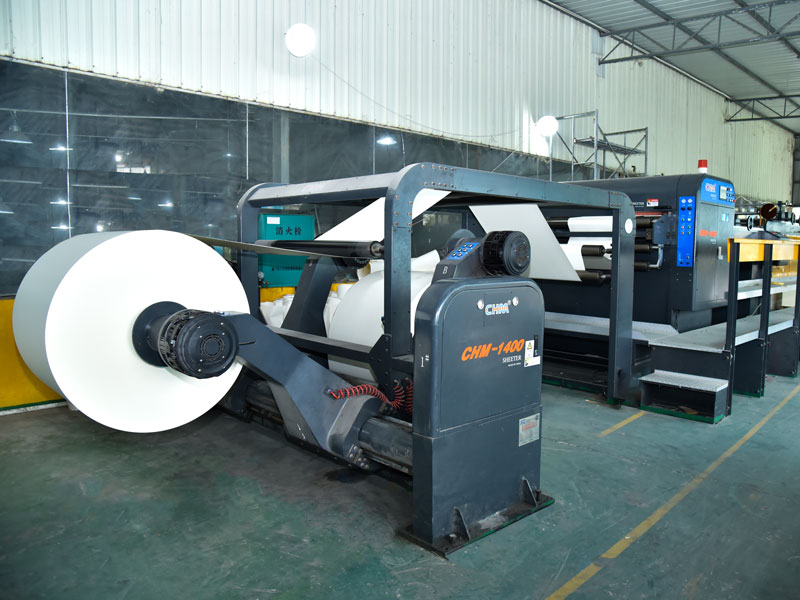
5. One high-speed cutting machine for the production of Pe coated paper sheets.
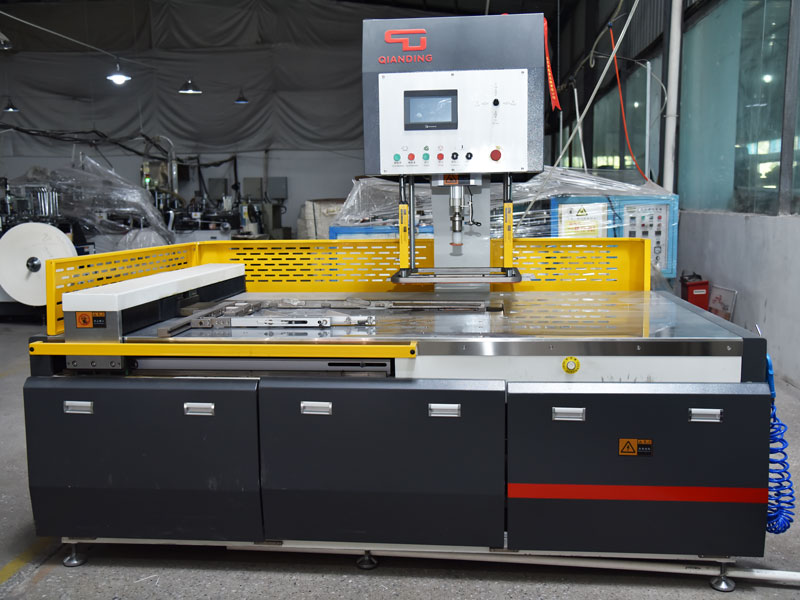
6. Eleven set of product standard machine. Cleaning the waste generated by various specifications of paper.
Personnel Operation Process & Facilities
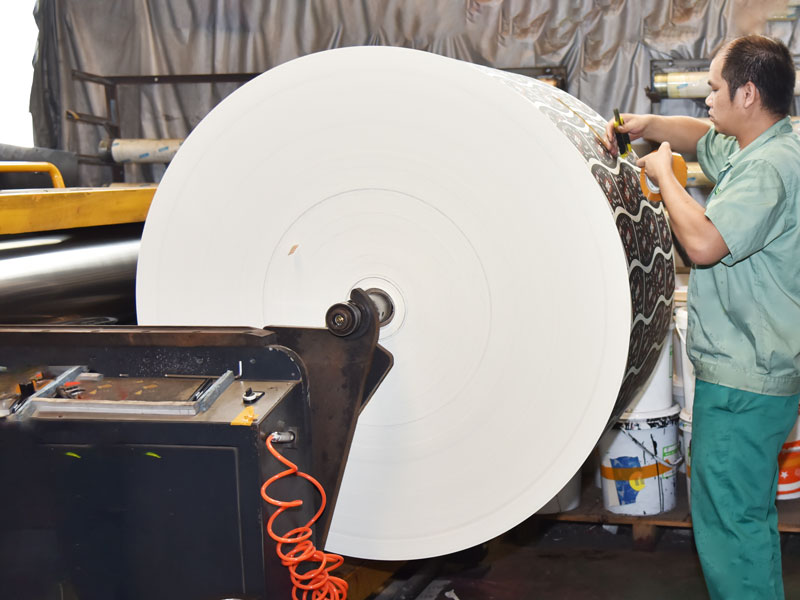
Paper Cup Fan Roll Preparation & Web Alignment
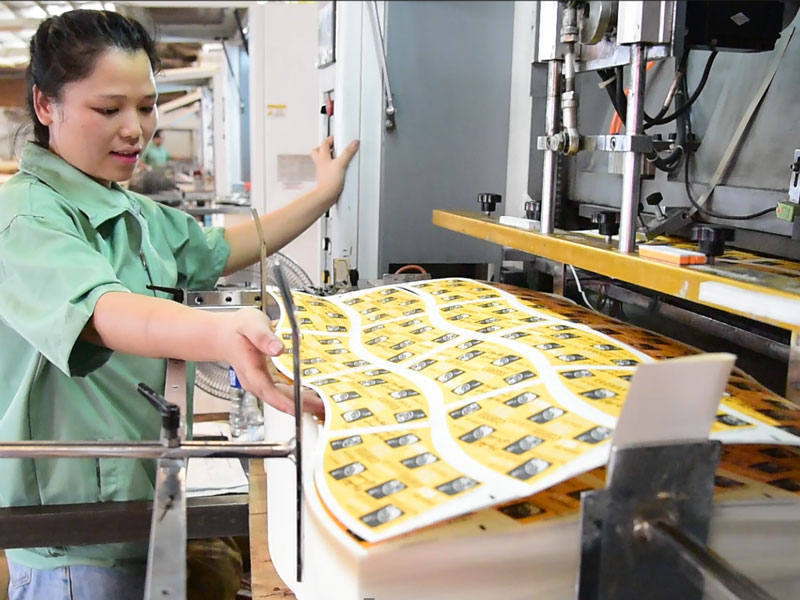
Die-cutting Paper Cup Fan High-Speed Processing
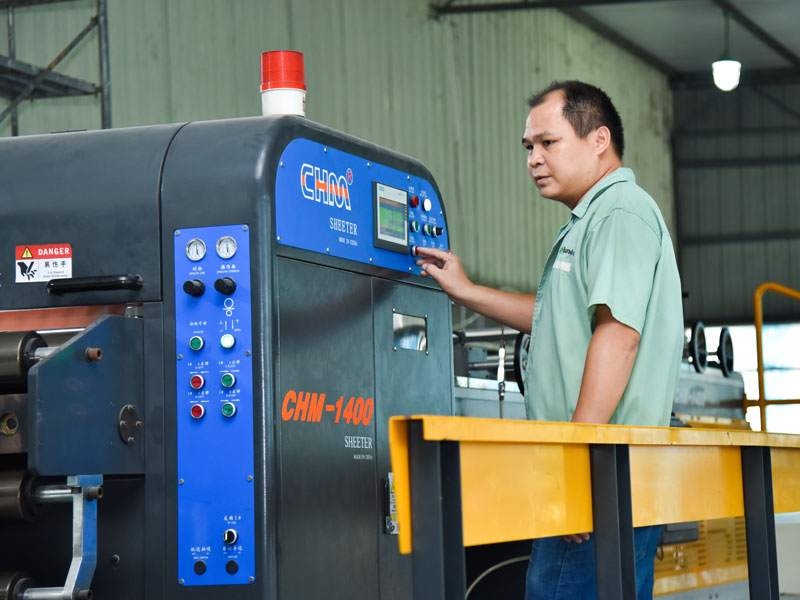
Waste Stripping & Packaging Automation
Strict Quality Inspection Protocol
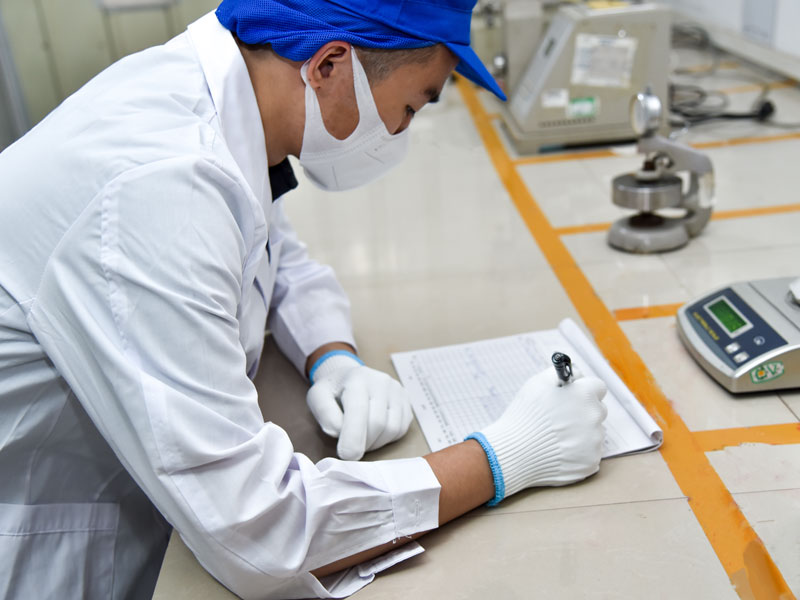
Rigorous multi-stage quality control from raw base paper batch inspection to finished product cup-forming simulation.
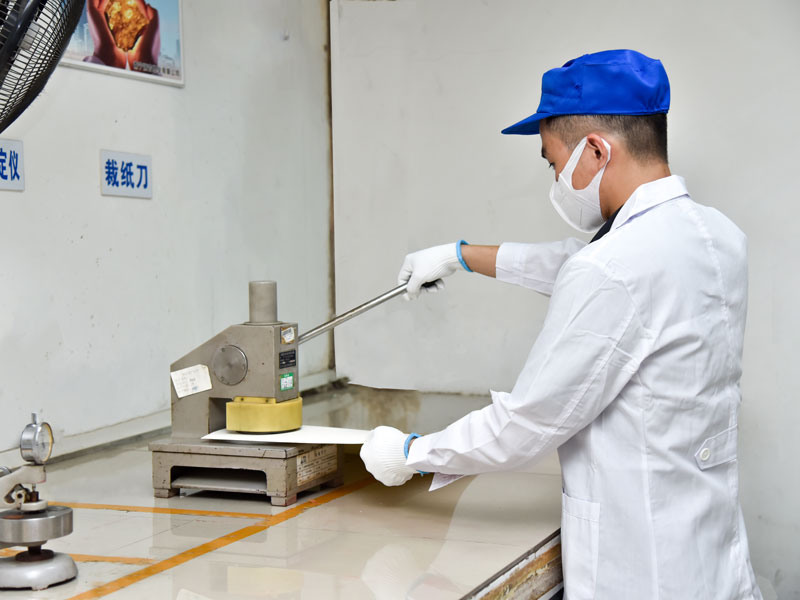
Basis Weight & Thickness Gauge
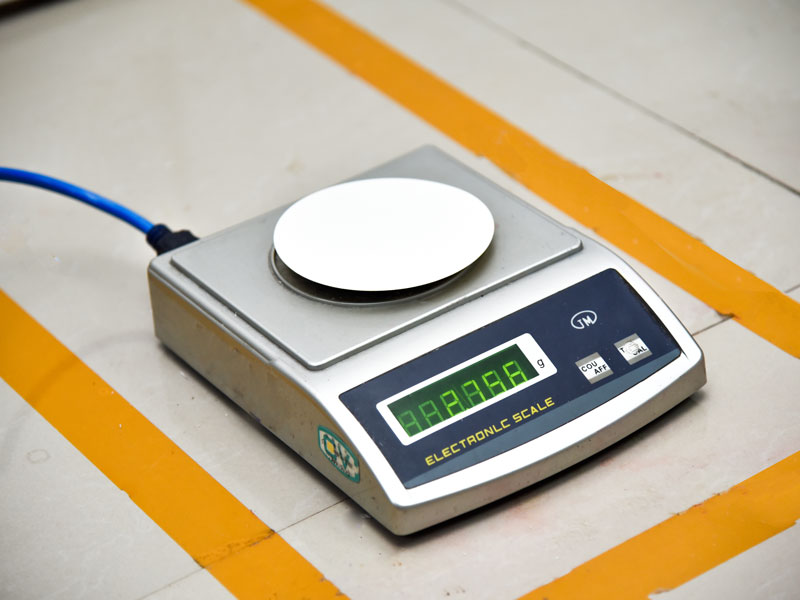
Moisture & Cobb Absorbency Testing
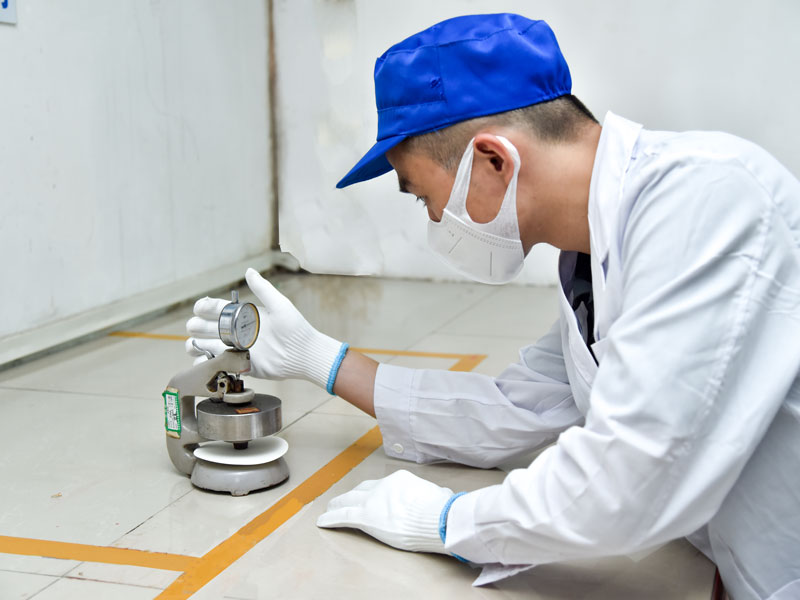
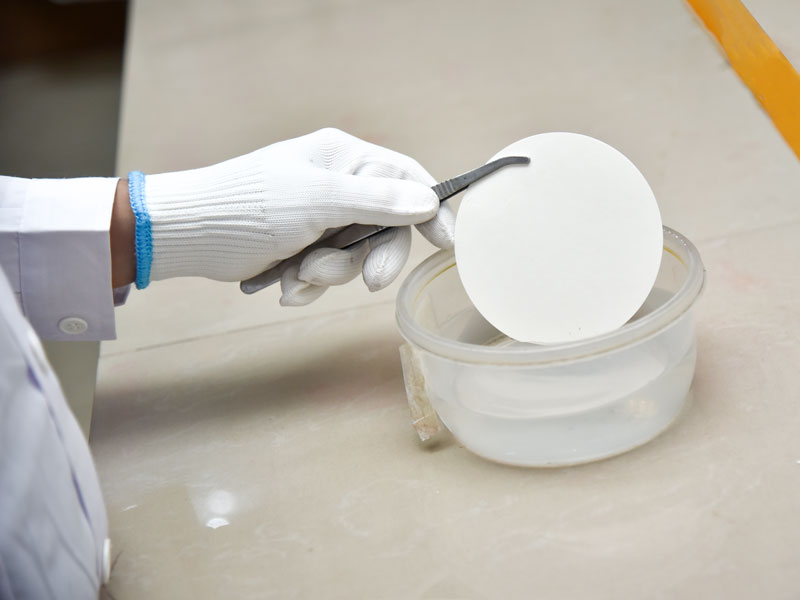
PE Film Adhesion & Corona Check
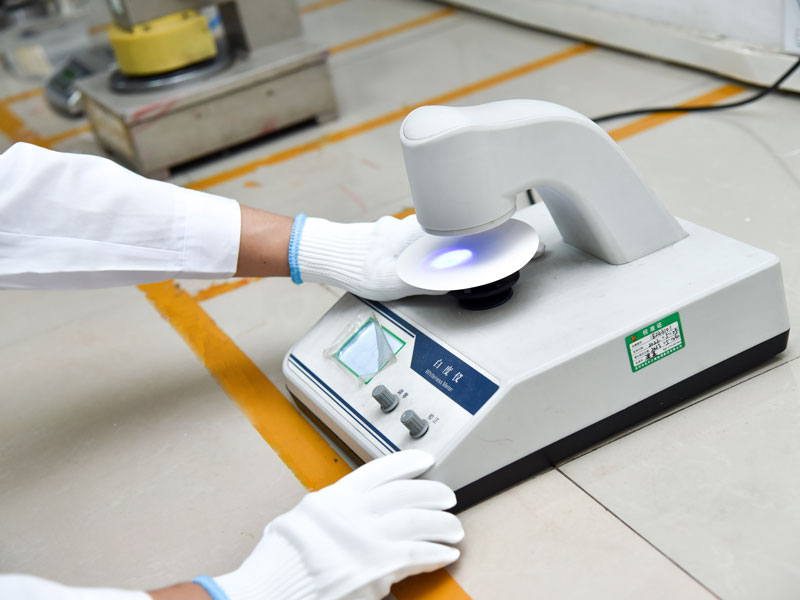
Tensile & Bursting Strength Test
Flexo Printing Spectrophotometry
Cup Forming Trial & Leakage Check
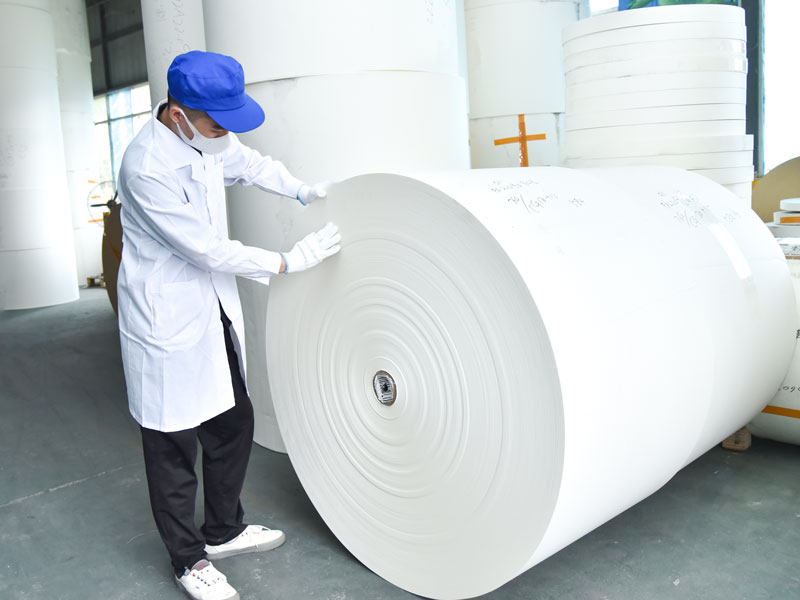
PE Coated Paper Roll Winding Density
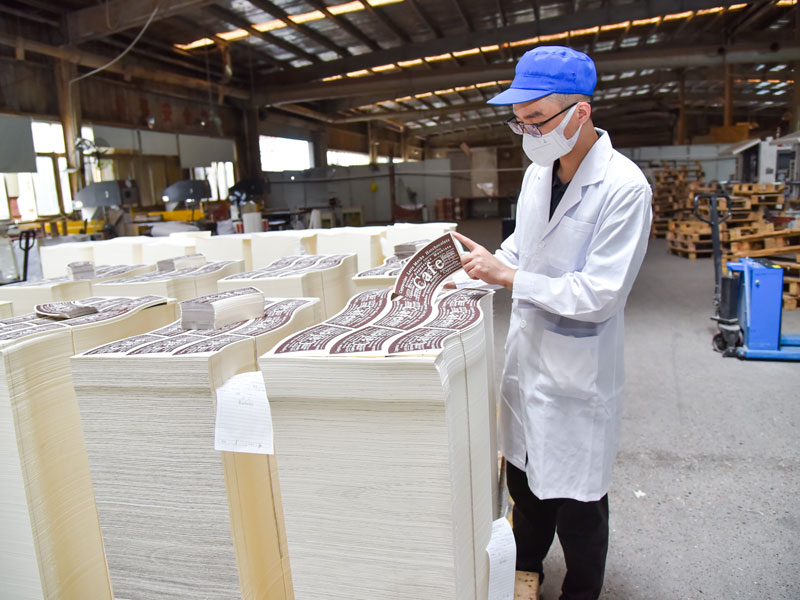
Paper Cup Fan Die-cut Precision Check
PaperJoy Global Service & Core Strengths
Your Reliable Global Partner for High-Quality Professional Paper Cup Raw Materials Supplier and Manufacturer & Professional Solutions.
Customized Products
We can provide customers with customized paperboard raw material products according to their needs and requirements to meet their different needs and application scenarios.
Diverse Products
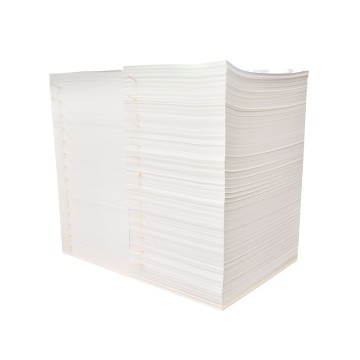
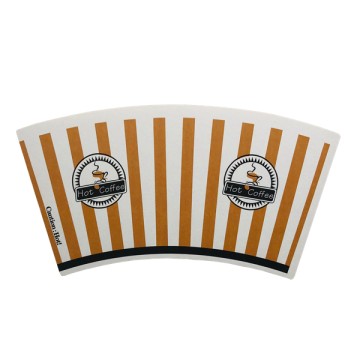
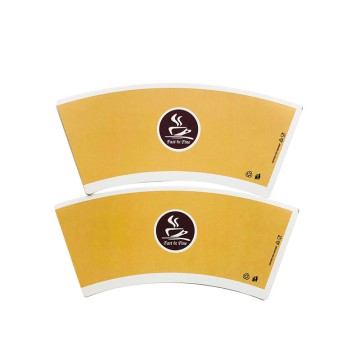
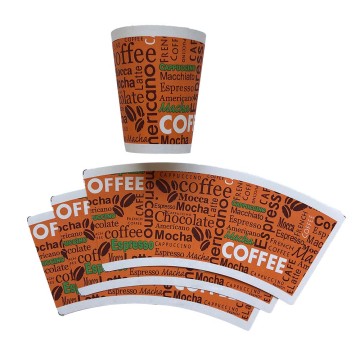
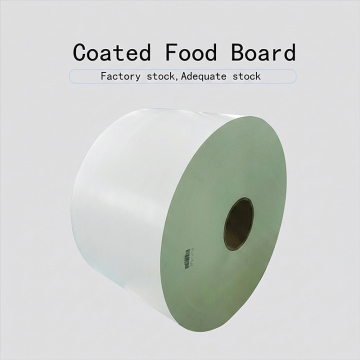
We offer a variety of paperboard raw material products, including PE coated Paper Roll, PE Coated Paper Sheet, Paper Cup Fan, C1S Ivory Board, Kraft Paper Roll, and more.
Free Quotations & Samples
We provide free samples and quotes to ensure that our customers can experience our high-quality paperboard raw materials firsthand and make informed purchasing decisions.
Fast Delivery
With an efficient production and supply chain management system, we can ensure that customers get the required paperboard raw materials in the shortest possible time and meet urgent market demands.
Technical Consulting
Our professional technical team provides consulting services on product specifications, technical parameters, and production machine tuning to ensure trouble-free cup conversion.
24H/7D Professional Support
We have a professional technical team and after-sales service team providing 24/7 one-to-one assistance, ensuring comprehensive support throughout the purchasing lifecycle.
Factory Overview & Key Metrics
Packaging, Export Delivery & Enterprise Honors
Moisture-proof wrapping, palletized protection, and international sea-freight logistics excellence.
PE Coated Paper Roll Multi-layer Waterproof Kraft Wrapping
Die-cut Paper Cup Fans Bundled & Carton Pallet Packaging
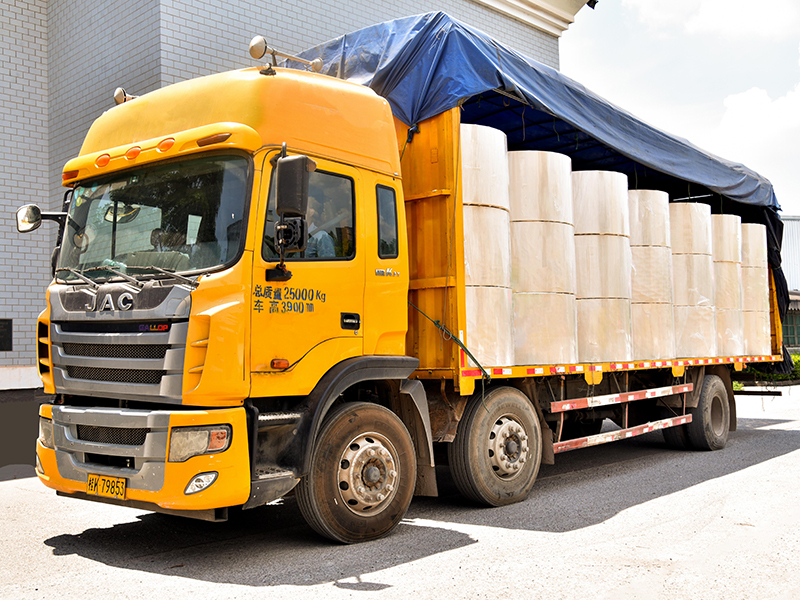
Strict Container Stuffing & Port Logistics Near Beibu Gulf
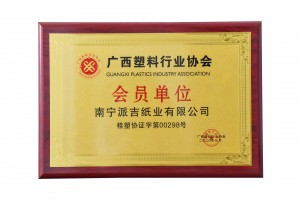
Plastics Association member unit
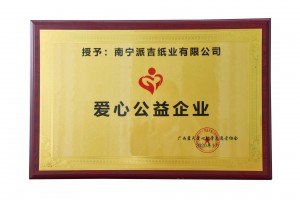
Charitable enterprise
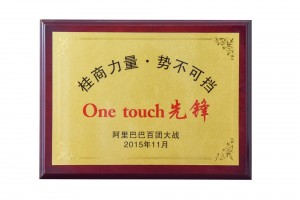
Alibaba Verified Supplier
Complete Paper Cup Raw Material Product Catalog
Explore our full line of food packaging paper raw materials, cupstock paper rolls, printed fans, and food-grade barrier boards.