


The Versatility of PE Coated Paper in Packaging
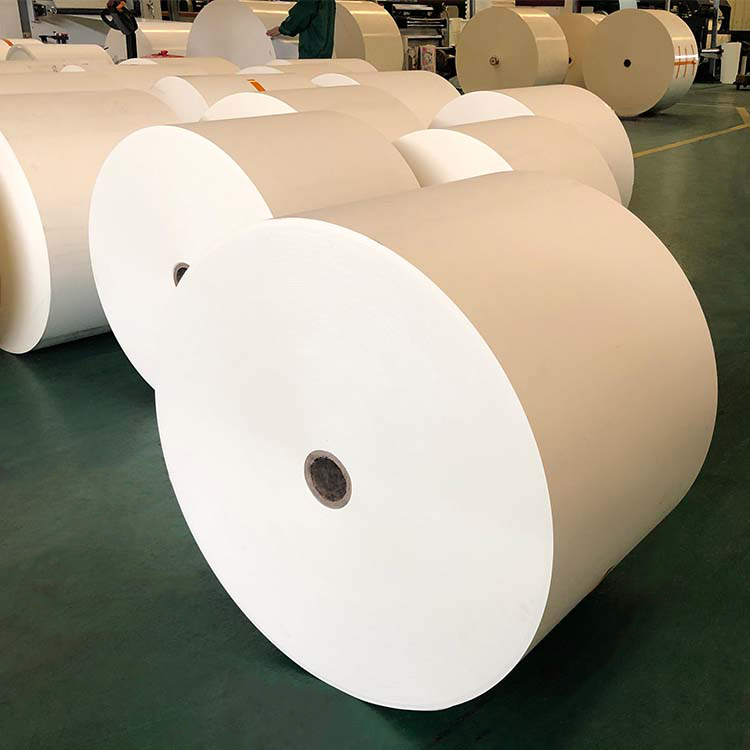
In today’s world, packaging plays a crucial role in preserving the quality of products and ensuring their safe transportation. One such packaging material that has gained significant popularity is PE Coated Paper. But what exactly is PE coated paper, and why is it so commonly used in various industries?
What is PE Coated Paper?
PE coated paper is simply paper that has been coated with a layer of polyethylene (PE), a type of plastic. Polyethylene is widely used for its waterproof and durable properties, and when applied to paper, it enhances the paper’s ability to resist moisture, grease, and other environmental factors. The process involves applying a thin layer of PE to one or both sides of the paper, creating a smooth, water-resistant surface. This makes it an excellent material for packaging, especially for products that need protection from liquid or oil.
Properties of PE Coated Paper
The main advantages of PE coated paper include:
Water Resistance: The polyethylene coating makes the paper resistant to water and liquids, which helps prevent it from getting soggy or damaged. This is particularly useful in applications like food packaging, where the paper needs to stay intact even when in contact with moisture.
Grease Resistance: The PE coating also acts as a barrier against oils and grease. This is especially beneficial for food packaging items such as pizza boxes, sandwich wrappers, or snack bags, which often come into contact with oily or greasy substances.
Durability: The layer of polyethylene adds to the strength of the paper, making it more durable and resistant to tearing or breaking. This makes PE coated paper suitable for heavier-duty packaging needs.
Printable Surface: Despite the coating, PE coated paper retains a printable surface, making it ideal for custom branding and labeling. Whether for logos, product information, or other designs, the paper can be printed on with high-quality inks.
Common Uses of PE Coated Paper
PE coated paper is commonly used in a variety of industries, particularly in packaging. Some of the most common applications include:
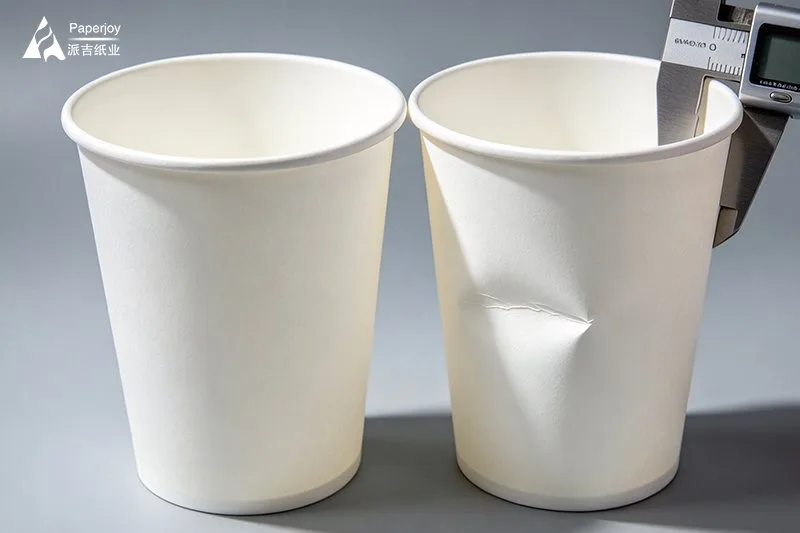
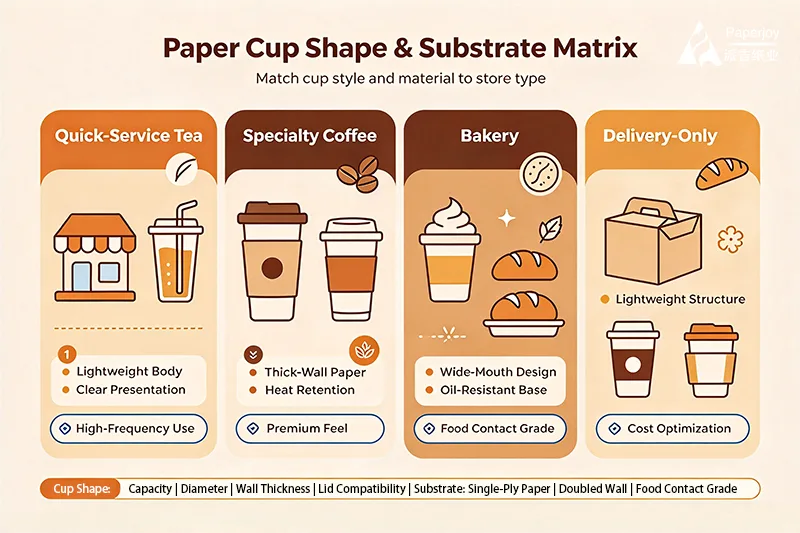
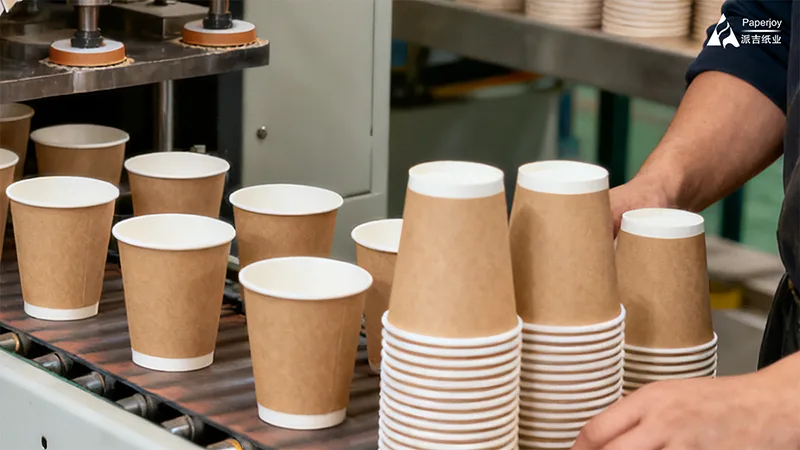
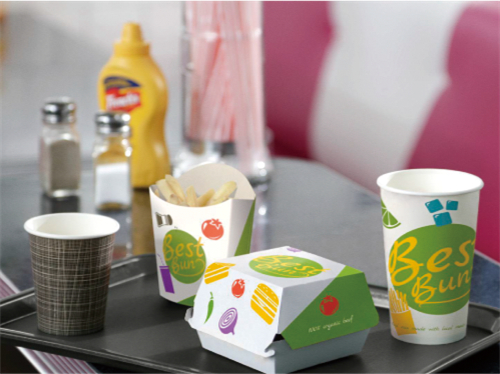
Take-out containers, food wraps, sandwich sleeves, and drink cups often use PE coated paper to protect the food from moisture, grease, and contamination. It ensures the food stays fresh and the packaging remains intact.
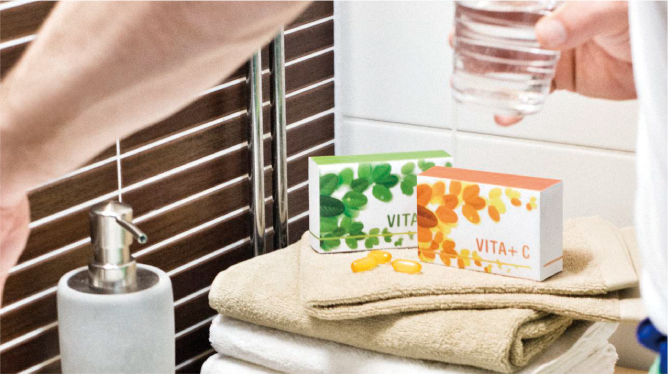
Due to its protective properties, PE coated paper is also used in some medical packaging applications to safeguard products from contamination or damage.
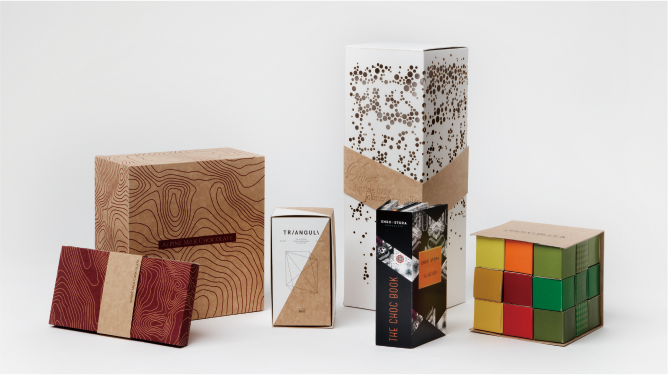
The smooth, glossy finish of PE coated paper makes it ideal for high-quality gift wrap that resists tears and wrinkles while offering an attractive sheen.
Environmental Considerations
While PE coated paper offers many practical benefits, one of the challenges is its environmental impact. The polyethylene coating makes the paper more difficult to recycle than regular paper. However, there are ongoing efforts to develop more sustainable coatings or to recycle PE coated paper through specialized processes.
Some manufacturers are turning to bio-based polyethylene as a more environmentally friendly alternative. Additionally, many businesses are focusing on reducing waste and increasing the recyclability of their packaging materials, including PE coated paper.
PE coated paper is a versatile material that has become indispensable in the packaging industry due to its moisture and grease resistance, durability, and printable surface. Whether for food packaging, medical supplies, or even gift wraps, its unique properties make it a popular choice for a wide range of applications. As environmental awareness grows, innovations in sustainable PE coatings may further enhance the material’s role in eco-friendly packaging solutions.